
Client satisfaction in mass timber projects often comes down to what you don’t hear.
Acoustics are one of the top post-occupancy complaints in buildings, especially when exposed systems amplify the problem. And with mass timber - this can’t be ignored.
In mass timber buildings, acoustics are often overlooked until it’s too late - when the client is frustrated, complaints start piling up, and your team is asked to explain why a premium building sounds like a budget one.
The irony? The very things that make mass timber so desirable, its sustainability, openness, and exposed finishes, also make it harder to control noise.
This isn’t just a minor inconvenience, it’s a design liability.
“What you don’t want is to be hearing everything going on outside your walls,” says Aedan Callaghan with Pliteq.
And neither do your clients. Solving for sound requires remembering, and maybe a bit of rethinking, of the fundamentals - all without compromising the architectural or environmental intent that brought you to mass timber in the first place.
Breaking Down the Basics: Airborne vs. Structure-Borne Sound
Not all noise is created equal - distinguishing between its sources is fundamental to effective acoustic design. Callaghan clarifies the two principal categories: airborne sound, such as voices or music, and structure-borne sound, like footsteps or mechanical vibrations.
Airborne sound is quantified by the Sound Transmission Class (STC), a number rating that reflects a wall assembly’s ability to block noise passing through the air. Structure-borne sound is measured by the Impact Insulation Class (IIC), which gauges how well a floor or ceiling assembly dampens impact-generated vibrations.
“The higher the [STC or IIC] rating, the better job it does at preventing you from hearing that type of noise,” Callaghan explains.
Recognizing these distinctions is the first step toward specifying assemblies that genuinely improve acoustic comfort.
The Unique Acoustic Behavior of Mass Timber
The drive for exposed timber aesthetics introduces a paradox: the very qualities that make mass timber appealing can compromise its acoustic performance. Unlike concrete, mass timber’s lower density and the frequent omission of suspended ceilings create new transmission paths for sound.
“Ironically in mass timber, the mass isn't actually all that high… about one-fifth the weight of the same thickness concrete,” says Callaghan.
Traditional assemblies rely on suspended ceilings as acoustic buffers. In mass timber, with its exposed CLT ceilings, designers must rethink their approach—and build quiet from the top down.
Practical Acoustic Solutions for Mass Timber Projects
Solving for Sound, Layer by Layer
To deliver acoustic performance that lives up to design expectations, project teams must approach mass timber differently.
Here are four key areas of focus:
1. Floor Systems: Building Quiet from the Top Down In mass timber construction, exposed CLT ceilings are part of the appeal—but they come at an acoustic cost. Unlike traditional wood or steel systems, which often include a suspended ceiling cavity to house resilient channels or insulation, exposed timber ceilings eliminate that layer entirely. That means the burden of acoustic performance shifts upward—to the floor assembly above.
This challenge is compounded by mass timber’s relatively low density compared to concrete. Without the mass or the decoupling benefits of a dropped ceiling, structure-borne impact sounds (like footsteps, dropped items, or appliance vibrations) can easily travel from floor to floor unless the system above is properly engineered.
The fix? You need to introduce mass and isolation above the CLT, and do it in a way that doesn’t undermine the benefits of timber construction—namely speed, sustainability, and moisture sensitivity. A few widely used strategies include:
- Acoustic mats that isolate the finish floor or topping layer from the CLT substrate.
- Topping layers that add mass, like traditional concrete, lightweight Gypcrete, or newer dry solutions like compressed gypsum fiber board.
- Floating floors or decoupled subfloor assemblies that minimize direct mechanical connection to the CLT.
Aidan Callaghan recommends a composite dry system, combining isolation and mass without the downsides of wet trades:
- GenieMat FF – a post-consumer recycled rubber isolation underlayment laid directly over CLT to absorb vibration and prevent transmission.
- GenieBoard – a dry, high-density recycled gypsum fiber board that adds acoustic mass without introducing water into the building envelope.
“You’re trying to keep the timber as dry as possible. GenieBoard gets rid of the cure time and moisture challenges—and still meets code,” Callaghan says.
In side-by-side performance testing, this dry system matched traditional 2" concrete topping assemblies in acoustic performance while offering major construction benefits:
- Eliminated wet trades and cure time
- Reduced floor weight by 10 psf
- Enabled thinner foundations and CFS wall framing
- Shortened schedules by 7–10 days
2. Wall Assemblies: Separate to Isolate
When it comes to blocking airborne noise—voices, music, or television—wall assemblies are your primary line of defense. But not all walls are created equal. Standard single-stud assemblies with drywall on both sides typically fall short, allowing sound vibrations to travel through the rigid connections between materials.
The result? Code minimum STC ratings—and clients who hear far more than they should.
To improve isolation, the key is to introduce separation within the wall structure, either by decoupling layers or adding mass and damping between them. The most effective solution in high-performance multifamily and commercial projects is the double stud wall: two parallel stud walls with a 1" air gap between them and drywall applied to each outer face.
“When the sound gets into that first wall, there's an air gap preventing it from getting into that second wall,” explains Callahan.
This configuration minimizes rigid connections across the wall, allowing it to achieve STC ratings of 60–63—often enough to meet or exceed expectations for luxury residential, hospitality, and institutional settings.
For projects where space is at a premium and thicker wall assemblies aren’t viable, alternatives like resilient isolation clips (e.g., GenieClips) can decouple one side of the drywall from the framing without sacrificing square footage. These clips absorb and damp vibration, reducing the transfer of airborne sound while preserving the wall’s footprint.
No matter which path you choose—wider assemblies or resilient mounting hardware—the principle remains the same: disconnect the structure to block the sound.
3. Flanking: The Silent Saboteur
You can specify the highest-performing wall and floor assemblies on paper—but if flanking isn’t addressed, the sound will find another way in.
Flanking paths are indirect routes that sound takes around acoustic separations. In mass timber buildings, the most common culprit is the continuous CLT structure—a beautiful, solid surface that also acts as a bridge for vibration. Sound can travel over, under, or around rated walls via uninterrupted timber panels, undermining even the best acoustic assemblies.
Think of it like water slipping through the cracks—except in this case, the cracks are the architectural connections between timber elements.
Callahan emphasizes that flanking can completely undermine the performance of even top-tier assemblies, making them ineffective in real-world conditions if not addressed holistically. That’s why it’s critical to design with flanking in mind -not after the fact, but as part of the core acoustic strategy.
Several best-practice approaches include:
- Interrupting CLT panels at unit boundaries, where possible
- Using spline joints or acoustic gaskets to reduce sound transfer
- Designing bulkheads or dropped soffits at transition zones
- Alternating ceiling treatments (e.g., exposed vs. acoustic finishes) between adjoining spaces
- Performing detailed junction reviews with your acoustic consultant and timber fabricator
“If you've ignored flanking, you're not actually getting what you paid for with that upgraded assembly,” warns Callahan.
The fix isn't always complicated but it must be deliberate. Addressing flanking is about ensuring the building performs as designed, especially in exposed systems where structural continuity is visually celebrated but acoustically risky.
4. When to Act: Earlier Is Quieter Timing matters. Callahan recommends engaging acoustic teams no later than early design development (DD) to ensure integration of acoustic strategy into structural and architectural design. Late-stage fixes are costlier and often less effective.
The Importance of Considering Acoustics Early
Acoustics can't be value-engineered in after the fact. Callahan emphasizes the importance of bringing on acoustic consultants during design development (DD):
“The earlier that you can bring all these decisions forward, the better it is for the project as a whole.”
Early coordination allows for optimized junction details, accurate acoustic targets, and the ability to realize whole-building efficiencies like lighter foundations and thinner floor plates.
Case in Point: Multi-Family Building in New York
In a recent mass timber project in New York, Pliteq’s dry system replaced a conventional concrete topping with:
- 10 psf weight savings
- 2" less rebar and slab thickness
- 16% less cold-formed steel (CFS) wall material
- Acoustic performance equal to traditional assemblies
- Construction schedule shortened by 7–10 days
Despite a slightly higher installed cost for the GenieBoard system (~$1–2/sf), the overall project cost came out lower—thanks to structural and scheduling efficiencies unlocked by the lighter, dry floor assembly.
Conclusion
Acoustic design in mass timber construction is no longer a fringe concern. It’s a core pillar of performance, occupant satisfaction, and project success.
From floor isolation mats and dry subfloors to flanking mitigation and early consultant engagement, the path to quieter mass timber buildings is paved with proven, practical solutions. And with recycled materials like GenieBoard and GenieMat FF, those solutions don’t have to come at the cost of sustainability.
As Callaghan puts it: “We’re using end-of-life materials to stop you from hearing the guy upstairs snoring.”
That’s acoustic performance with a conscience.
Frequently Asked Questions
- How do airborne and structure-borne sound differ in mass timber buildings, and how are they measured? Airborne sound (like voices or music) is measured by Sound Transmission Class (STC), while structure-borne sound (like footsteps or vibrations) is measured by Impact Insulation Class (IIC). Mass timber’s lower density and lack of drop ceilings make these harder to control.
- What specific wall assembly is recommended for improved acoustic separation? A double stud wall with a 1" air gap can achieve STC 60–63. For tighter spaces, resilient isolation clips like GenieClips can help decouple drywall while maintaining acoustic performance.
- Why are traditional concrete toppings often replaced in mass timber buildings? Concrete introduces moisture and weight. Dry systems using GenieBoard avoid both while matching performance, saving time, and reducing foundation and framing loads.
- How does the absence of ceilings impact sound performance in mass timber? With no suspended ceilings to absorb or block noise, floor assemblies above must do all the work, making floor design critical for both airborne and impact sound.
- What’s the best time to bring in acoustic expertise? Early design development (DD). Waiting until construction begins limits options and costs more. Early decisions enable flanking control, optimized assemblies, and potential structural savings.
Tired of Mass Timber Challenges Derailing Your Projects? Learn How to De-Risk & Deliver Them.
Lead mass timber projects with confidence — and leave delays, redesigns, and budget blowups behind.
✅ Solve early-stage design, sourcing, insurance, permitting, code & cost hurdles before they derail your project.
✅ Find technical answers on design, detailing, procurement, embodied carbon ROI, hybrid systems & more.
✅ Build relationships with developers, GCs, architects, and engineers shaping mass timber’s future.
Get your ticket— and get the insights, skills, and network to deliver mass timber projects successfully.

Latest episodes
Building a CLT Plant: Why Starting Small Can Beat Starting Big with Ledinek's Jaka Bradac
How mass timber gets made, what plant size changes, and what Ledinek's Jaka Bradač has learned selling CLT and glulam lines on both sides of the Atlantic.
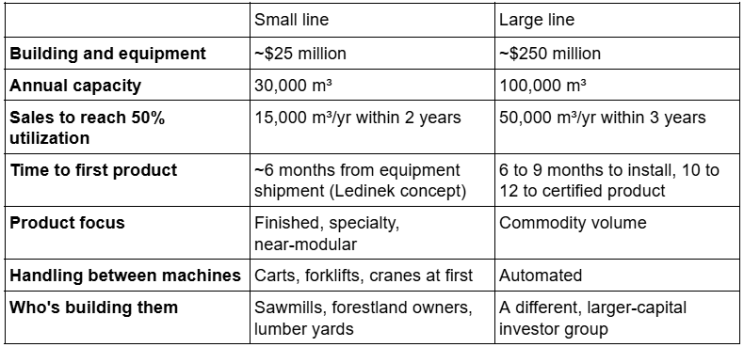
Picture two CLT plants in the same town, chasing the same customers. One cost $25 million. The other cost $250 million. At the start, they'd win the same share of the market. One of them has to sell more than three times as much to stay on track.
That's the case Jaka Bradac makes for starting small. He's Sales Executive for North America at Ledinek Engineering, a Slovenian company that has designed and built more than 35 CLT and glulam lines. Most North American plants were built big, sized for demand expected three to five years out. Bradač argues the next wave should look different, and his reasons come down to four things: how much you have to sell, how fast you get to product, how you grow, and how much control you have over your wood.
Here's how the two compare.
This article is just one part of the newsletter where we cover who and what’s shaping the mass timber industry.
👉 Stay ahead of the mass timber industry & grow your network. Join Our Newsletter
How is CLT made? From log to finished panel
Every CLT plant, large or small, turns boards into panels the same way. Cross-laminated timber (CLT) is a structural panel made by gluing layers of lumber at right angles to each other. Glulam is a beam or column with every lamination running the same direction. Both follow the same path.
Example of a CLT production line. Credit: Ledinek
Where the lumber comes from
A sawmill cuts the log to a pattern set by a scanner and optimizer, sorts the wet boards, and kiln-dries them, typically to about 12% moisture content. (ANSI/APA PRG 320-2025, the North American CLT standard, caps it at 16%.) The boards are planed and graded visually, by X-ray, or by machine stress rating (MSR), which bends each board to measure stiffness.
Inside the plant
A graded board still carries knots, cracks, and splits. The plant regrades it and cuts out the defects. The clear pieces are finger jointed into long laminations. That joint is watched closely: glue application, joint pressure, and friction through the press are all monitored, and joints get daily tension tests. Then the laminations are planed, the surfaces prepared, and glue applied, with ambient conditions recorded. The press applies a specified load for a specified time. A finishing step completes the panel.
Bradač calls the finger jointer, the planer, and the press machine centers. They're the expensive part of a line, and they set its capacity. Everything that moves wood between them is handling: automated conveyors in a big plant, carts and forklifts in a small one. Handling is where a small line can save the most up front, and where it finds capacity later.
TAKEAWAY: Large or small, every CLT plant runs the same steps: regrade, cut out defects, finger joint, plane, glue, press, finish. Scale changes how those steps are automated and connected. It doesn't change what they are.
How do European and North American CLT plants differ in size and wood supply?
In Europe, CLT grew out of glulam. The first producers were attached to sawmills, and some were tied all the way back to logging. The boards that reached their lines came from their own mills, not the open market. Those plants started small and grew over time. That control shows up in the product: a typical European CLT layup mixes a wide range of layer thicknesses and grades, because the producer decides which boards go where.
North American plants mostly skipped that path. They were built at large scale “from zero,” and all but a few buy their lumber on the open market, usually as graded, kiln-dried dimensional lumber.
How does plant size change a CLT plant's risk?
Capital comes with a production target. The bigger the investment, the more the plant has to produce and sell to cover it, and the sooner it has to get there.
But plant size doesn't change demand. Go back to the two plants in the same town. At the start, they win the same customers and the same orders. What changes is how much of each line those orders fill.
The small plant needs to sell half its 30,000 cubic meters, or 15,000 a year, within its first two years. The large plant needs to sell half of 100,000, or 50,000 a year, within three. If both win the same orders, the small plant is on track. The large plant is running at a fraction of its capacity. The small one, as Bradač puts it, doesn't have to stress as much.
That pressure decides what each plant can make. A large plant only makes money with its press full, so it has to chase commodity volume. Specialty projects don't fill an operation that size. A small plant can take that work, and specialty is where the margin is.
The volume target also takes a long time to reach. In Europe, the companies running 100,000 cubic meters a year got there after 20 years of winning business.
TAKEAWAY: A large plant carries more risk because it has to sell more, sooner, into the same market. A small plant can hit its target on fewer orders, and that leaves room for higher-margin specialty work.
What should a small CLT line make?
A small line wins on product, not volume.
One of the smallest lines Ledinek has built, in Europe, has a press that makes panels up to 45 feet long and runs four to five cycles a day. The plant doesn't sell bare panels. It goes a couple steps further to serve the housing market: insulation and cladding installed at the plant, ready to go. It's a niche, value-added product. It doesn't need to compete with the large manufacturers for big projects.
Bradač sees the same model fitting North America: a more complete, modular or prefab product that simplifies the purchase and grows the market.
But that model doesn't lock a small line out of larger work either. A $25 million plant can still run eight CLT press loads a day. It needs longer delivery times on a big job, but it can deliver. And size alone doesn't guarantee throughput. Unless a plant's downstream formatting line is fully automated across several machine centers, it runs into bottlenecks anyway.
How fast can a CLT plant get product out the door?
A 100,000 cubic meter line takes six to nine months to install and 10 to 12 months to reach first certified product, roughly. Every situation is unique.
Ledinek's 30,000 cubic meter concept is built to move faster. Product comes about three months after installation starts. Then comes roughly a month of commissioning to dial in reliable bonds, and three to four weeks for APA certification. That's about six months from the day equipment ships from Europe to product on the U.S. market.
How does a small CLT line add capacity?
Start with the machine centers. Move wood between them by cart, forklift, or overhead crane. Automate the links later, when the orders justify it.
Full automation between machine centers is what drives a line's price up. Plenty of North American plants still run on hand work, and a new pilot plant can do the same.
Growth then comes in two steps. The first is utilization. Machine centers are built with growth in mind, so they are rarely the limit. Handling is. Wood doesn't reach the machine because the forklift driver is on a coffee break and half an hour is gone. Or it can't leave because something backed up downstream. Tightening that up adds roughly 20 to 25% capacity from equipment you already own. The second step, if you need to double output, is ordering another line.
“It's not the machine centers. It's mostly the handling around the machine centers.” - Jaka Bradač, Ledinek
No two lines come out the same. Each is customized to the owner, which is why machine selection matters at the start. It sets how much headroom you have to grow into.
What this means if you're considering a CLT plant
- Size the line to the orders you can win, not the market you expect.
- Spend first on machine centers. Move wood manually until volume pays for automation.
- Make a product your line can add to: finished, specialty, higher margin.
- Get close to the wood. Own a mill, partner with one, or build next to one.
- Choose machines with growth potential in mind. Your first 20 to 25% of growth comes from handling, not new equipment
If you're exploring mass timber for your own projects, your going to need the team, knowledge and connections to make it successful.
Frequently asked questions about CLT plants
- How is CLT made? Kiln-dried, graded lumber is regraded at the plant and trimmed of defects such as large knots and cracks. The clear pieces are finger jointed into long laminations, planed, and glued. Layers are laid at right angles to each other and pressed under a specified load and time, then finished.
- How much does a CLT plant cost? It depends on capacity and automation. Ledinek’s Jaka Bradač contrasts roughly $25 million for a small plant with $250 million for a large one as an illustration. Published European projects include about €30 million for a 100,000 m³ plant (2017) and €130 million for 140,000 m³ including sorting and planing.
- How long does it take to build a CLT plant? According to Bradač, a 100,000 m³ line takes six to nine months to install and 10 to 12 months to reach first certified product. Ledinek’s 30,000 m³ concept is designed to produce certified product for the U.S. market about six months after equipment ships from Europe.
- What is the difference between CLT and glulam? CLT is a panel made from layers of lumber glued at right angles, used for floors, roofs, and walls. Glulam is a beam or column made from laminations glued with the grain running the same direction. Both are mass timber products and share much of the same production process.
- Can CLT be made from hardwood? Yes. Yellow poplar was added to ANSI/APA PRG 320, the North American CLT standard, in its 2025 edition. University testing found yellow poplar CLT comparable in strength and stiffness to Southern pine CLT. Hardwood lumber is still appearance graded rather than machine stress rated, which remains a gap for glulam.
- What wood species are used for CLT in North America? PRG 320-2025 covers softwood groups including Spruce-Pine-Fir, Douglas Fir-Larch, Hem-Fir, Southern pine, and others, plus yellow poplar.
New Glulam Species, 3D-Curves & Impossible Projects with Art Massif
Somewhere between the era of steamboats and the world wide web, the industry lost the muscle memory to build with heavy timber. We were putting up NLT and glulam buildings before 1950. But then, everything switched to steel and concrete, and the expertise walked out the door with it. So when an architect brings an ambitious timber concept to the table, too often they hear “Not feasible. Too expensive. Switch that part to steel. Nobody can build it.”
Dave Savard and Geneviève Constancis, ing.f./for.eng. of Art Massif | Wood Structure spend their days proving those answers wrong. In this piece, Dave and Geneviève walk through Aspen Pure, their new structural glulam made from quaking aspen, the free-form theater canopy they just delivered for Hudson Valley Shakespeare, and why so many timber designs get talked down before anyone checks what's actually possible.
This article is just one part of the newsletter where we cover who and what’s shaping the mass timber industry.
👉 Stay ahead of the mass timber industry & grow your network. Join Our Newsletter
A Structural Product From a Tree Nobody Wanted - Aspen Pure
"It really started from the forest," Geneviève says.
One of Art Massif's four partners, the company's production director, was harvesting quaking aspen on his own land and couldn't get past how white the wood was. It was just too beautiful to waste on the usual fate. Because that's what quaking aspen has been, one of the least valued trees in North America. It goes to pulp for paper. It goes to shipping pallets. Almost no value-added products, and almost no economic return for the communities that harvest it.
So they started testing it. With the right moisture content, the right drying, and the right sanding, it now has a home in the structural glulam market.
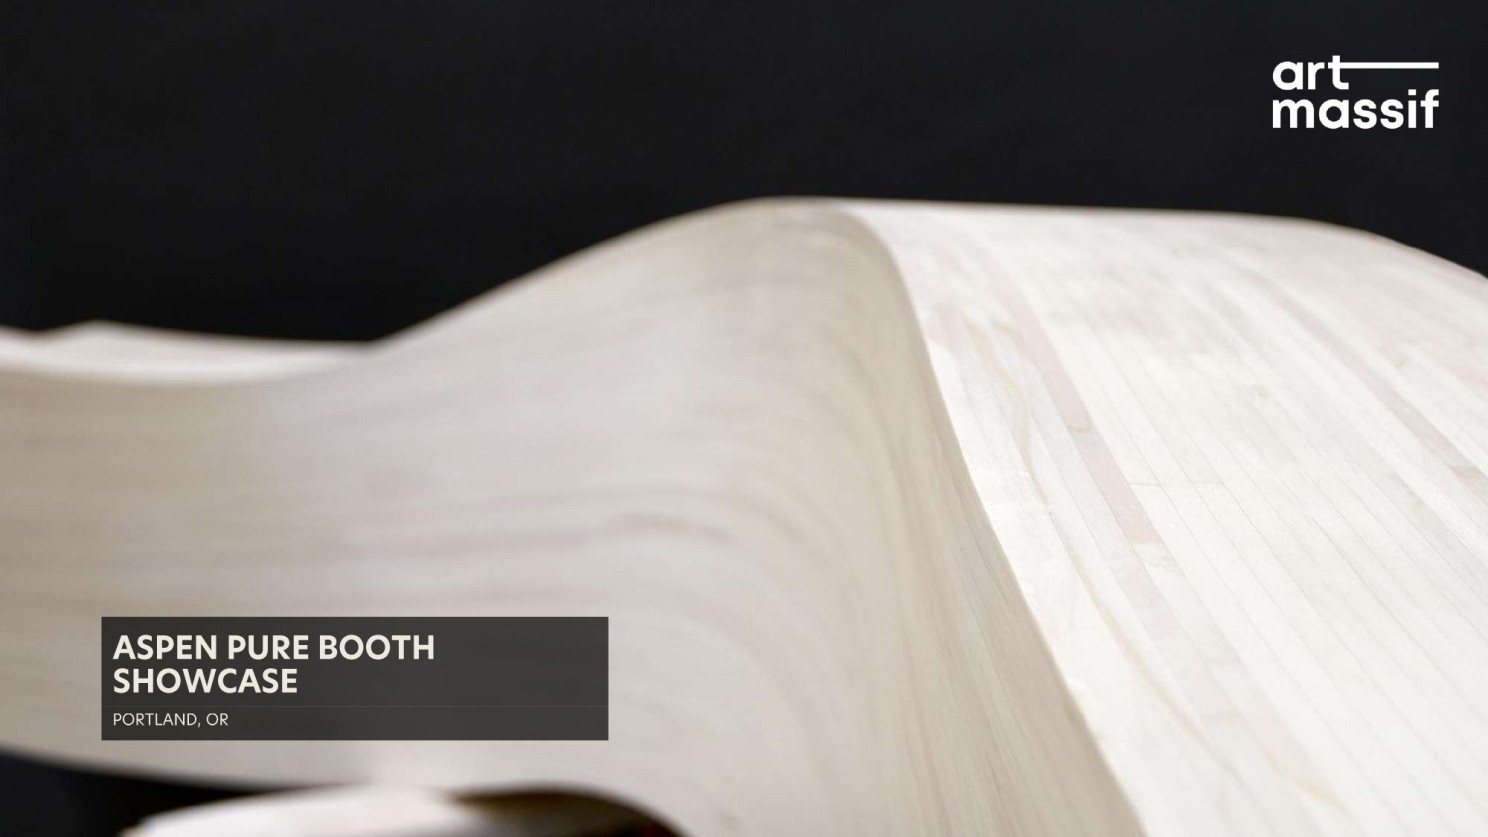
What came out is a different architectural language for glulam. Lighter, brighter, more uniform, with fewer knots and less character than Douglas Fir, southern yellow pine, or spruce. Nothing wrong with the traditional species in the right setting. But Aspen Pure gives architects and designers a modern look they've been asking for and couldn't get.
The performance is there too. From Art Massif's testing, the design values are equivalent or superior to spruce. Part of that comes from selection: they sort and grade the fiber themselves with their own equipment, so only the best material makes it into the structural product. Right now Aspen Pure runs as the equivalent of a 20f-EX layup, and they believe a more detailed process could push the values higher.
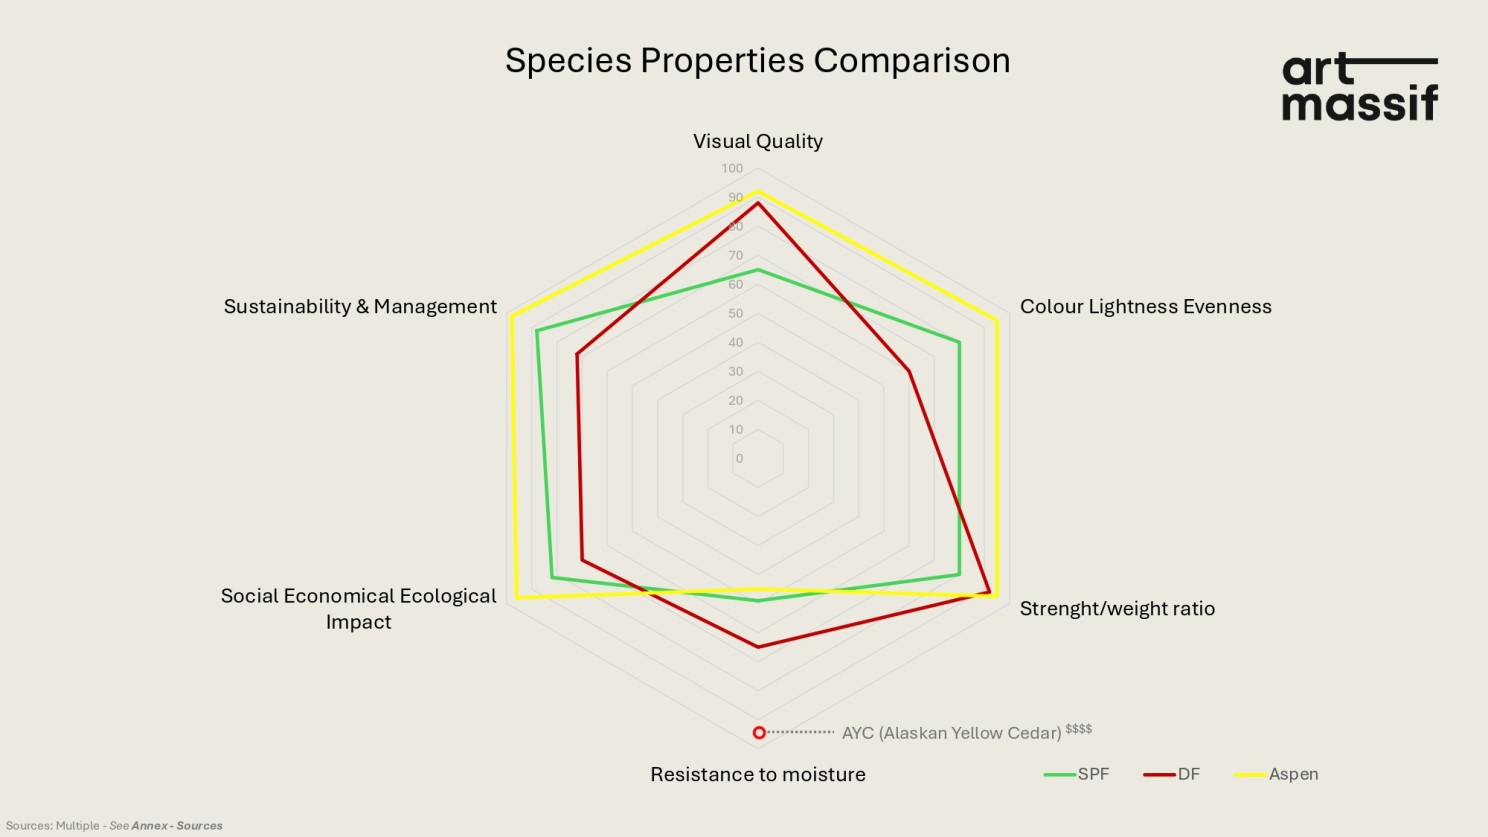
None of it was plug and play. Every species has its own character. Aspen can't be graded the way other species are graded, and it can't be kiln dried the same way either, so Art Massif developed its own drying methods to protect the fiber properties. Sourcing had to be built from scratch too, because structural-grade aspen supply didn't exist in the market.
They launched Aspen Pure in Spring 2026, and the reception from architects and designers has been strong.
But, you might have seen something else in the mass timber world challenging assumptions on what’s possible. And Art Massif played a role there too.
The Theater That Had to Grow From Its Site

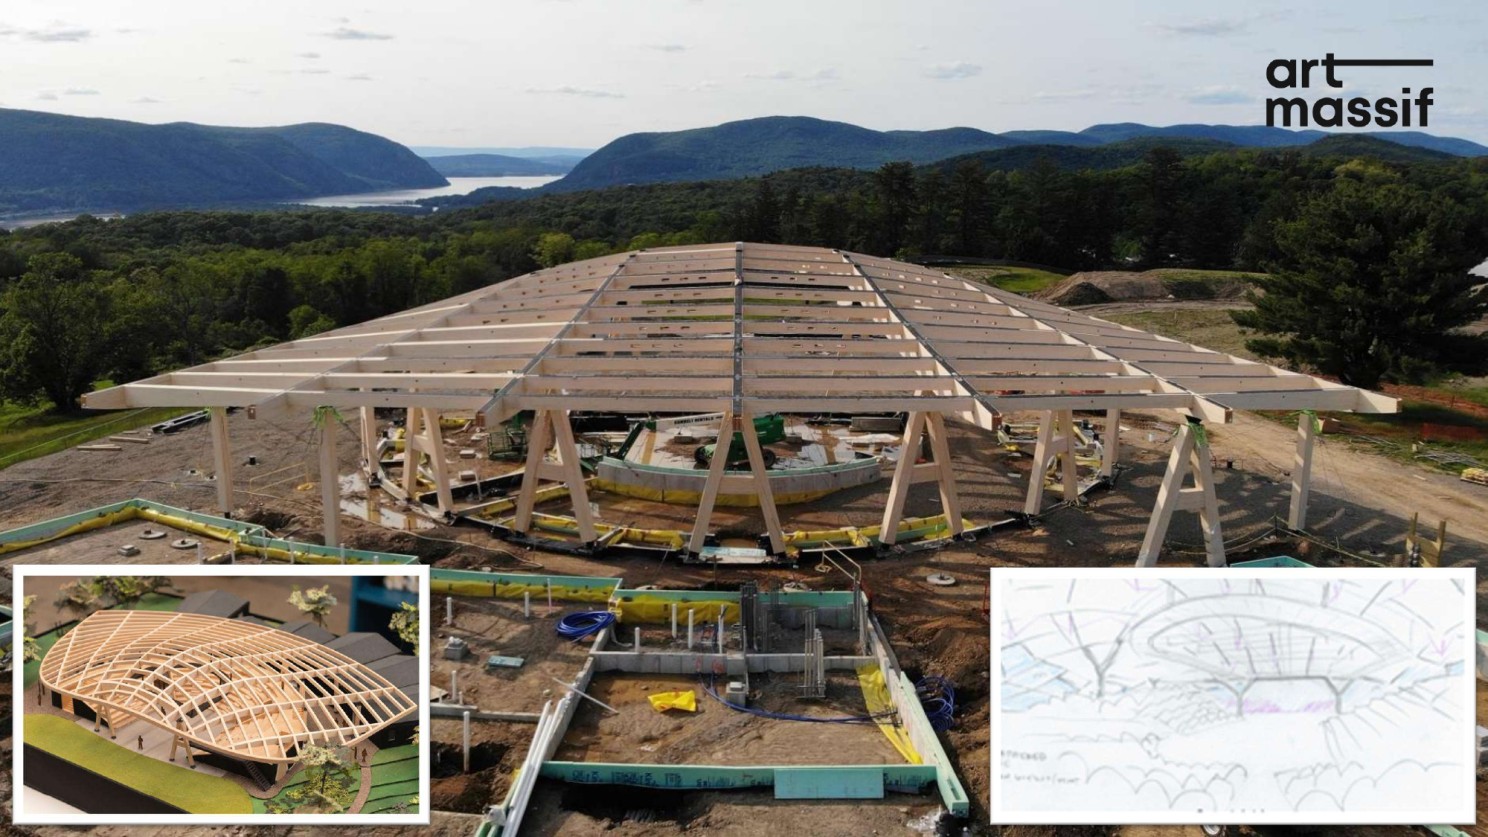
Hudson Valley Shakespeare's new permanent home, the Samuel H. Scripps Theater Center, opened with a ribbon cutting this spring.
The site sits in the middle of a valley with a mountain behind it, and the architect's intent was a building that belongs to that scenery, almost like it had grown from the site itself. That meant curves in every axis and every angle. It also meant a nonprofit client with a real budget ceiling and zero appetite for compromising the design.
The path between those two things was a comprehensive design assist phase. Months of it, with the architect, the engineer of record, the construction manager, and Art Massif's team working through hundreds of small challenges to make the structure constructible. Dave's description of the team: “no egos, nobody fighting for a bigger piece of the pie, everybody solving problems.”
Three moves from that phase stand out.
Straighten what nobody will notice.
The most important members stayed fully curved in both axes. But some elements, like certain purlins, could be straightened without changing the overall look. You can't spot it in the finished structure. Curves cost time and money, so they saved them for where the design needed them. That kept the project on budget and on schedule.
Borrow strength from what's already there.
A theater needs a steel catwalk regardless. The team put it to work as a compression ring, pulling load off the wood structure. Smaller connections, smaller members, lower overall cost, from a piece of steel the building was getting anyway.
Prove it out.
The original design had the roof in another material, because the team had doubts the timber decking couldn't follow a roof curved in all angles. Art Massif was convinced it could. So they built a full-size mock-up in their shop. Nobody asked for it, and nobody was paying for it. But the mock-up proved it was possible, and it showed the team how committed Art Massif was to the timber succeeding.
"This is where our dream thrives," Dave says of that phase. It's where their engineers and project managers find their value, working shoulder to shoulder with the architect and EOR until the ambitious version of the building is the buildable version.

Every one of those solutions existed because someone kept asking what was possible. Geneviève's concern is how rarely that happens.
Why Architects Stopped Asking
Art Massif has a phrase they repeat to designers: architects are allowed to ask for what they want.
That phrase shouldn't need to exist. Of course an architect asks for what they want. Except in mass timber, they often don't, and Geneviève traces it back to that lost expertise. Wood is an old structural material with a young workforce. When construction switched to steel and concrete, the knowledge of how to design and engineer with timber faded across every stakeholder group. Few schools in North America teach it. Architects are excited about the material, but if the engineers, builders, and reviewers around them aren't educated on it, the whole thing feels risky.
And risk gets answered with myths. It's not feasible. Change that part to steel, wood will be too expensive. Nobody can manufacture it. The design shrinks a little at every meeting until the ambition is gone.
Geneviève's answer is simple. Ask for it, and ask the right person for it. The manufacturers doing this work at a high level exist, and the capabilities go further than most of the industry realizes.
Asking is half the equation. The other half is a partner built to say yes.
Built to Say Yes
There's no machine you can buy off a shelf that makes 3D curved glulam. That's the first thing to understand about how Art Massif works. Their production team runs on the same everything's-possible mindset as the front office, so when a project calls for something no equipment exists for, they adjust their machines or build new ones.
How a 3D Curve Gets Made
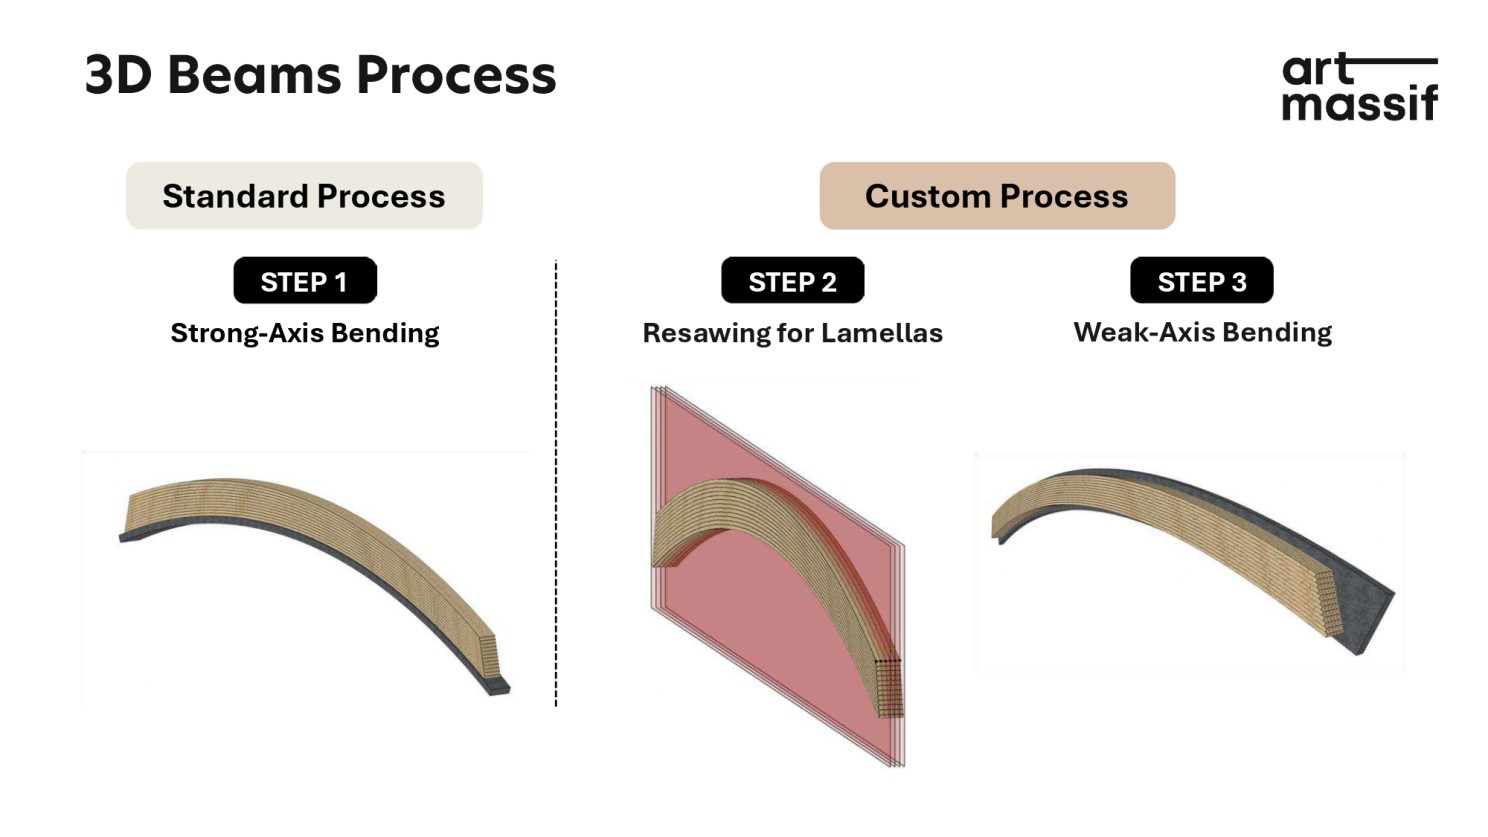
For a tight-radius member curved in both axes, it's a three-step process. First the member gets curved in one axis in the standard press. Then it's resawn into lamellas. Then those get curved in the second axis on a custom press Art Massif built specifically for 3D work. It takes real time and energy, and as Dave puts it, "it's not a cheap cubic meter." Which is exactly why they simplify shapes anywhere it won't change the design intent.
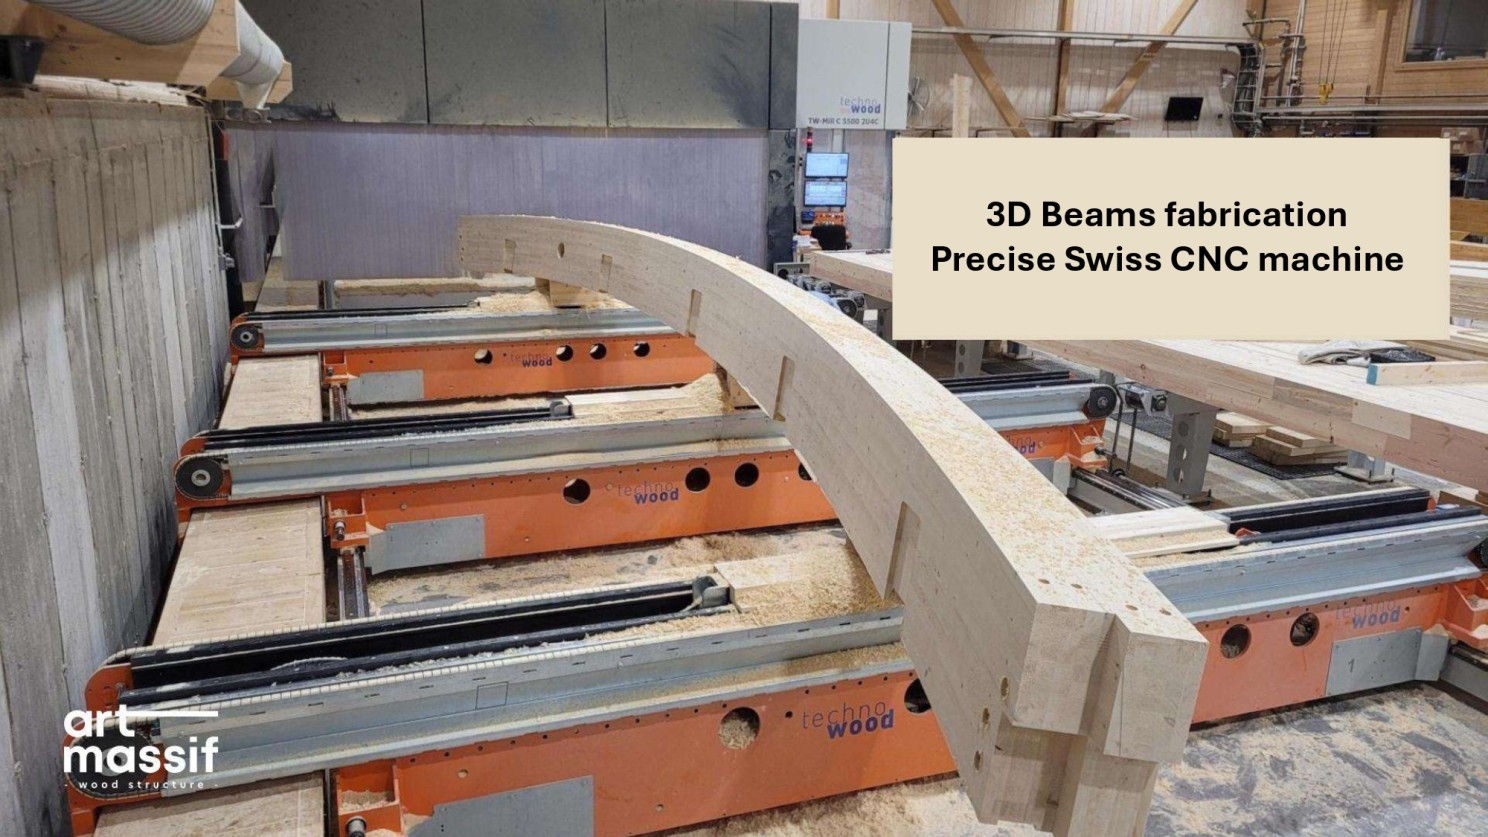
The equipment is one piece of a bigger structure: Art Massif can own nearly everything on a project when the project requires it. Design build or design assist from a blank page, backed by a large in-house engineering team. CNC fabrication on a high-end Swiss machine they acquired in 2021, precise enough that complex members in all angles fit perfectly on site. Finishing, fabrication, and installation with their own crews. And something rare in the industry: connection design and steel fabrication in-house.
The reason is de-risking. Every additional interface on a complex project is another chance for miscommunication, delays, or budget problems. Art Massif partners with others the majority of the time, and gladly. But where the right expertise didn't exist externally, they built it internally. For the client, that means one conversation and one accountability structure.
Where does all that capability aim? Geneviève's shorthand is quality or complexity. The 100,000 square foot, ten-story square box with huge volume is not their type of project. Theirs is the 15,000 square foot luxury home, the 30,000 to 40,000 square foot museum or arts center, the condo amenity space. Right now they're in construction on the 12th story of a condominium building, a penthouse level with a gym, pool, and spa in high-quality glulam.
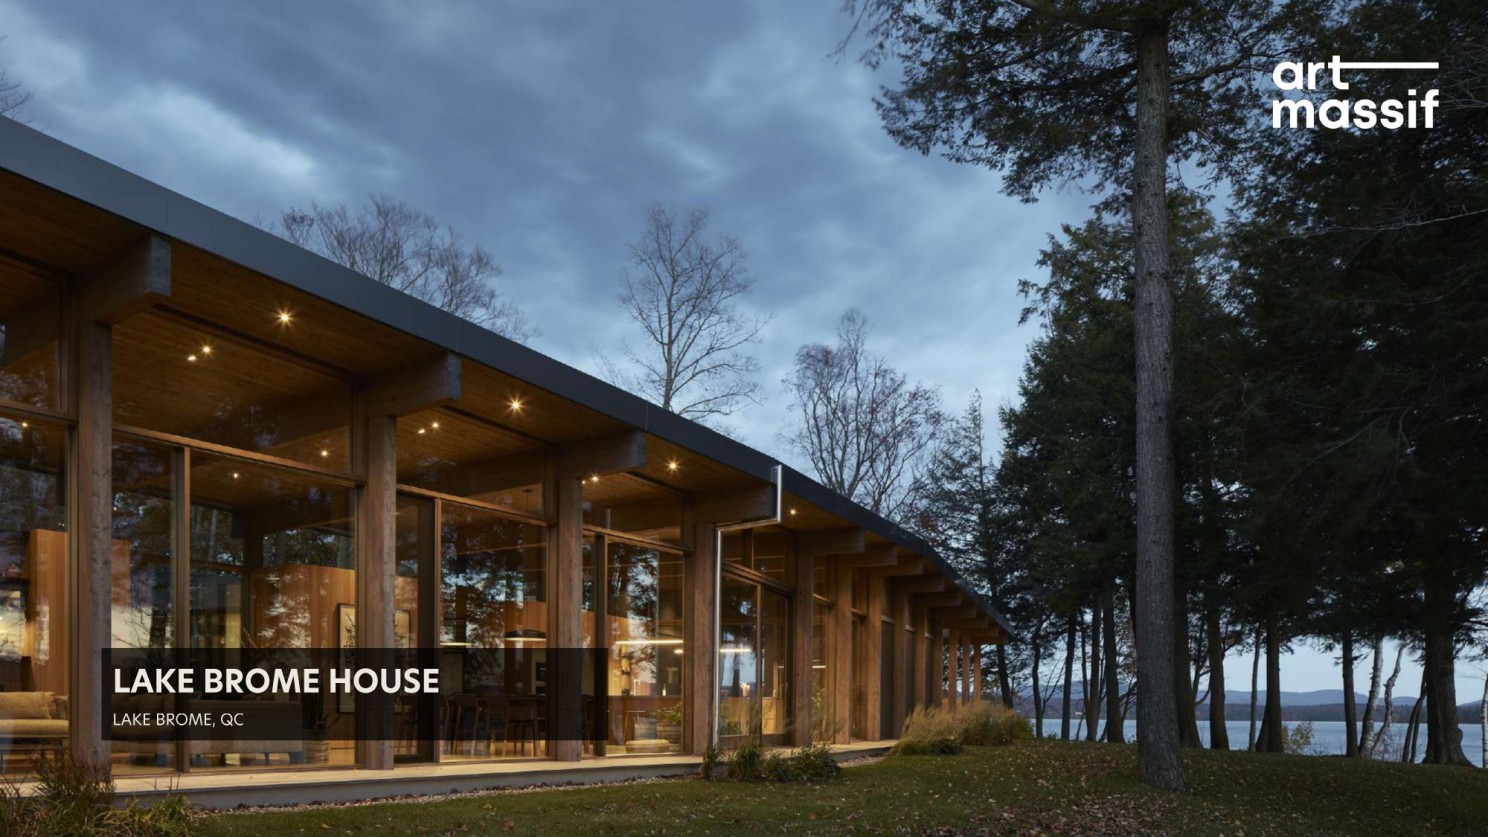
All of it circles back to the advice they'd give any architect starting a first timber project.
Talk to Someone Who Knows
Geneviève's day-one checklist is short. Think about your grid. Think about efficient radii and repetition. But her bigger point sits above all of that: talk with someone who has real experience before you lock in your design. Timber is a different material from steel and concrete, and it changes how you take the very first step. Maybe in 20 years every school will teach it and this conversation won't be necessary. Right now, the shortcut is borrowed expertise.
Dave's version: involve your producer. Art Massif keeps a full pre-construction team ready to pick up the phone at any stage of a project, and they'd rather invest time educating a design team early than watch anyone rework plans mid-project against a budget and schedule.
And when the doubts start arriving in meetings, remember the phrase. Architects are allowed to ask for what they want.
If you're exploring mass timber for your own projects, your going to need the team, knowledge and connections to make it successful.
Stop Waiting for Better Building Products w/ Zenon Radewych of WZMH Architects
The building industry has a strange relationship with its own materials. Most of the people designing, engineering, and building things treat the products and materials as a fixed list of options. If the available products don't quite do what the project needs, the project bends to fit the products.
But not all. Some people have stopped accepting that. Instead, they’ve leaned into the “what if we had this…” or “what if we made that?” They've built the inventor’s mindset into their companies, literally and figuratively.
Zenon Radewych is one of them. He's a principal at WZMH Architects, a 65-year-old firm based in Toronto, and the person behind @sparkbird, their R&D lab where they don’t let what’s currently available limit their options. And now, they’re looking at mass timber.
This article is just one part of the newsletter where we cover who and what’s shaping the mass timber industry.
👉 Stay ahead of the mass timber industry & grow your network. Join Our Newsletter
A Lab Isn't a Department. It's a Permission Slip.
When most people in this industry hear “R&D lab,” they picture a big space with a big budget. A formal program. A roadmap. Milestones. Maybe a Ph.D. or two.
sparkbird isn't that. It's a corner of the WZMH office where people work on things that interest them, often without a deadline, often without a guarantee that anything will come of it. Ideas come from client meetings, from frustration with how a project went, from a side problem that showed up while solving something else. Some of those ideas take a month. Some take ten years. Some get shelved. Some get handed off to industry partners who can actually take them to market.
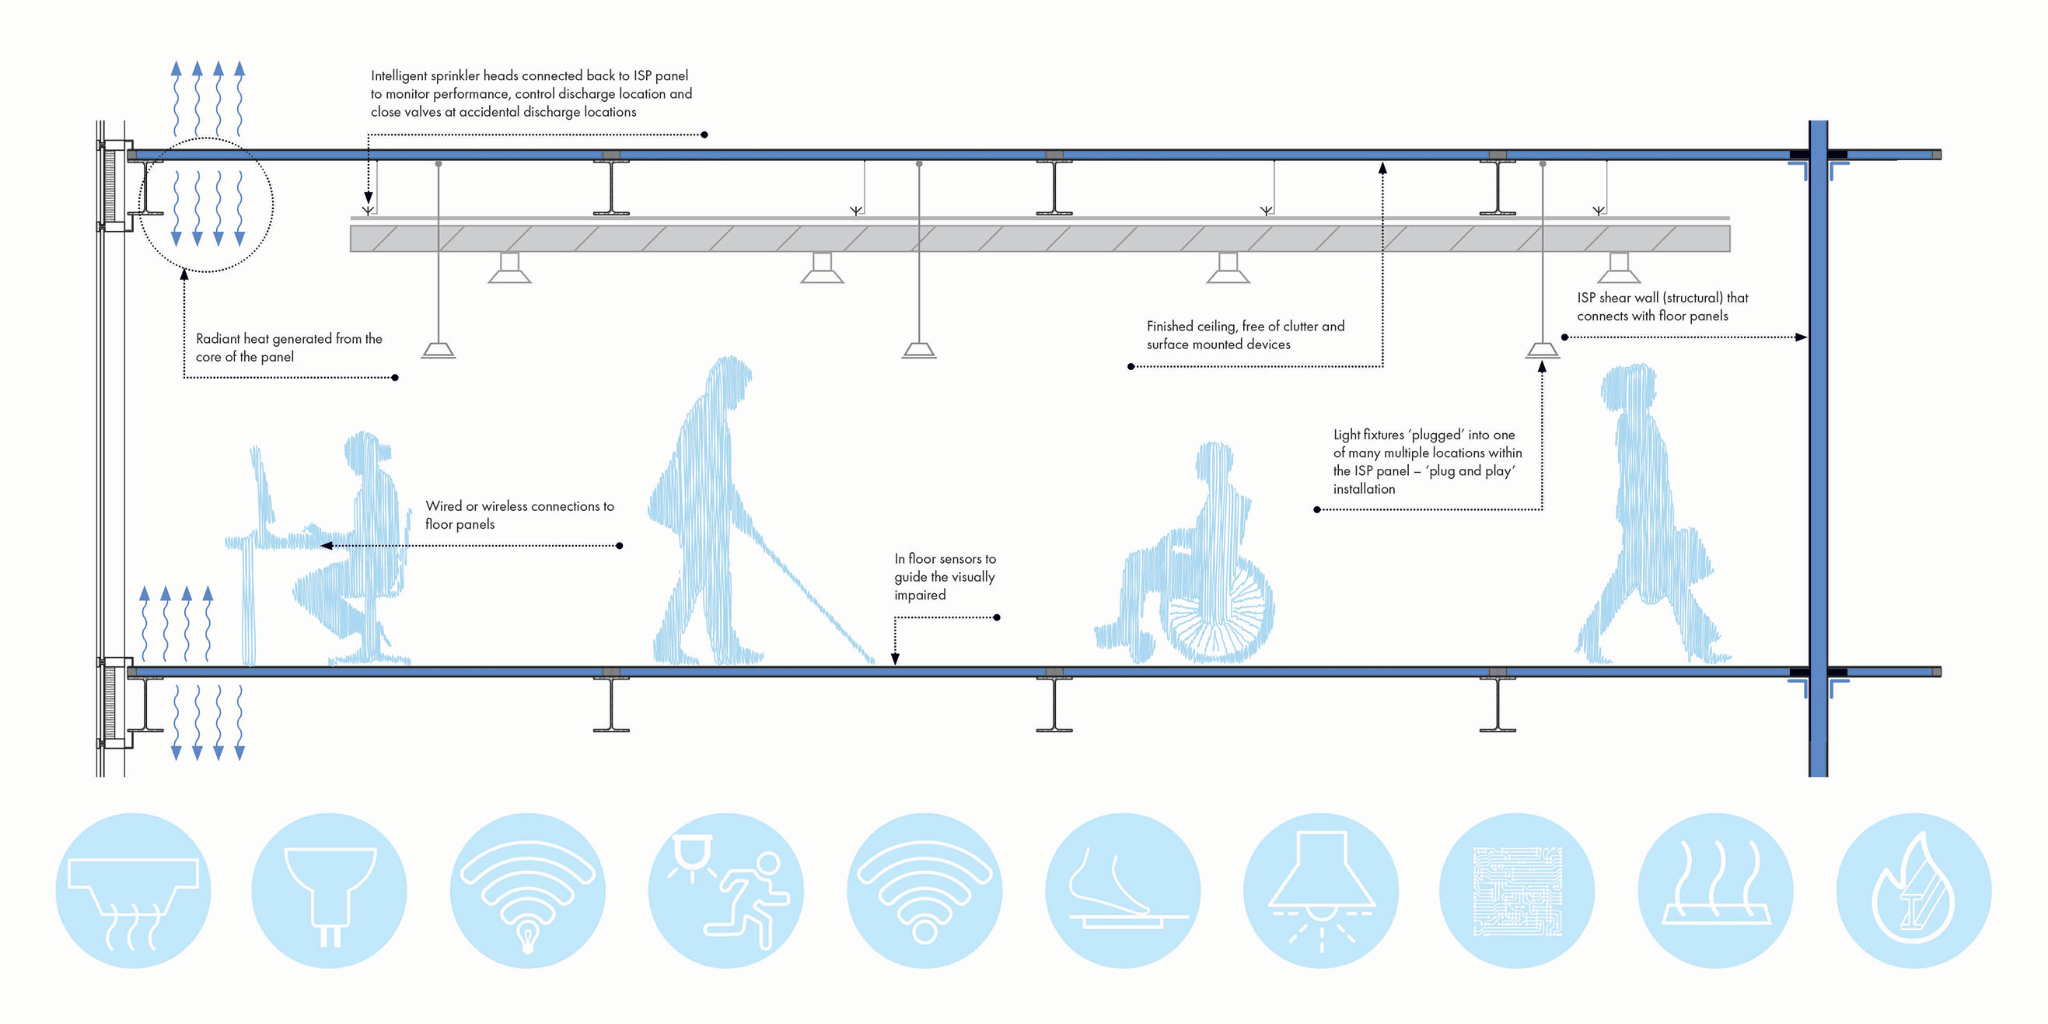
sparkbird's first invention, the Intelligent Structural Panel, started in 2017. It takes all the components and processes that go into constructing a floor and shear wall in a building and combines it into one product, including the mechanical, electrical, and IT. Microsoft saw an early mockup, invited WZMH into their IoT (Internet of Things) and AI Insiders Lab, and accepted them as the only architectural firm in the program.
When it comes to mass timber, four projects are live in the lab right now (and probably more by the time this article comes out - they move fast).
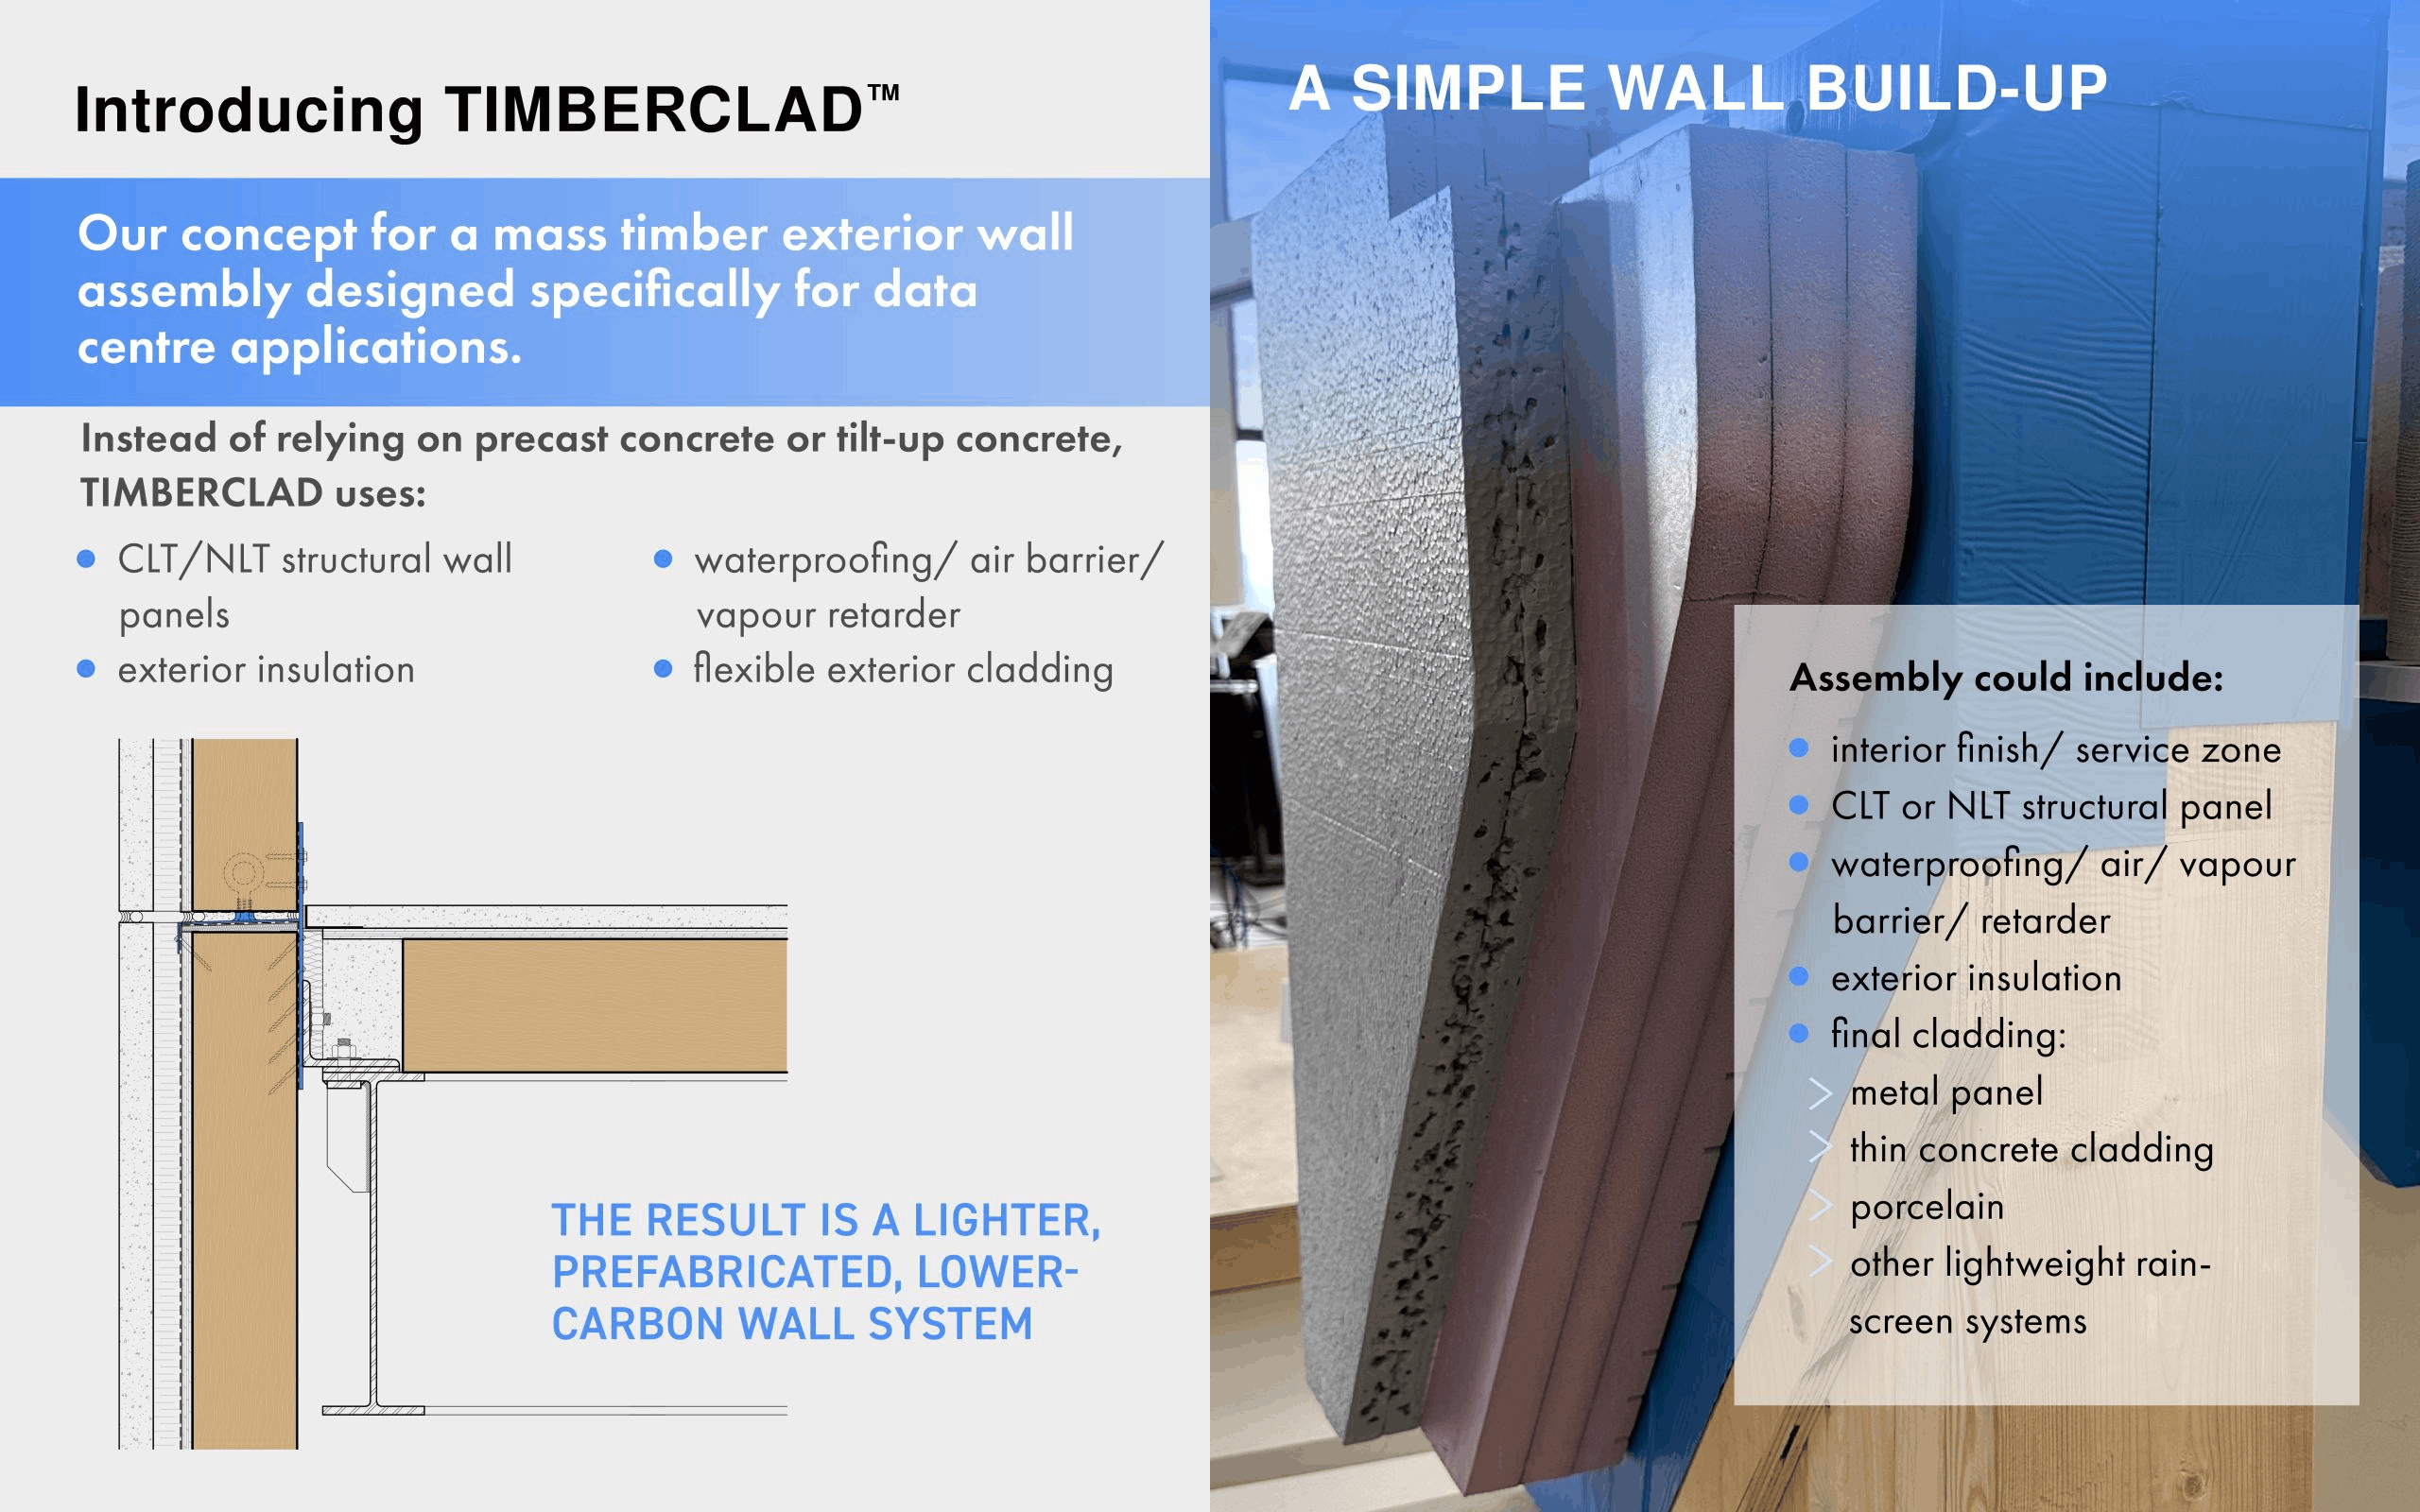
TIMBERCLAD™ is a mass timber exterior wall system aimed at data center construction. CLT or NLT panels paired with exterior insulation, air and water barriers, and flexible cladding options, designed to replace precast or tilt-up concrete walls. Lighter, prefabricated, lower-carbon. WZMH has a full-scale mockup of it in their office and is testing whether GripMetal between timber layers can improve composite action and stiffness under wind loading.
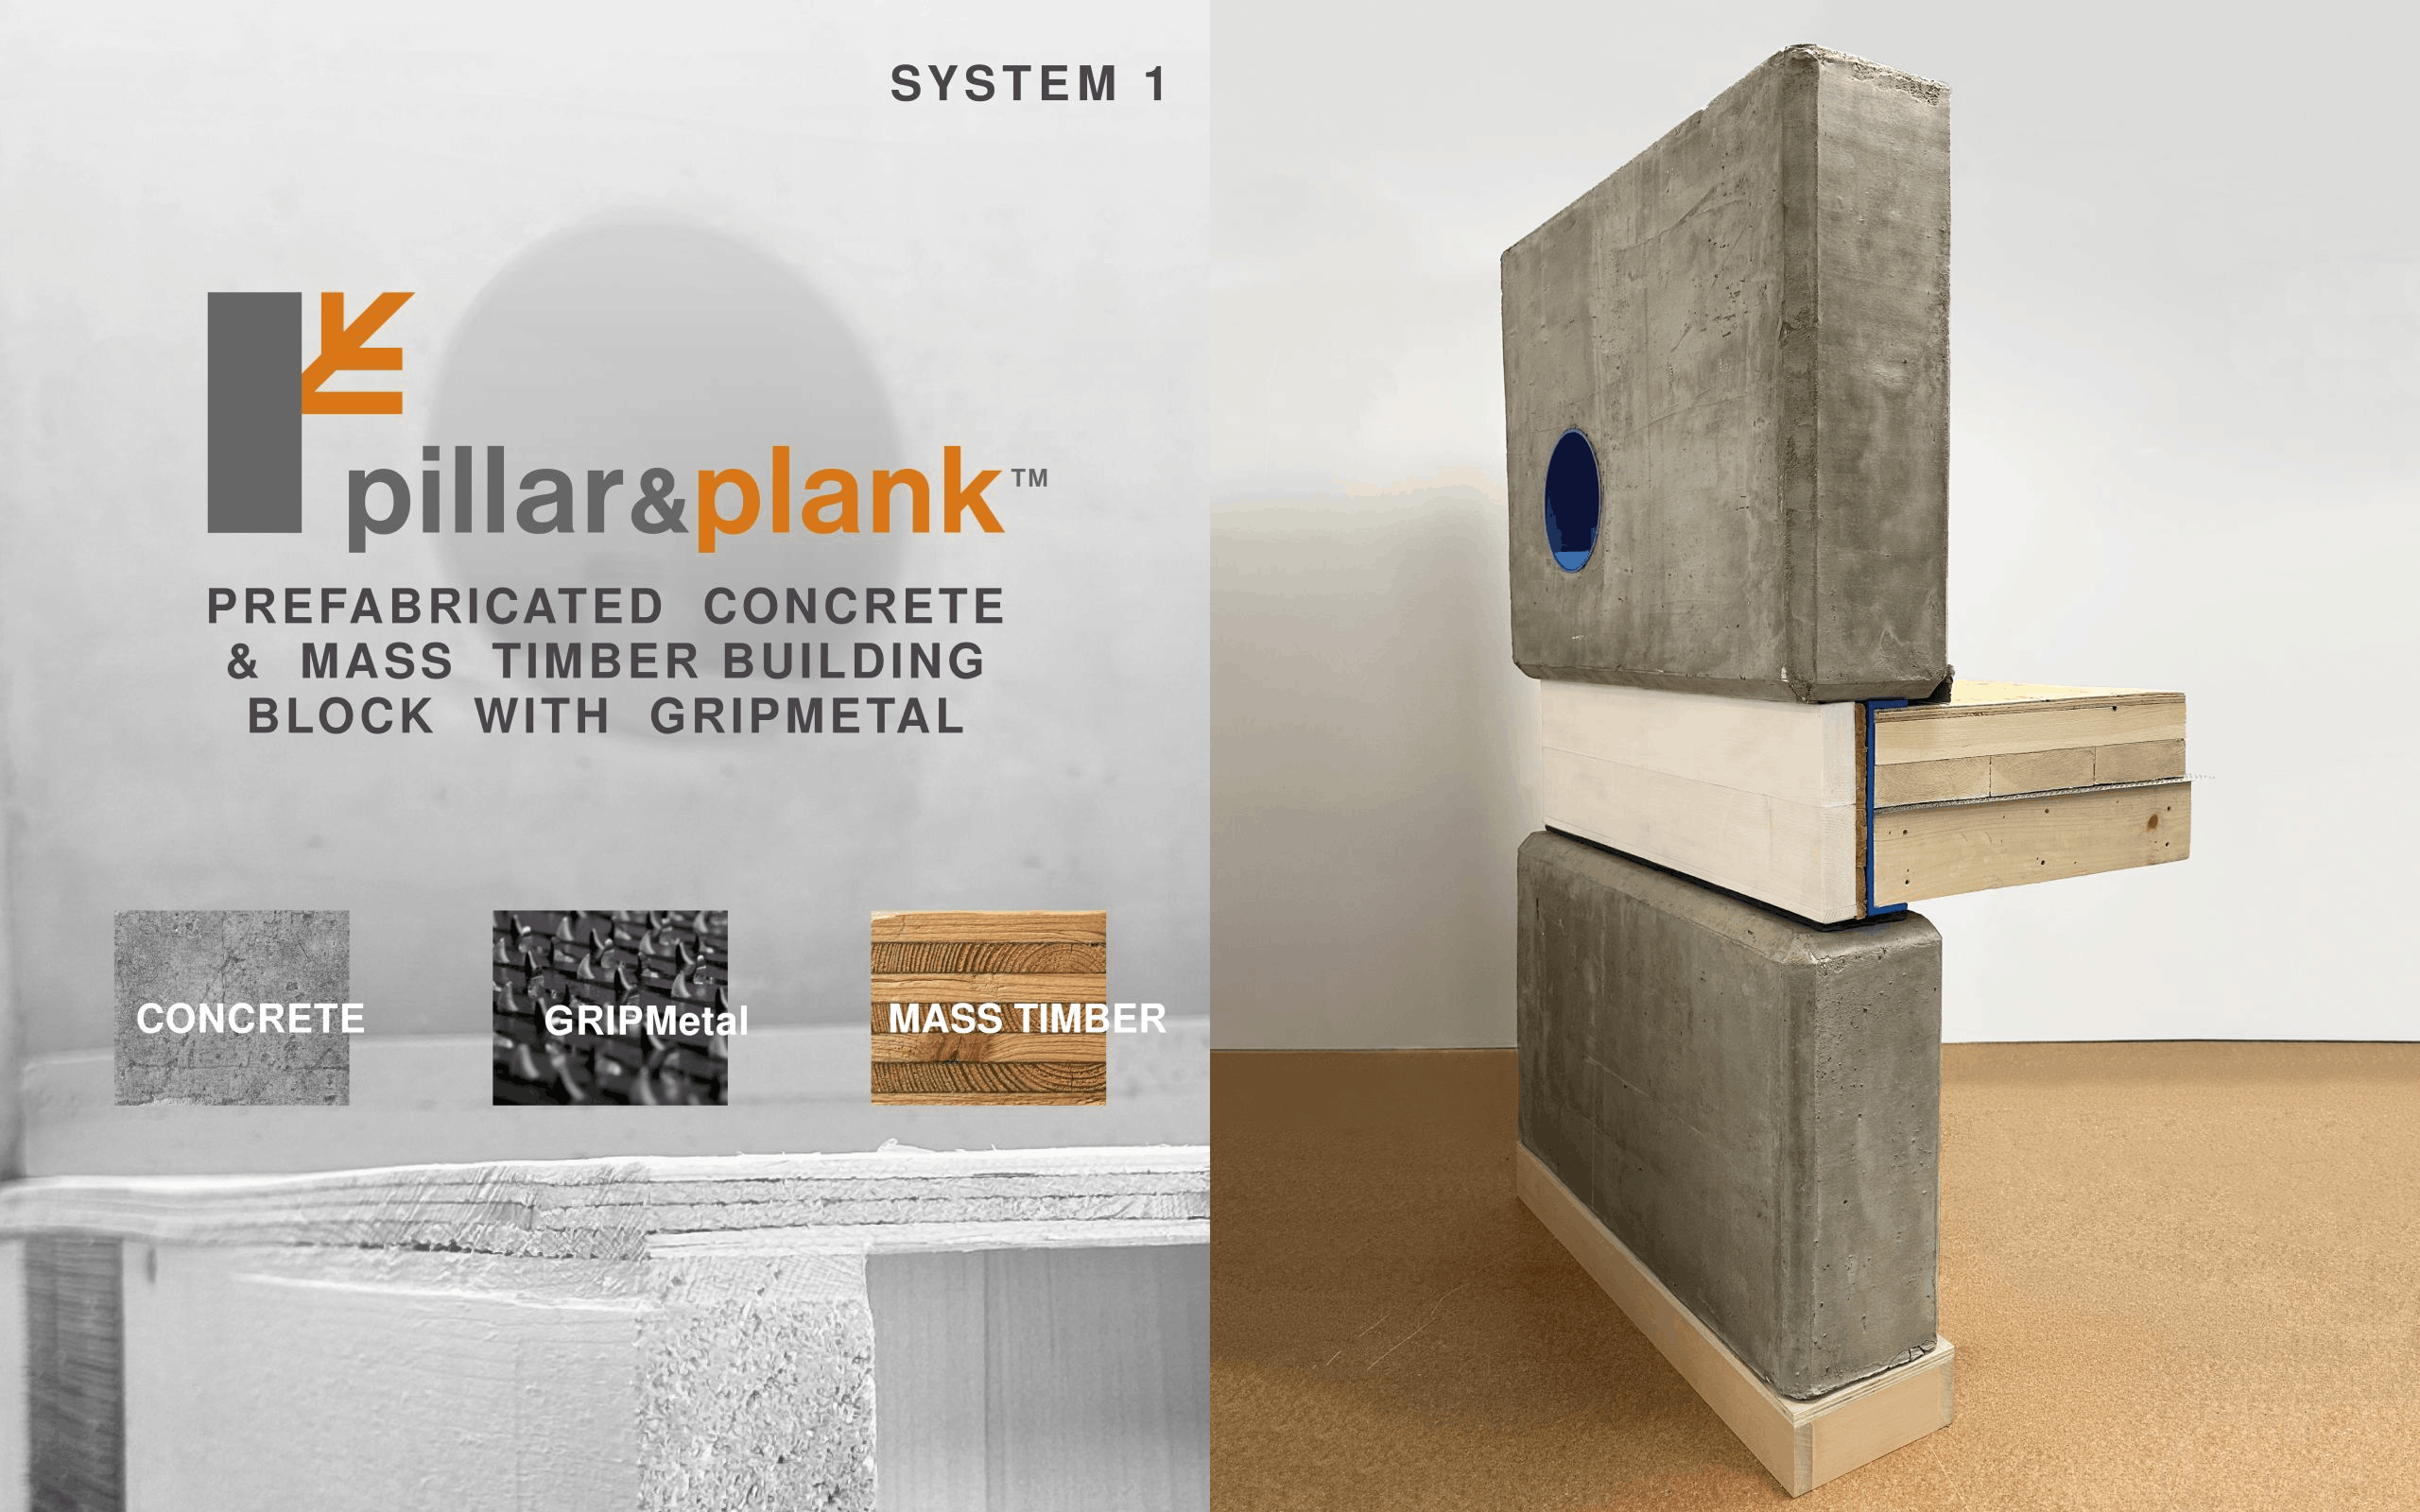
Pillar & Plank is a hybrid system aimed at multi-family residential, where clients want mass timber but are getting hit by cost and lead time. The structure combines precast concrete piers with mass timber floor panels, with or without GRIPMetal reinforcement. Precast plants exist across Canada, which helps with supply chain and price certainty. The pitch is the same as most good hybrid systems: use each material where it makes the most sense, rather than forcing one material to carry the whole building.
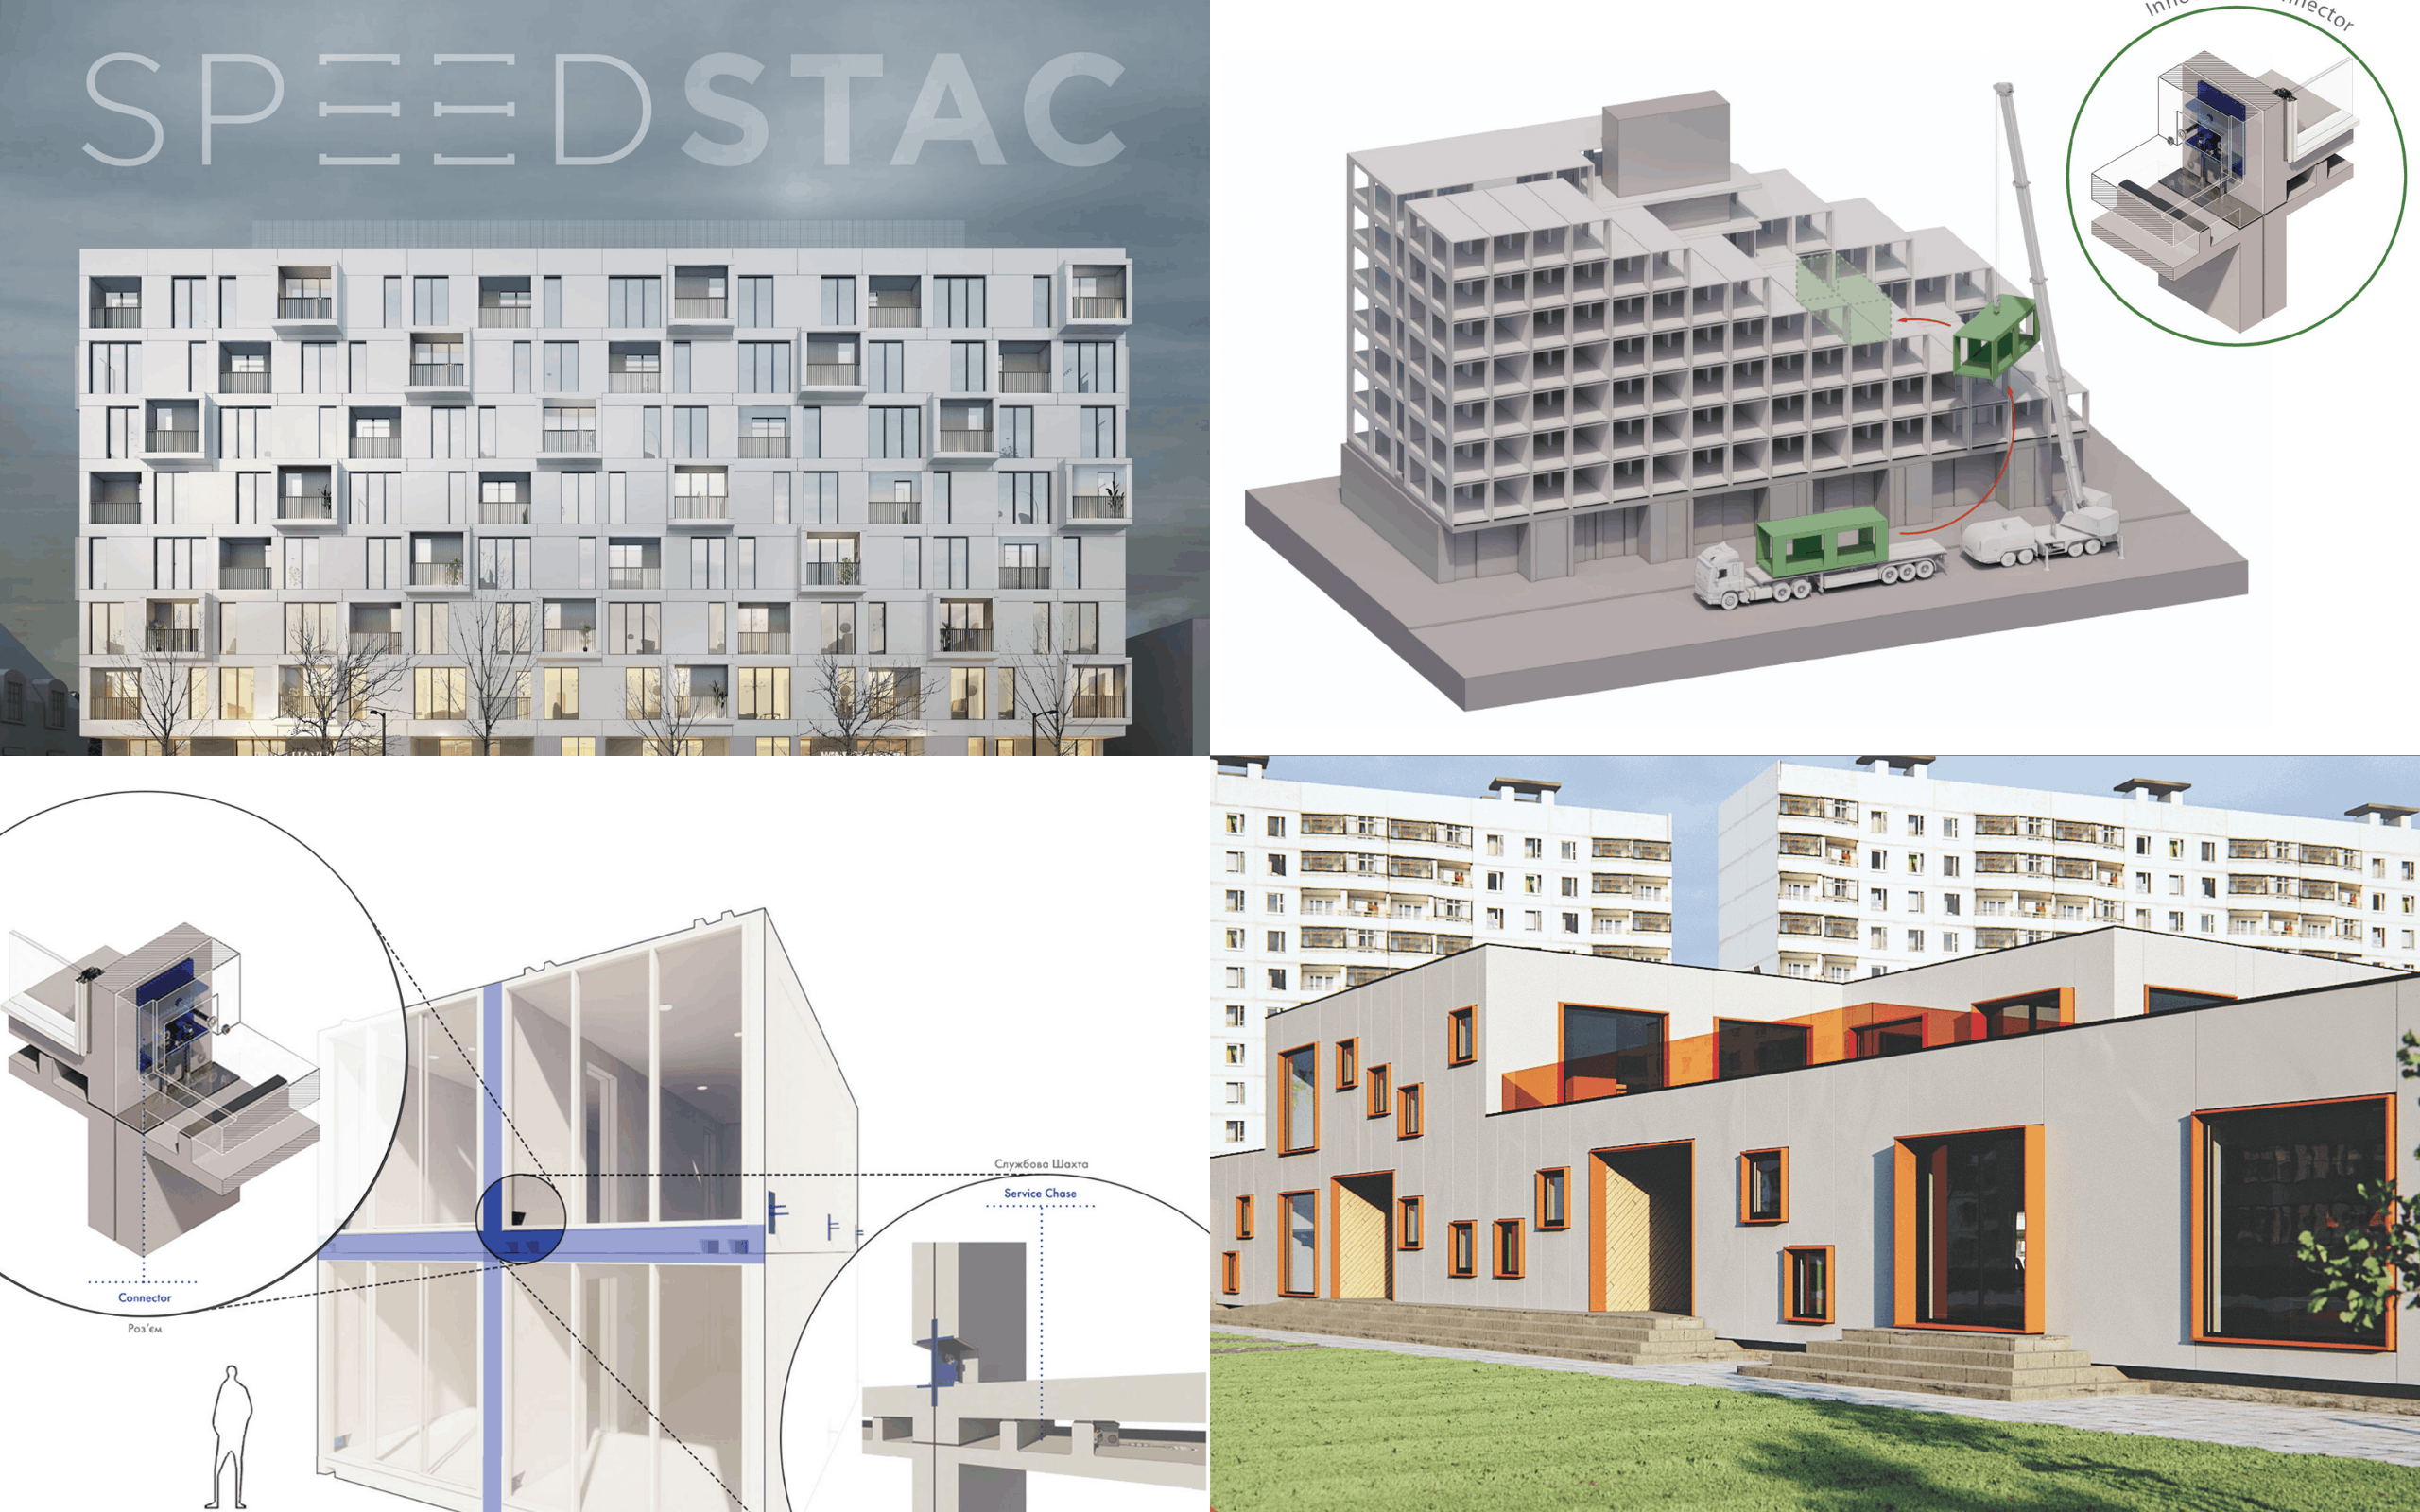
Speedstac is a modular building block system with built-in electrical and plumbing, designed to slide into damaged buildings by crane and replace destroyed sections without demolishing the whole structure. It started as a North American housing solution and pivoted to Ukraine after the 2022 invasion. The dimensions of Soviet-era apartment blocks turned out to match Speedstac modules almost exactly. WZMH won the Architect's Award at the 2023 Rebuild Ukraine competition, sponsored alongside Autodesk and Kingspan, designing 200 residential units for Kharkiv's north Saltivka district. A Speedstac kindergarten concept goes up in 10 working days. The system has both concrete and mass timber versions.
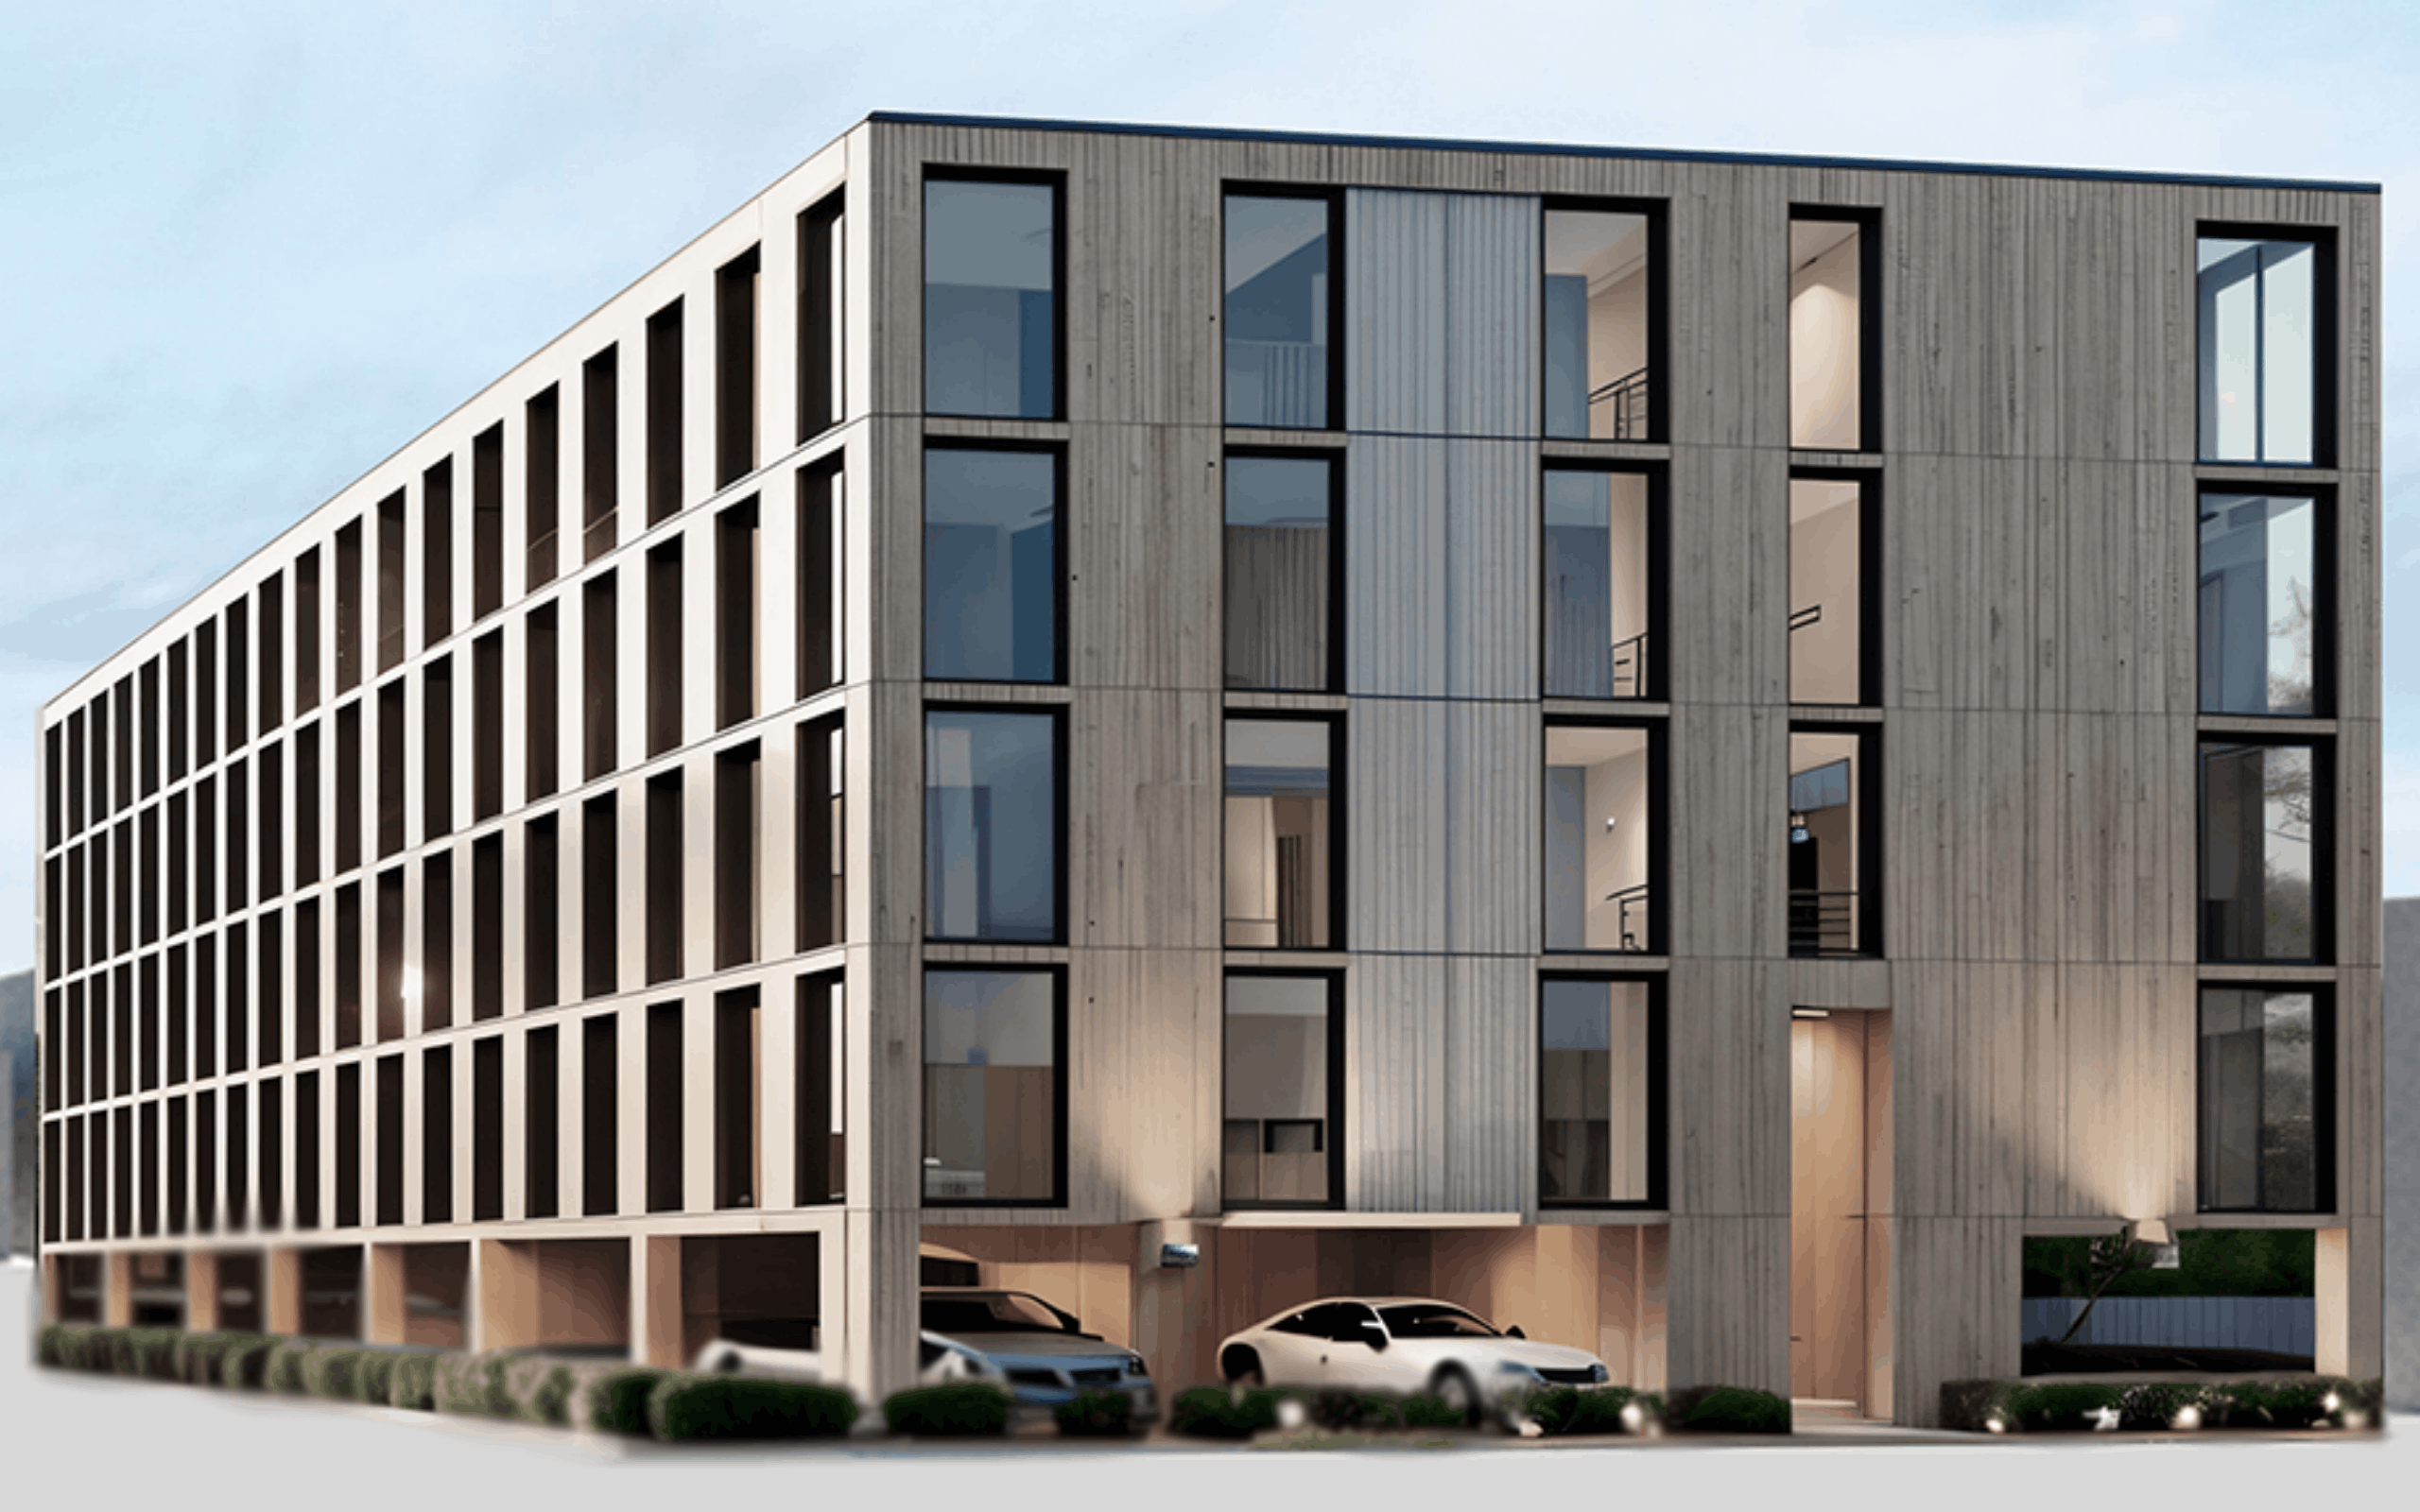
ELEVATE is the housing model. Build rental apartments on stilts over under-used community sites, decentralize the mechanical room into in-suite utility closets, and structure the deal so the host institution gets a revenue stream instead of selling land.
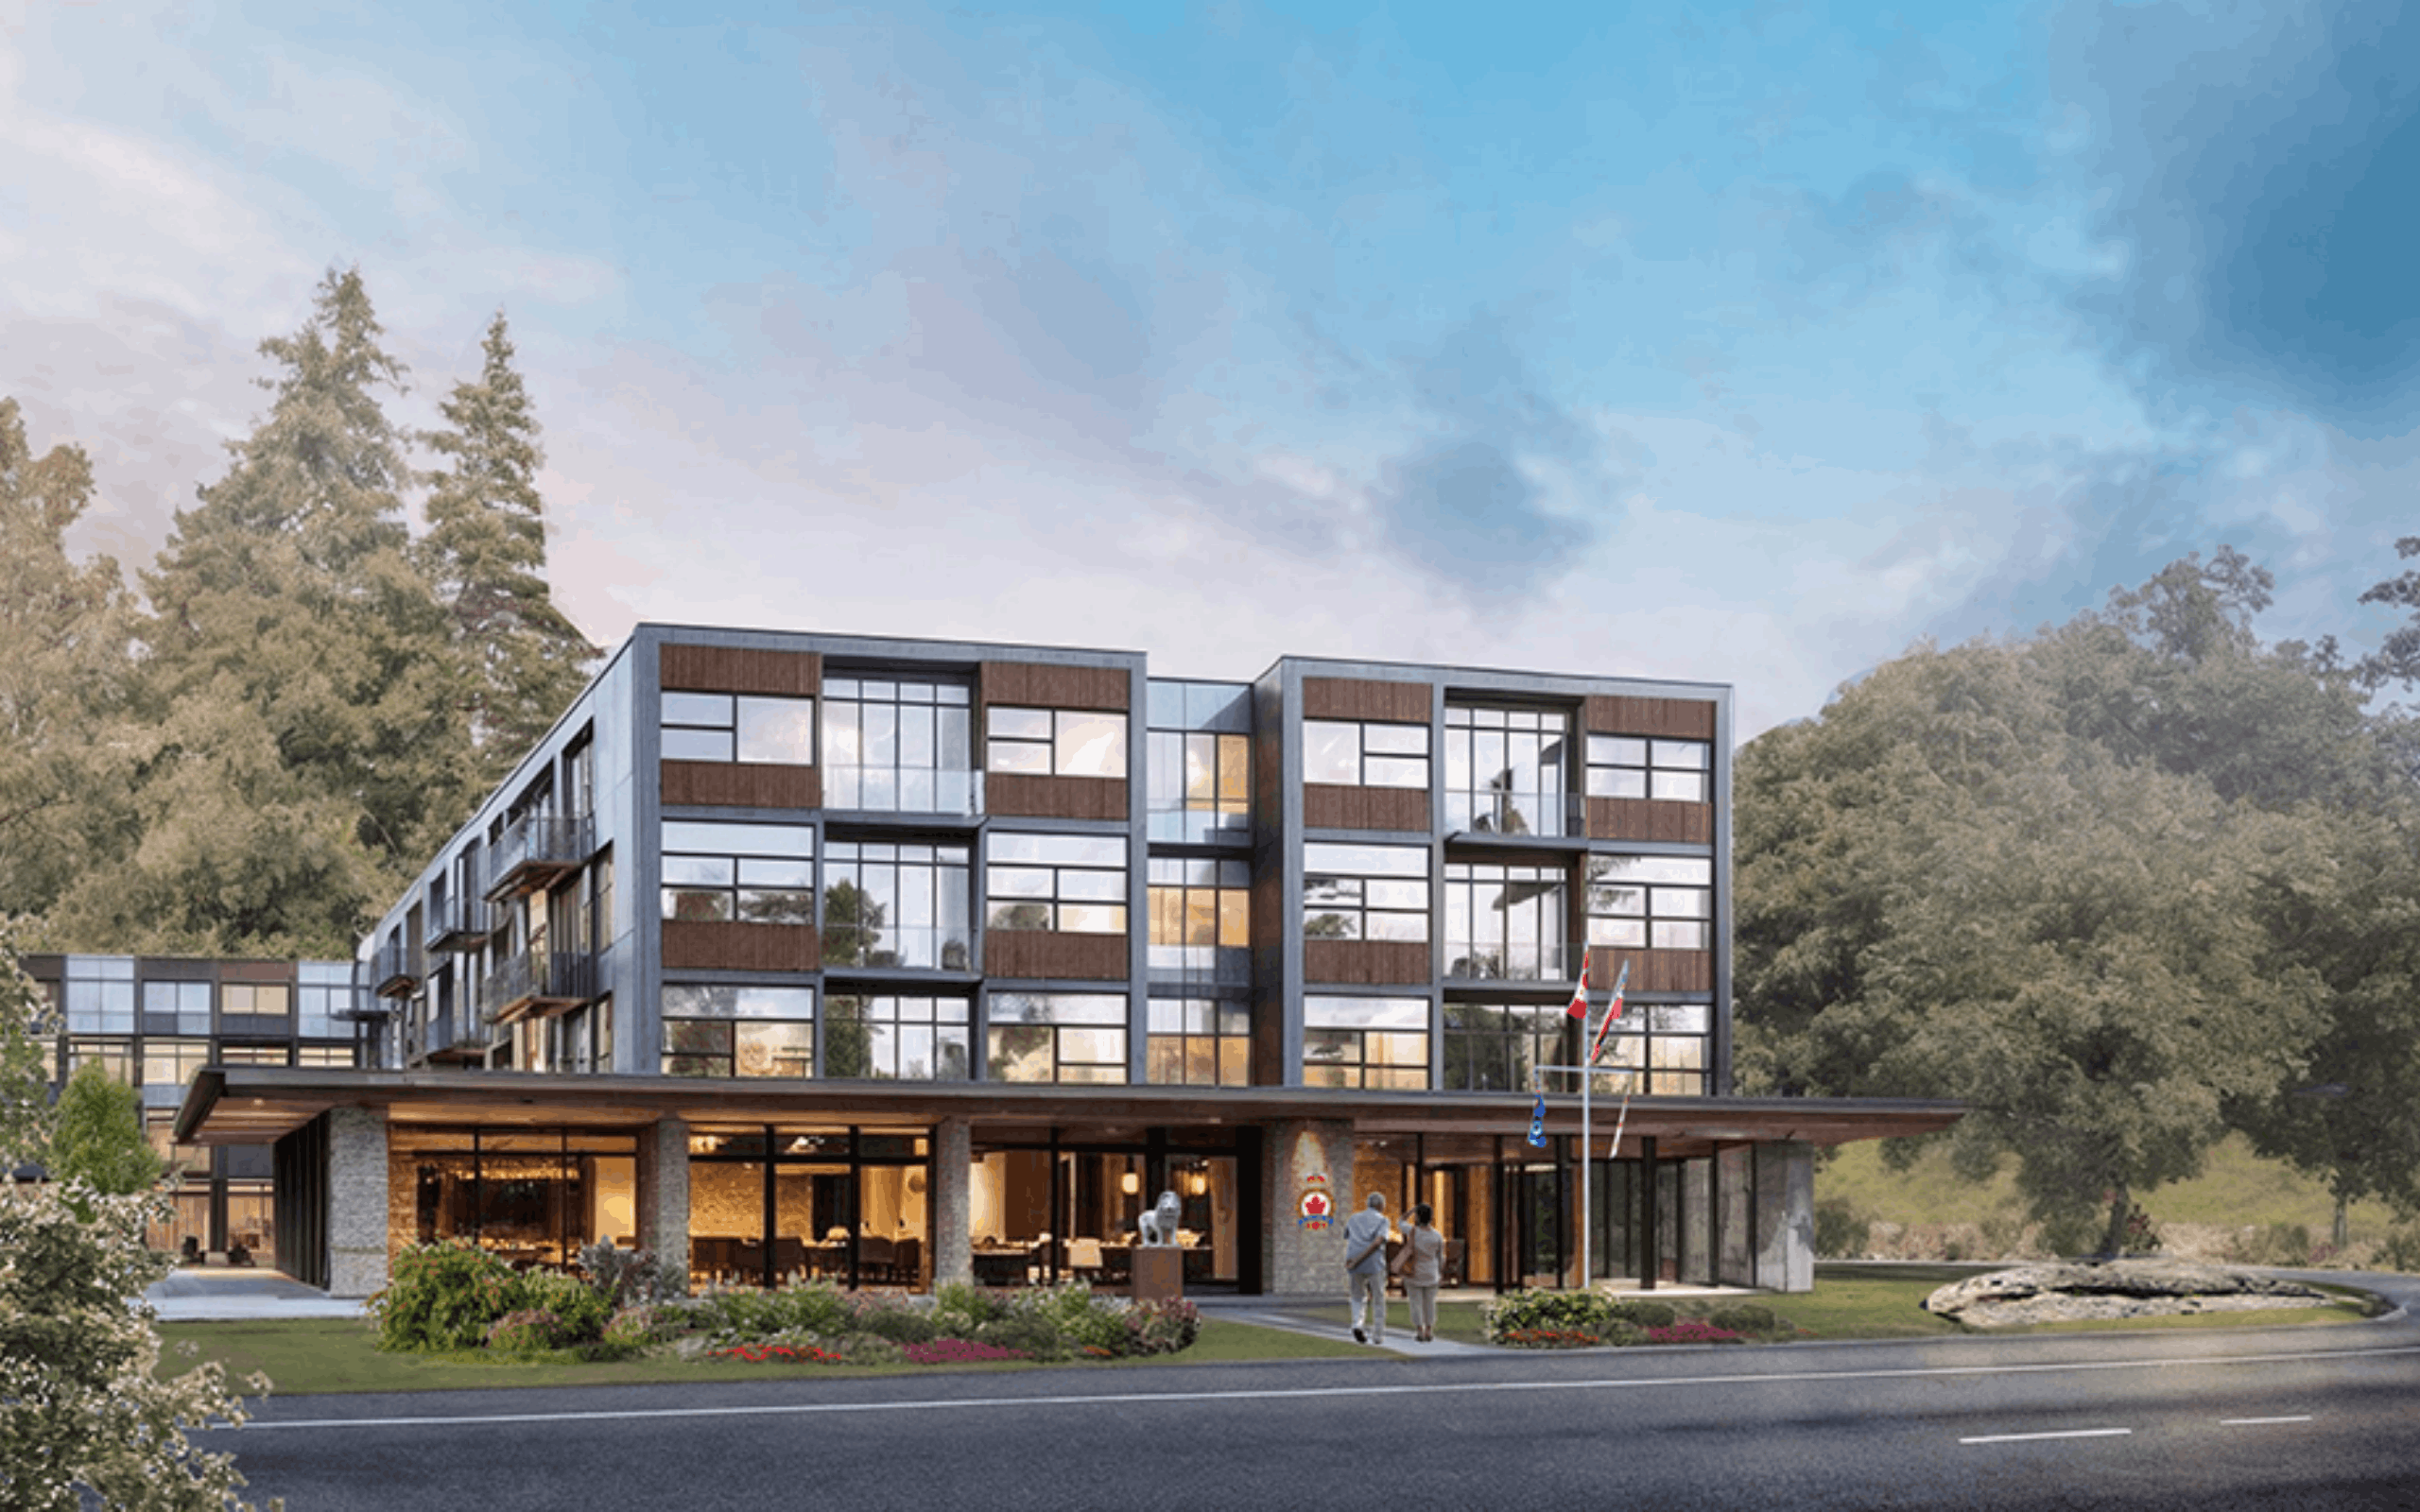
The first live project is in Bala, Ontario, where WZMH is replacing a 1970s Royal Canadian Legion hall with a larger legion facility on the ground floor and apartments above. The legion's signature semi-circle red brick bar will be dismantled and reinstalled in the new building. Demolition is targeted for May 2026. The same platform has been proposed for Toronto library sites.
None of those came from a strategic plan. They came from a team that was given permission to follow what looked interesting. The output is what happens when you keep that permission slip valid for a few years.
If a lab is just a permission slip, the question becomes: what does giving that permission actually do for the firm?
What Running a Lab Actually Does for the Firm
The easy answer is that the lab produces ideas, and some of those ideas turn into products. That's true, but it's the smallest part of what sparkbird has done for WZMH.
The bigger benefits show up in the day-to-day business.
The first is talent. People want to work somewhere that's doing exciting things. In a market where every firm is fighting for the same hires, it’s a real recruiting advantage. New staff gravitate towards the opportunity to invent and explore alongside their more traditional architectural work.
The second is competitive positioning. When WZMH competes for a project against other firms, they’re all showing up with similar portfolios, similar past projects, and similar people. Nobody's resume is really winning the interview. Zenon says sparkbird is what differentiates them.
“We could spend business development dollars on taking clients golfing and for dinners. Or we could spend that money in the lab here. Honestly, the results we're getting for spending the money in the lab are way better.”
The lab is the signal that the firm thinks differently, which is what clients hire firms for in the first place. The lab doesn't even have to be working on the client's specific project. The fact that the firm is the kind of firm that runs one says enough.
The third benefit is the longest to materialize and the hardest to measure. It's a different way of thinking. Teams that have spent time prototyping in the lab bring a different mindset back to their day-to-day work. They're more willing to question why something gets detailed a certain way, more comfortable proposing an unfamiliar assembly, more curious about what's actually possible.
The bet isn't on any single product. The bet is on what the lab does for the firm over time. Talent, positioning, mindset, and occasionally a real product that changes how something gets built.
If a lab does all that for one firm, the obvious question is what the industry would look like if a lot more firms ran one.
What If More Firms Did This?
Construction is one of the only major industries that hasn't fundamentally changed in a hundred years. Manufacturing has. Healthcare has. Aerospace has. The list of industries that have made big productivity leaps in the last fifty years is long. Construction isn’t on it.
There's no shortage of explanation for that. Fragmented supply chains, slow code cycles, project-based risk, conservative clients, thin margins. All real. But there's also an explanation that doesn't get said out loud often enough: most of the people designing buildings don't see inventing the parts - as part of their job.
Manufacturers are running businesses that depend on selling things they've already figured out how to make. The economic incentive for radical change sits with whoever is willing to spend time and money on something that might not work. And historically, that's been a small number of researchers in universities, an even smaller number of firms with their own labs, or the occasional tinkerer trying to make something better.
If a hundred more firms ran labs, even modest ones, that changes. Hundreds more people experimenting with hybrid assemblies, alternative materials, new connections, smarter mechanical layouts. Most of those experiments wouldn't go anywhere. But a few would.
A network of firms running labs, sharing what works, handing things off to producers who can ship them, moves things a lot. Mass timber in particular is the kind of category that would benefit from this. The product set is still relatively small. The supply chain is still developing. The cost curve is still figuring itself out. Every additional firm pushing on what mass timber can do, structurally and economically, accelerates how fast it becomes a default option instead of an alternative one.
The choice in front of most firms isn't whether to build a sparkbird or not. It's whether to keep treating innovation as something that happens somewhere else. The ones who’ve embraced the inventor mentality are already shaping what mass timber gets to be next.
If you're exploring mass timber for your own projects, one of the first questions is often: who actually makes the materials?
To help with that, we created a Mass Timber Producer Map featuring 39 North American producers and fabricators. You can explore manufacturers near your project, see the products they produce, visit their websites, and connect directly with them.
👉 Get access to the Mass Timber Producer Map by joining our newsletter!
Getting the Full Mass Timber Look Without the Price w/ Mike Lipke of Torzo Surfaces
Hybrid mass timber is often the smarter structural choice. But it comes with a trade-off most teams just accept. The exposed steel beam. The run of ductwork overhead. A finished building that doesn't quite look like the one in the renderings. You wanted all wood. You got wood plus everything you had to leave showing.
Mike Lipke has spent over a decade making sure you don't have to accept that. He's the president and owner of TorZo Surfaces, the only U.S. manufacturer of Thin CLT panels. Thin sheets of cross laminated timber, available in almost any species, made from new material or remanufactured scrap. He's been making them since 2011, well before most people in the U.S. had heard of CLT.
In this piece Mike breaks down what Thin CLT actually is, the problems it solves on a jobsite, how it gets made from both new wood and salvaged material, and what the demand for it says about where mass timber is headed.
This article is just one part of the newsletter where we cover who and what’s shaping the mass timber industry.
👉 Stay ahead of the mass timber industry & grow your network. Join Our Newsletter
What Thin CLT Is and What It Solves
Thin CLT is a 4x8’ cross laminated timber panel ¾” thick (standard, they can make custom sizes too). It's designed that way to be familiar with crews used to working in standard plywood and OSB dimensions.
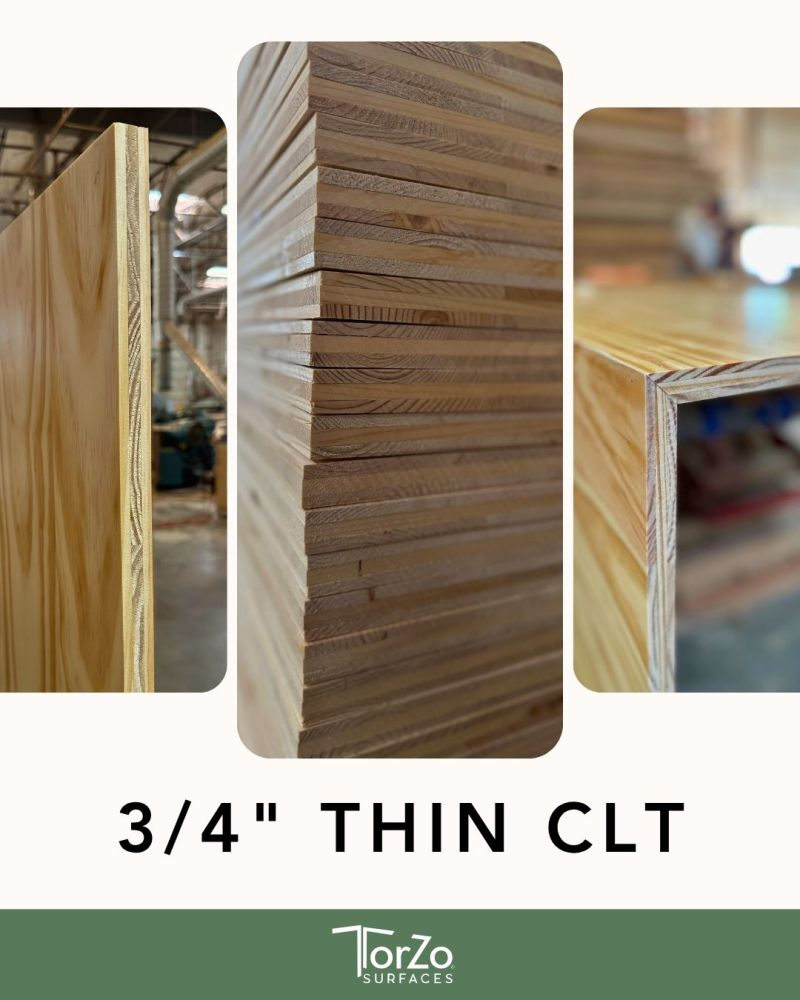
Most of the time, the job is cladding. In a mass timber building, that usually means covering up something that isn't wood. A steel beam. Concrete. Mechanical and HVAC ducting. You wrap it in a panel so it looks like mass timber. Most commonly, Mike sees it used as a beam wrap.
A lot of mass timber buildings put a steel beam in here and there, and the team wants it gone. Covered. Looking like the rest of the wood. Normally, that means using a different wood product (and mismatched look), or a full-sized mass timber piece that comes with a bigger price tag. But, with Thin CLT, you don't need the full-sized panel to maintain the consistent aesthetic.
On a big field nobody sees the edge of a panel in the middle of that wall, nor is it carrying any sizable load. There's no reason to pay for the structurally sized members there.
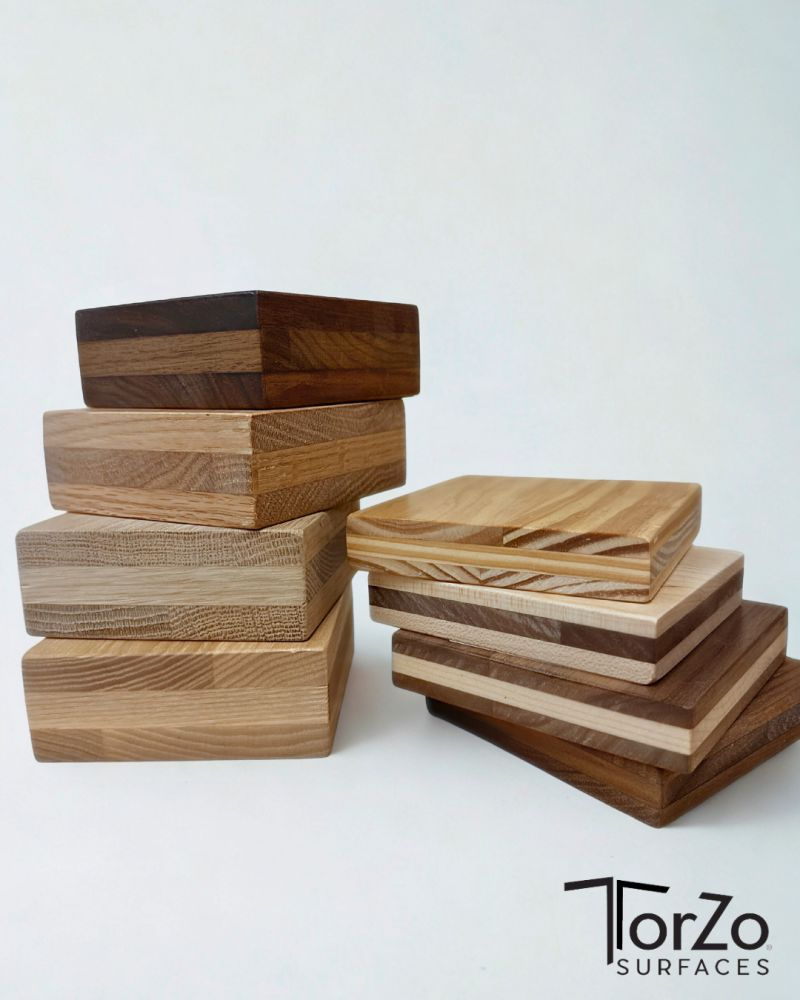
Instead, Mike laminates the exact same species, grade and finished material onto a cheaper backer, getting the exact same look, and saving the money. The whole wall looks like the same CLT construction as the main structure, even when most of it isn't.
How It's Made: New Wood and Salvaged Scrap
The new-wood process starts with standard dimension lumber. Two by fours, two by sixes, any species. Torzo re-saws it into thin layers, glues the strips into sheets, then laminates the sheets together in a normal 3-layer CLT pattern to make the panel.
You might be thinking, why not just use a single layer of the face material? In a perfect world, or with a perfect material, that would work. The problem is that wood isn’t perfect.
It moves. It drys. Bends. Warps. And twists. And then, no 2 pieces are alike. They do all that in different ways, times, and cycles. Using just the face material in a single layer would give you a very unstable material. Using multiple layers and putting the more “spirited” pieces in the middle stabilizes and distributes all that action across the panel and keeps it stable.
So when you want a “clear” panel look (no knots, checks, decolorization) you can get a perfectly clear face while the knottier material goes inside (the middle) where nobody sees it. The face (and/or the back) match what the customer wants. And nothing gets wasted.

AEC Convention
This is THE mass timber event where new projects get started, deals happen, and you grow your network (ask anybody who comes).
Next year, we'll have dedicated tracks for each AEC profession, and a series on developer conversations and priorities.