
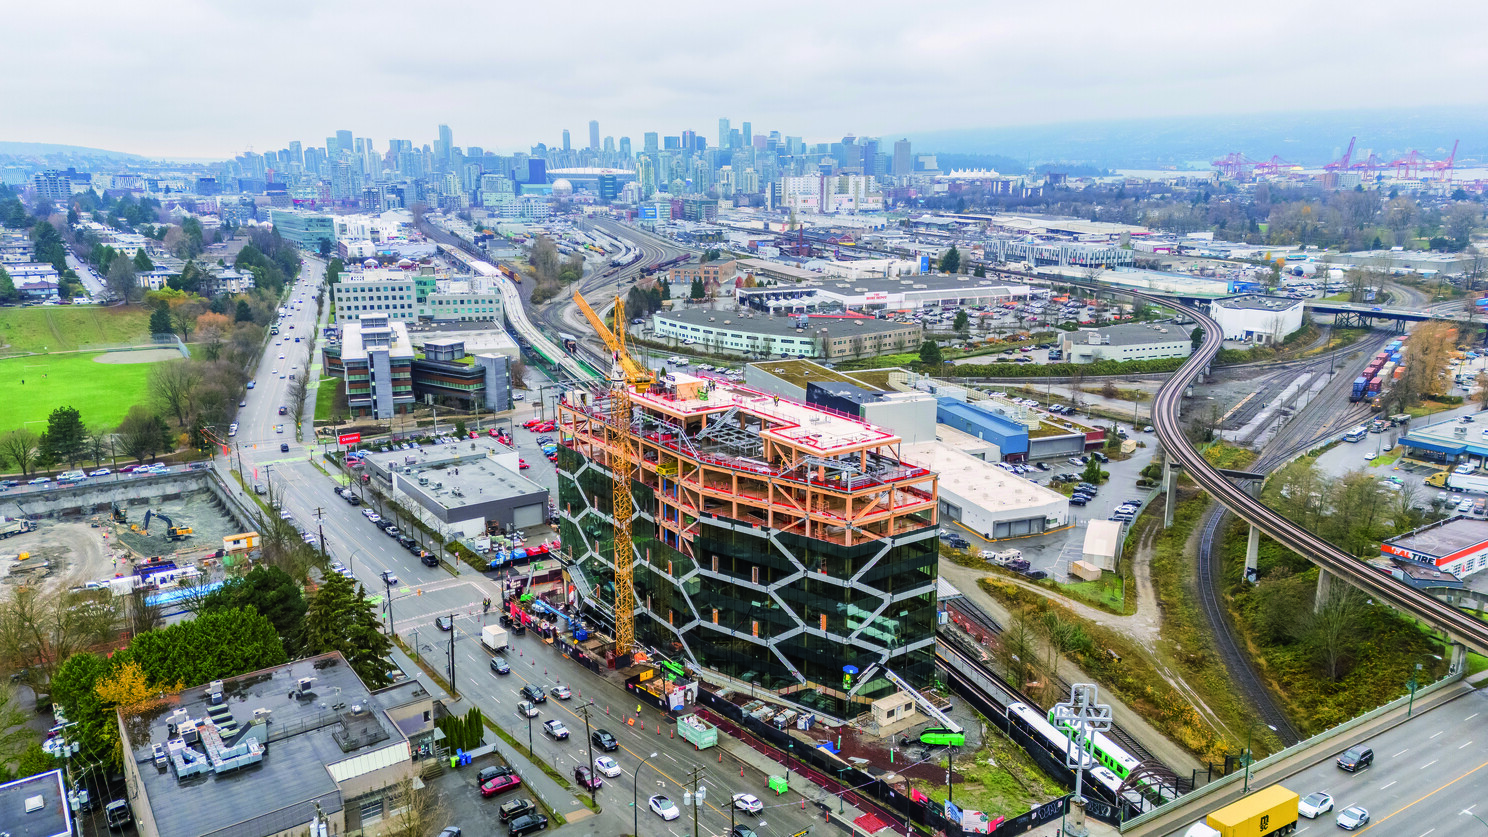
If you had asked a room of architects a decade ago whether a 10-story timber building could stand tall in a seismic hotspot, most would have dismissed the idea as fanciful—if not outright reckless. Yet today, Vancouver’s Hive rises as a striking counterpoint, its honeycomb exoskeleton and timber braced frame system challenging both convention and gravity. What changed? And how did a material once relegated to low-rise construction become the centerpiece of one of North America’s most ambitious urban projects?
For Ryan McClanaghan of DIALOG , the answer is as much about community as it is about engineering. “There’s something about this material and this way of thinking about a project that really captured my imagination,” he recalls of his early exposure to mass timber in Europe. That initial spark—fueled by open collaboration and a willingness to rethink the fundamentals—set him on a path from novice to innovator, culminating in a project that demonstrates what can happen when design, sustainability, and resilience converge.
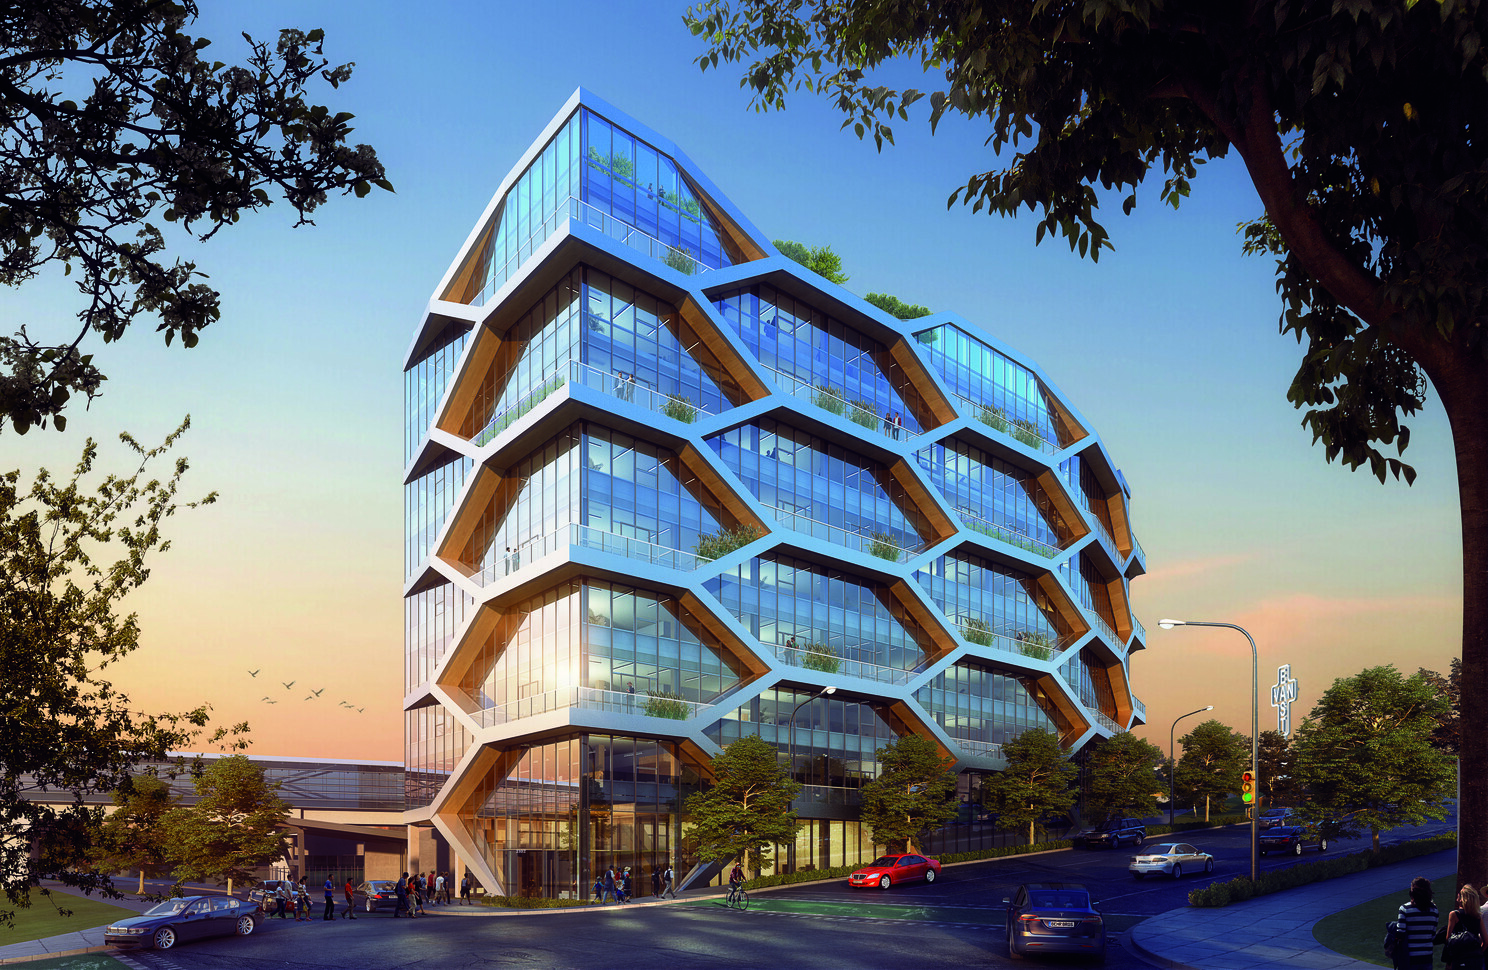
From Novice to Innovator: Ryan McClanaghan's Journey into Mass Timber
A single encounter with a new material can redirect an entire career. For Ryan McClanaghan, that moment arrived during his studies at the University of Toronto, where early exposure to mass timber set the stage for a transformative path. His formative work term in Berlin, immersed in the European timber scene, catalyzed a fascination that would later position him as a leader in North American mass timber design with The Hive.
“There’s something about this material and this way of thinking about a project that really captured my imagination.” Ryan’s early intrigue was fueled by witnessing projects like a mass timber office building in Helsinki—examples that demonstrated both the technical and cultural momentum of timber in Europe. Returning to Canada with Dialogue, his growing expertise soon converged with the opportunity to lead the design of The Hive.
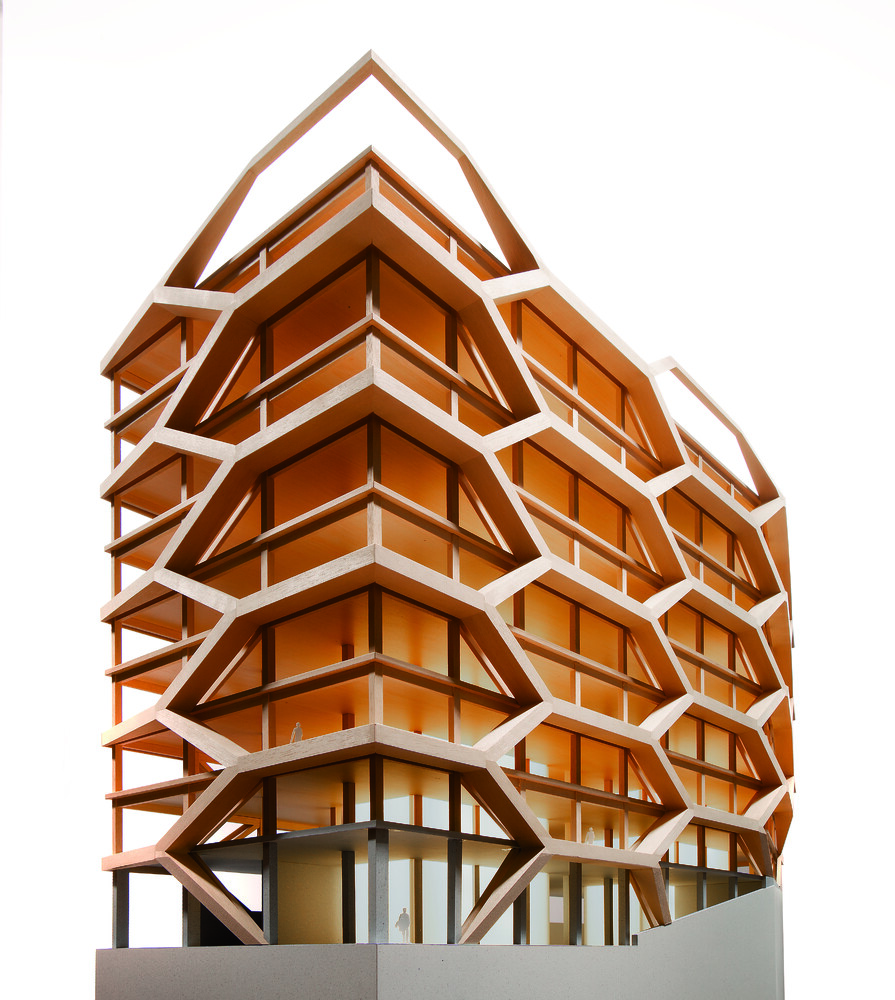
Rethinking Structure: The Hive’s Perimeter-Driven Timber System
Few North American projects have so thoroughly reimagined the structural logic of mass timber as The Hive. Rather than defaulting to a concrete core, the design team shifted the primary structural elements to the building’s perimeter, unlocking new architectural and engineering possibilities.
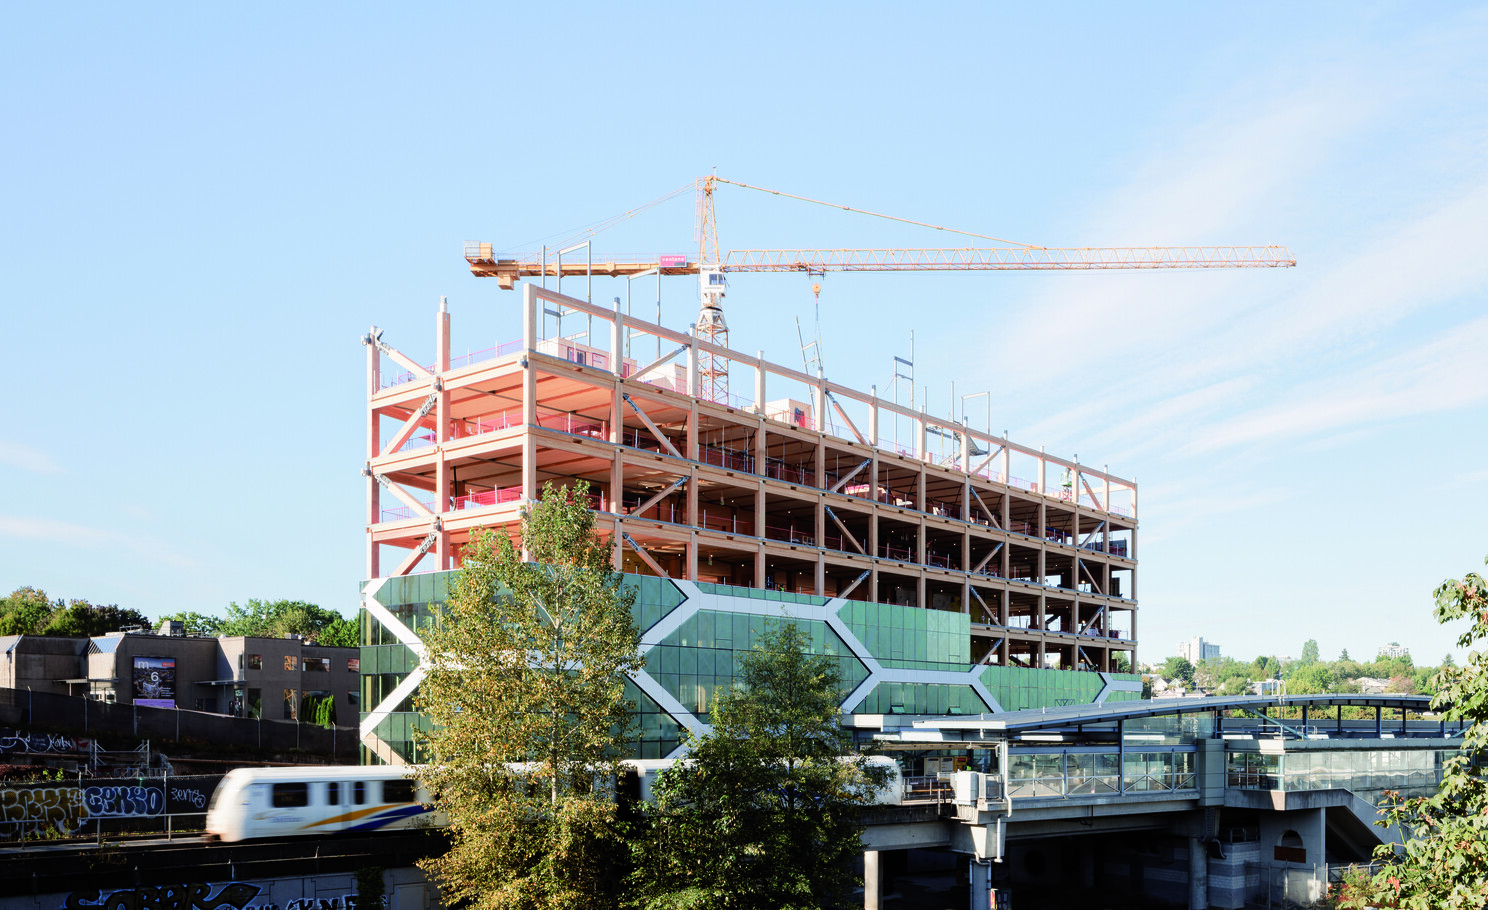
“What if we did an all-wood structure above L2?” This question reframed the project’s ambitions, resulting in a 10-story Vancouver building whose cellular exoskeleton and timber braced frame system serve both as expressive façade and as the backbone of its seismic resilience. The integration of timber shear walls and buckling restraint braces demonstrates how mass timber can perform at scale—not just as a material of warmth, but as a robust structural solution.
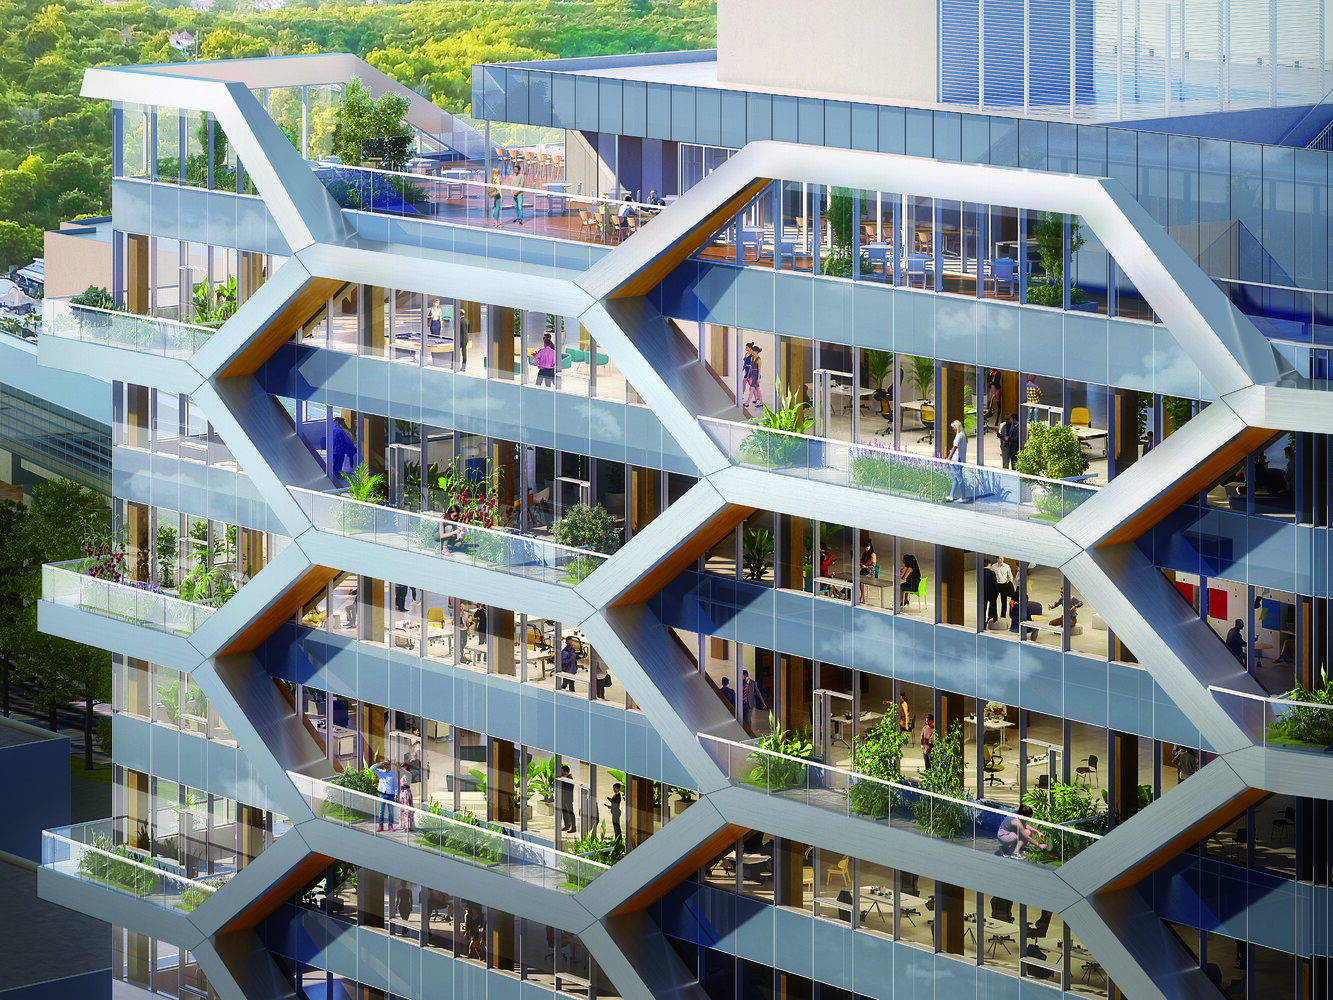
The Hive’s biophilic strategies—from cascading balconies to generous daylighting—are not mere aesthetic gestures. They are embedded in the building’s structural DNA, with the unique geometry of the façade channeling forces efficiently while fostering occupant well-being. As Ryan notes, “The unique geometry of the building facade carries the forces that act on it, creating a harmonious relationship between form and function.”
This perimeter-driven approach set the stage for the project’s next major challenge: seismic performance in a demanding context.
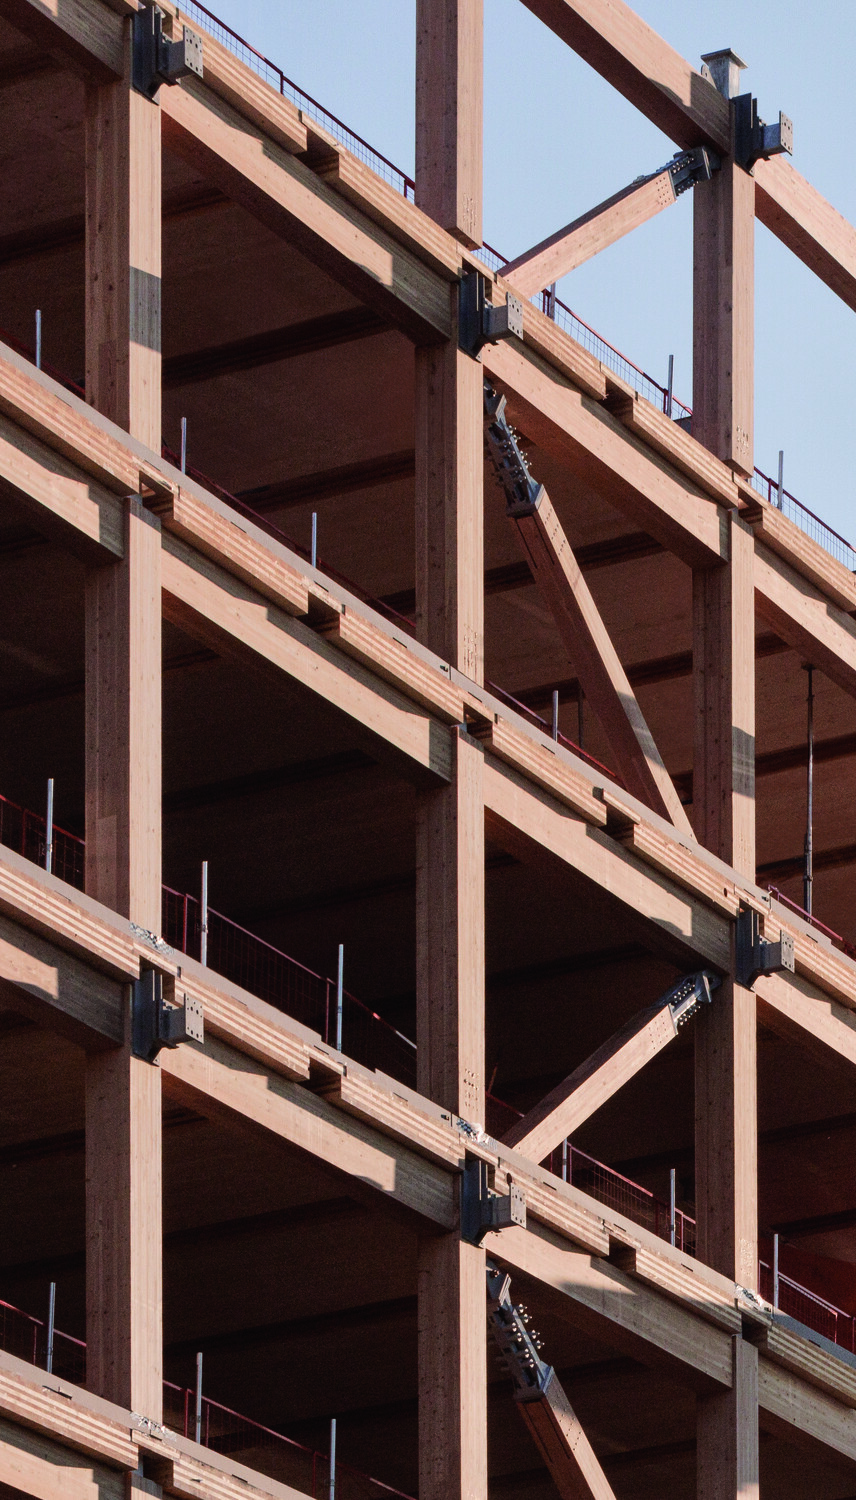
Navigating Seismic Challenges: Engineering Resilience
Vancouver’s seismic profile demands more than conventional solutions, especially for mass timber structures. The Hive’s design team confronted this directly, seeking to minimize concrete use while meeting stringent performance criteria.
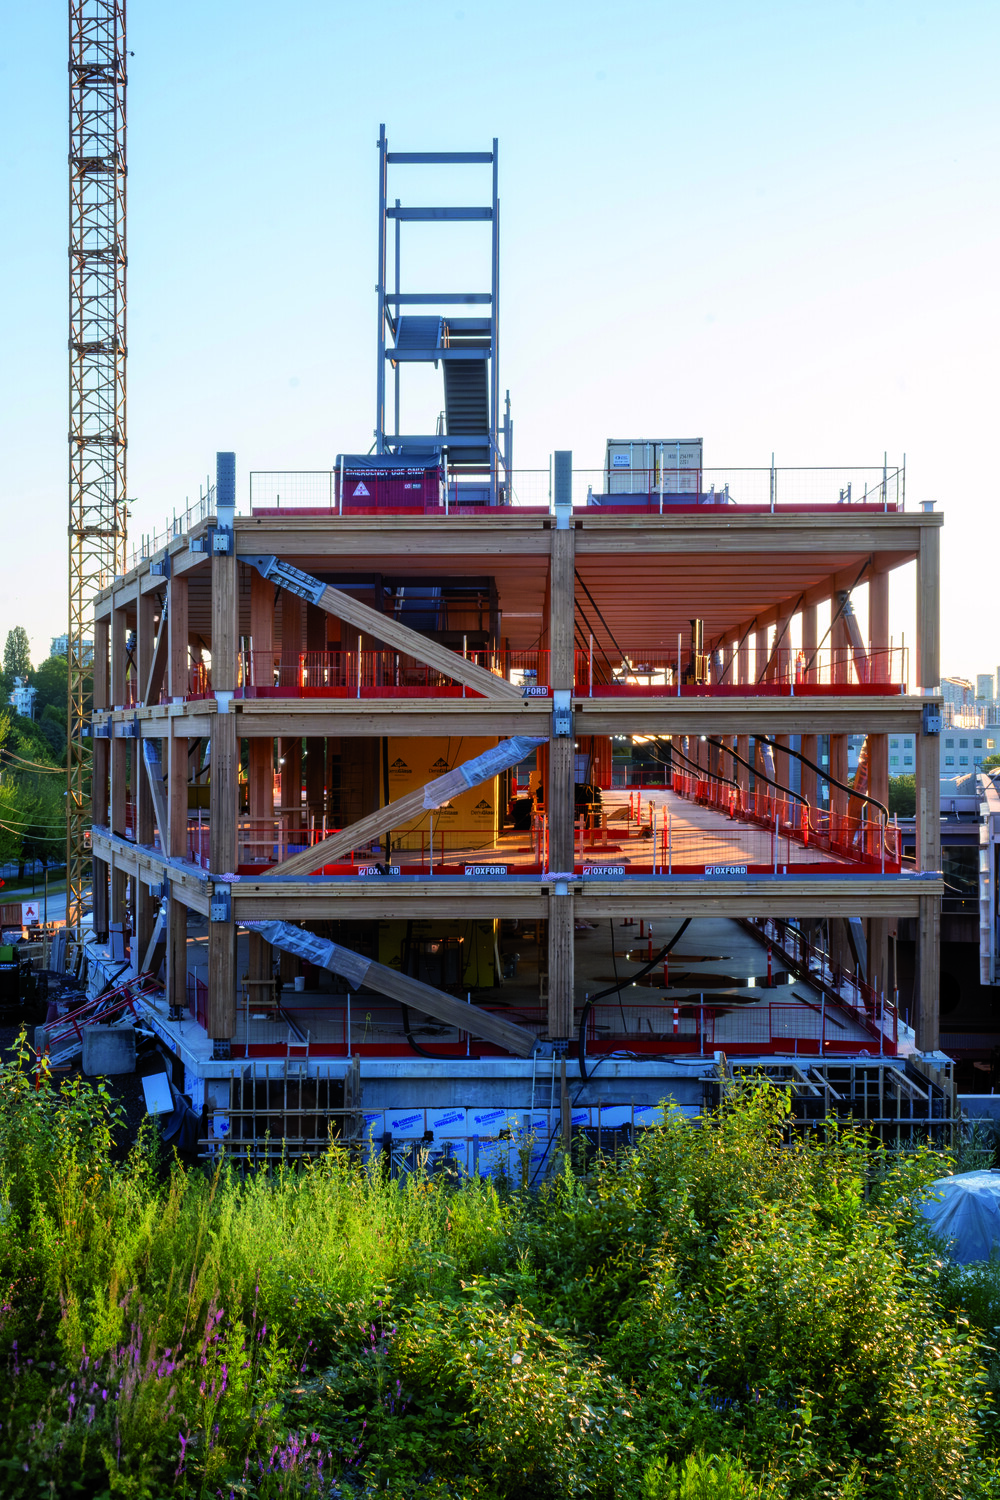
“We only wanted to use concrete as much as we needed to get out of the ground.” This guiding principle led to a predominantly timber superstructure above the second level. The team’s close collaboration with structural engineers yielded a lateral system built around timber buckling restraint braces—an approach that satisfied seismic codes and reinforced the building’s architectural identity.
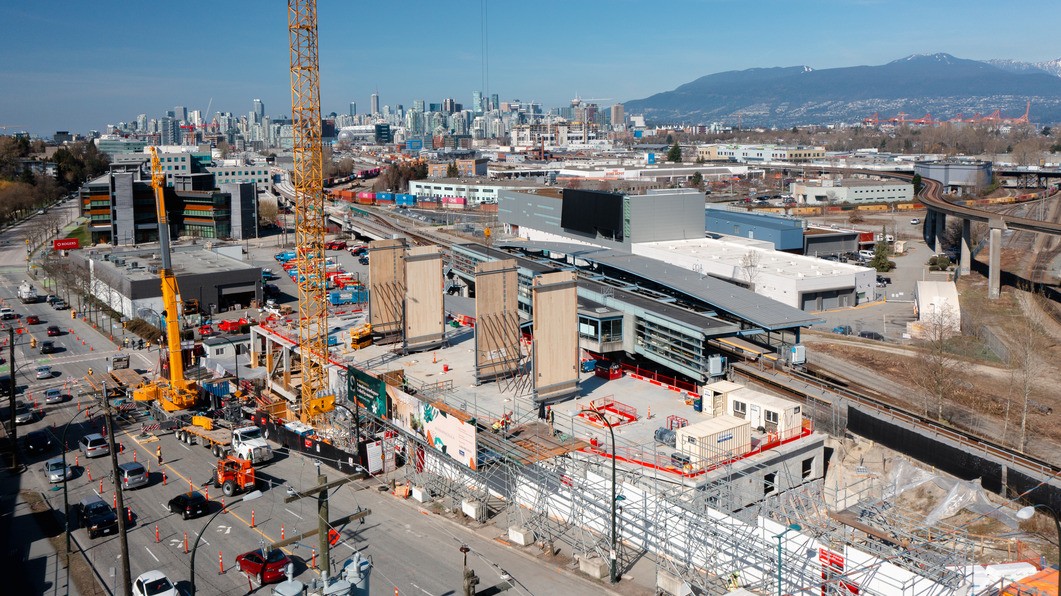
“We are well above what the performance needs to be,” Ryan explains, underscoring the project’s commitment to both safety and technical rigor. The integration of seismic resilience into the building’s visual language exemplifies how engineering and design ambition can reinforce one another.
The complexity of these challenges required a project culture built on trust and shared expertise—a theme that would define the next phase of The Hive’s development.
Collaboration: The Heart of Successful Mass Timber Projects
When technical ambition meets construction reality, the difference between success and failure often lies in the quality of collaboration. The Hive’s progress depended on a tightly integrated team of architects, engineers, and builders, each contributing specialized knowledge to solve unprecedented problems.
“Teams make projects go,” Ryan emphasizes, reflecting on the necessity of open communication and mutual respect. The project’s unique features—perimeter bracing, exposed timber, and complex connections—demanded iterative problem-solving and a willingness to adapt as new challenges emerged.
“How you solve problems together collaboratively is important,” he notes, highlighting the value of collective intelligence over individual heroics. This ethos extended beyond the core team, as Ryan actively sought input from peers across the industry, reinforcing a culture where knowledge-sharing accelerates progress.
The collaborative momentum built on The Hive would soon propel Ryan into a broader network of mass timber innovators, both locally and abroad.
Learning from the Best: A Journey of Knowledge and Networking
Access to global expertise can accelerate innovation far beyond what’s possible in isolation. Ryan’s deliberate outreach to leaders in mass timber—through site visits, conferences, and direct conversations—provided a foundation of technical insight and professional relationships that shaped his approach to The Hive and beyond.
“I was amazed by the number of doors that opened, the people I met, and the meaningful connections I made.” These experiences not only expanded his technical repertoire but also embedded him in a community where ideas and lessons circulate freely. Ryan encourages peers to seek out these opportunities: “If you can do it, get out in the world and visit some timber projects.”
By immersing himself in the international mass timber community, Ryan gained a nuanced understanding of both the material’s potential and its limitations—knowledge that would inform his approach to hybrid systems and sustainability.
The Future of Mass Timber: Hybrid Approaches and Sustainability
As mass timber matures, the conversation is shifting from material purity to strategic integration. The next frontier lies in hybrid systems that combine timber, concrete, and steel, each deployed where it performs best.
“We love timber and we want to use it in the right places and as much as possible.” This pragmatic philosophy underpins projects like the 19-story hybrid mass timber tower now underway in Vancouver, where timber’s strengths are complemented by other materials to achieve both performance and cost targets.
The adoption of life cycle analysis (LCA) as a design tool—not just a reporting requirement—enables teams to make evidence-based decisions about material selection and environmental impact. “I’m excited about this LCA process not as reporting but as a design tool to make good choices along the way,” Ryan explains, pointing to a future where sustainability is embedded in the earliest design moves, not appended at the end.
This evolution in practice is inseparable from the networks and communities that sustain it—a point Ryan returns to as he considers the broader movement.
Building Momentum: Community, Knowledge, and the Next Chapter
The rapid advancement of mass timber is not the result of isolated breakthroughs, but of a growing community committed to rigorous exchange and shared ambition. Ryan’s experience demonstrates that the most significant progress occurs when expertise is pooled and lessons are openly shared.
“If you’re curious about it, if you’re interested, you’re asking good questions. People love to talk about what they’re up to,” he observes, underscoring the accessibility of the mass timber community to those willing to engage.
As the industry moves toward more complex hybrid systems and deeper sustainability metrics, the need for robust professional networks and transparent dialogue will only intensify. The future of mass timber will be shaped not just by technical innovation, but by the willingness of practitioners to collaborate across disciplines and geographies.
In the end, The Hive stands as a case study in how seismic innovation, collaborative culture, and a commitment to sustainable hybrid systems can converge in a single project. The real measure of progress lies not in isolated achievements, but in the capacity of the field to continually integrate new knowledge, challenge assumptions, and build structures—and communities—that endure.
Frequently Asked Questions
How did The Hive’s structural system differ from typical North American mass timber projects? The Hive moved primary structural elements to the building’s perimeter, using a cellular exoskeleton and timber braced frame system rather than a conventional concrete core.
What strategies were used to address Vancouver’s seismic requirements with minimal concrete? The design team created a predominantly timber superstructure above level two, incorporating timber buckling restraint braces and shear walls to meet and exceed seismic performance standards.
How did collaboration influence the project’s technical and construction outcomes? A tightly integrated team of architects, engineers, and builders engaged in open communication and iterative problem-solving, enabling solutions to unique challenges like perimeter bracing and complex connections.
What role did international knowledge exchange play in shaping The Hive’s design approach? Ryan McClanaghan’s outreach to European mass timber experts through site visits and direct conversations provided technical insights and professional relationships that informed the project’s structural strategies and hybrid system integration.
How is sustainability addressed in The Hive and subsequent projects?The team uses life cycle analysis (LCA) as a design tool to guide material selection and environmental impact, and embraces hybrid systems that combine timber, concrete, and steel to optimize both performance and sustainability.

Tired of Mass Timber Challenges Derailing Your Projects? Learn How to De-Risk & Deliver Them.
Lead mass timber projects with confidence — and leave delays, redesigns, and budget blowups behind.
✅ Solve early-stage design, sourcing, insurance, permitting, code & cost hurdles before they derail your project.
✅ Find technical answers on design, detailing, procurement, embodied carbon ROI, hybrid systems & more.
✅ Build relationships with developers, GCs, architects, and engineers shaping mass timber’s future.
Get your ticket— and get the insights, skills, and network to deliver mass timber projects successfully.

Latest episodes
Mass Timber Moisture: Where Risk Hides & How to Manage It w/Jason Teetaert of SMT Research
CLT is going to get wet at some point. The real questions are how wet, for how long, and whether anyone will know when it happens.
Jason Teetaert is the co-founder and president of SMT Research Ltd. in Vancouver. SMT monitors moisture inside walls, roofs, and structure, and has been installing roof leak detection in mass timber buildings since about 2011.
Below, Jason covers how to tell when CLT is too wet, how to protect panels before they ship, where to put sensors, how to catch roof damage during construction, and why mold is a risk owners carry on their own.
This article is just one part of the newsletter where we cover who and what's shaping the mass timber industry.
👉 Stay ahead of the mass timber industry & grow your network. Join Our Newsletter
When Is CLT Too Wet? The 25% Moisture Content Threshold
If the surface of a CLT panel reads 25% moisture content for seven days, there's probably moisture at the core.
What happens next depends on where you're building. In the Pacific Northwest or the stormy Southeast, a panel past that line will likely need active drying, because it won't dry out on its own. In drier climates, you might get away with it.
Plan the schedule around that line. Some contractors start the CLT install at the beginning of the dry season and try to close in the cladding by the end of summer. Jason thinks that works on smaller floor plates and gets really difficult on larger ones. On the most successful projects he's seen, the facades and roof were finished within days of the primary structure. That won't fit every project, but it's the benchmark to aim for.
Hitting that line starts with knowing what's actually in your panels.
Protecting CLT Panels From Moisture Before They Ship
The CLT samples manufacturers send to researchers are perfect. The boards are square, the glue line is clean, and the panel is pressed tight. What shows up on site is often made with slightly different lumber that has more wane, and with air gaps that can run all the way through the panel.
For structure, those gaps make very little difference. Same for fire. For moisture, they're an open path in. Example below.
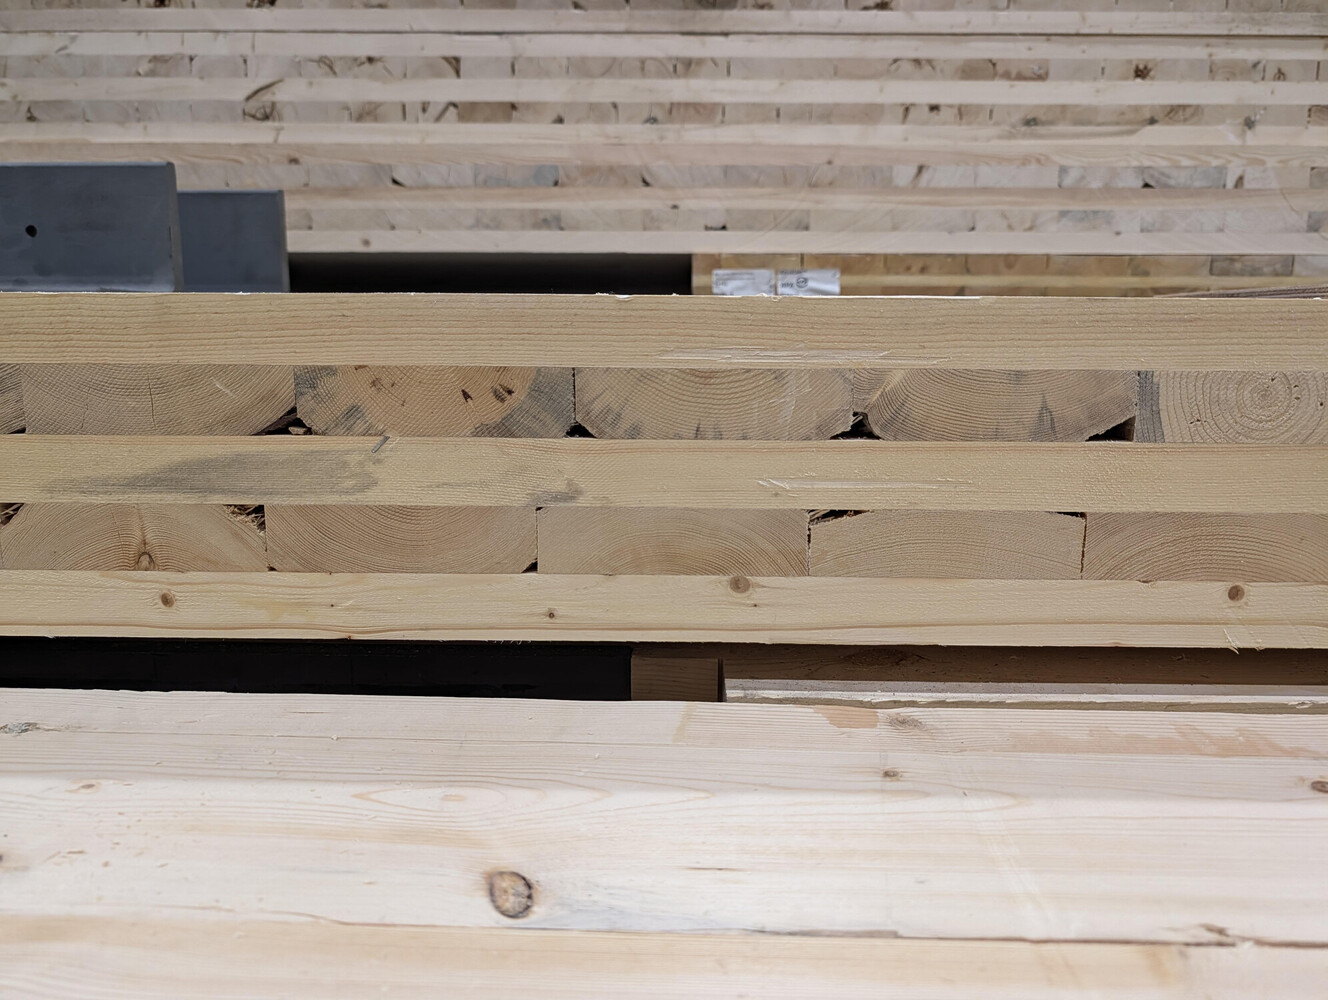
So if you're the designer or the owner, get the CLT covered in the factory. That's Jason's first move on any CLT building. Spec a moisture barrier or sheet good and an edge treatment before the panels ship. There are too many variables in transportation, installation, and commissioning. One delay plus one rain event and the panel is wet.
Teams don't need to start this from scratch. Research comparing protection methods like sheet goods, coatings, and wax was done about 10 years ago and is out there to find. Some new all-natural products are coming to market too.
Even covered panels need someone watching them, and that's where sensors come in.
Where to Install Moisture Sensors in Mass Timber Buildings
Installing sensors isn't a big lift. "It's literally drilling two holes, pushing in the probes and then hooking it up to a data acquisition system." The hard part is deciding where they go.
Start with the spots you can't easily fix later:
- Big glulam joints
- Areas that can't get waterproofing right away
- Structurally attached wood eyebrows, especially where wood replaced steel to save time or embodied carbon
- Anything under heavy overburden, like planters, pavers, and amenity spaces
- Drains, doorways, and plumbing risers on the roof
- Bathrooms and showers on the floor below
Jason's team used that checklist on a six-story rental housing project with an amenity roof garden. They put a sensor in every CLT panel and added more at every one of those risk points.
If he were building for himself, he'd install sensors in the factory. He'd measure moisture content and temperature at minimum and leave the sensors in for the life of the building. Panels can change hands two or three times before they're erected, and the data shows where along the way they got wet.
Already mid-build with wet panels? Sensors can be shipped to site and installed by your own crew at preselected spots, and the dashboards go live right away. That's more and more common. It beats handheld readings and an opinion. A graph showing what's wet and what's drying is what you need to decide on drying methods and cost.
The roof is where the most damage happens and where the fewest people notice.
Mass Timber Roof Leak Detection During Construction
Roofs go on early so the mass timber gets covered. Then, on tight urban or campus sites, the finished roof becomes the staging area and the damage starts.
The fix is monitoring from day one. SMT lays moisture detection tape on the air vapor retarder before the insulation and membrane go on. If the data shows the roof stayed dry through rain and then damage shows up on a specific day, the GC knows who was up there. Jason calls it "instant accountability."
GCs should look at this as protection for the whole team. Roofers and waterproofers often get stuck finding and repairing damage that other trades caused. You wouldn't ask a glazing contractor to replace a window a crane broke for free, so why them? Data lets you put the repair cost on the trade that caused the damage, right away. Wait two or three years, and that damage turns into a moisture intrusion mess nobody can trace.
That mess is also the part of the risk insurance won't help with.
Mass Timber Insurance, Mold, and Moisture Liability
Owners and developers should understand where moisture sits in the insurance picture:
- Construction: Jason says GCs are paying five to six times more for insurance than they did 10 years ago, especially on CLT. Moisture is a big part of why.
- Design: Errors and omissions reports show a disproportionate increase in claims against architects on their mass timber projects compared with their concrete and metal ones. The three drivers are acoustics, fire stopping, and moisture.
- Ownership: Fire, earthquake, flood, and pipe breaks are typically insurable. Mold isn't. Almost every major carrier has written it out of their policies. Mold usually comes from slow moisture that sits 30 days or more: enclosure and roofing deficiencies, window wall details, under shower pans. Owners are 100% liable for it.
That uninsured part is what owners can actually manage. Jason's answer is a moisture monitoring system plus regular maintenance and inspections. Monitoring also catches interior problems early. On one project, a mechanical room system kept sending alerts while the maintenance manager insisted there was no leak. An SMT technician followed a light trickle back to a leaking plumbing knuckle, weeks before it would've turned into a catastrophic loss.
Owners also don't have to fix every alert the same day. Some deal with issues right away, and some decide what can wait. Either way, they're making an informed choice. Schools, hospitals, universities, government, social housing, and rental owners get the most from it because they live with the building long term.
None of this sticks unless the people on site know it.
Moisture Management Training for Mass Timber Project Teams
Every mass timber project is a new mix of designers, GCs, and trades. Even when the company names are the same, the people change. The superintendent who nailed moisture management on your last job may be on another project or at another firm.
Jason is seeing more moisture trapped in assemblies as mass timber moves into mainstream residential work with less specialized builders. So treat moisture management as part of onboarding on every project. Cover how to keep panels dry, what to do when they get wet, and why the roof membrane isn't a work surface. It'll feel repetitive to the people who've heard it before. For someone on the crew, it's the first time.
Why Moisture Monitoring Is Worth It
Jason's case for moisture monitoring comes down to one line: "You might get lucky with the weather and you just might not."
Nobody builds with mass timber planning for the building to decay. So be honest about where the moisture risks are, identify them, and monitor them. It's relatively low cost compared to fixing the damage.
If you're exploring mass timber for your own projects, your going to need the team, knowledge and connections to make it successful.
Embodied Carbon in Mass Timber Buildings w/ Ryan Zizzo of Mantle Climate
Mass timber gives a project a head start on embodied carbon. What the team does with the rest of the building decides how far that head start goes. Foundations, cladding, material quantities, and how carefully the carbon gets counted all move the final number.
Ryan Zizzo has worked on that number for close to 20 years. He's the founder of Mantle Climate , a 15-person sustainability and climate consultancy based mostly in Toronto. Ryan is a structural engineer with a master's in sustainable building. He spent about 10 years running LEED certifications at Halsall Associates, now part of WSP. Then he spent three years consulting in Helsinki, where mass timber, whole life carbon, and circularity were already standard practice.
Ryan has supported some of Toronto's best-known mass timber projects, including T3 Bayside, Limberlost Place at George Brown College, and a YMCA transitional housing building. This article pulls out what those projects teach:
- how to make the business case
- how to read a carbon number
- the design moves that lower embodied carbon
- what policy to watch in your market
This article is just one part of the newsletter where we cover who and what's shaping the mass timber industry.
👉 Stay ahead of the mass timber industry & grow your network. Join Our Newsletter
Why Low-Carbon Buildings Pay Off for Owners
If the owner isn't on board, nothing gets done. Ryan's business case comes down to three things:
- Lower operating costs. A building that uses less energy costs less to run. If your energy bill is a third of what it would've been, that's savings every year.
- Future-proofing. Environmental, climate, and waste regulations are likely to tighten. Lower-carbon buildings are less exposed to the costs that come with that.
- Higher value. Reports from the U.S. and Canada Green Building Councils show certified spaces earn higher rents and returns. Many international investors require certification before buying a large commercial asset, so the buyer pool is bigger when it's time to sell.
On upfront cost, one Canada Green Building Council study Ryan cited found about an 8% premium to go fully net zero. That premium paid back within a 25-year amortization period.
Making that case starts with knowing exactly what you're measuring.
Embodied Carbon vs. Operational Carbon: What's the Difference?
Whole life carbon is a building's full carbon footprint. It splits into two parts.
Operational carbon is what shows up on your energy bill: heating, cooling, ventilation, lighting, and everything plugged in. It's calculated with an energy model.
Embodied carbon is everything that doesn't show up on your energy bill. Upfront embodied carbon, also called cradle to completion, covers:
- raw material extraction
- transportation to the manufacturer
- manufacturing
- delivery to site
- Construction
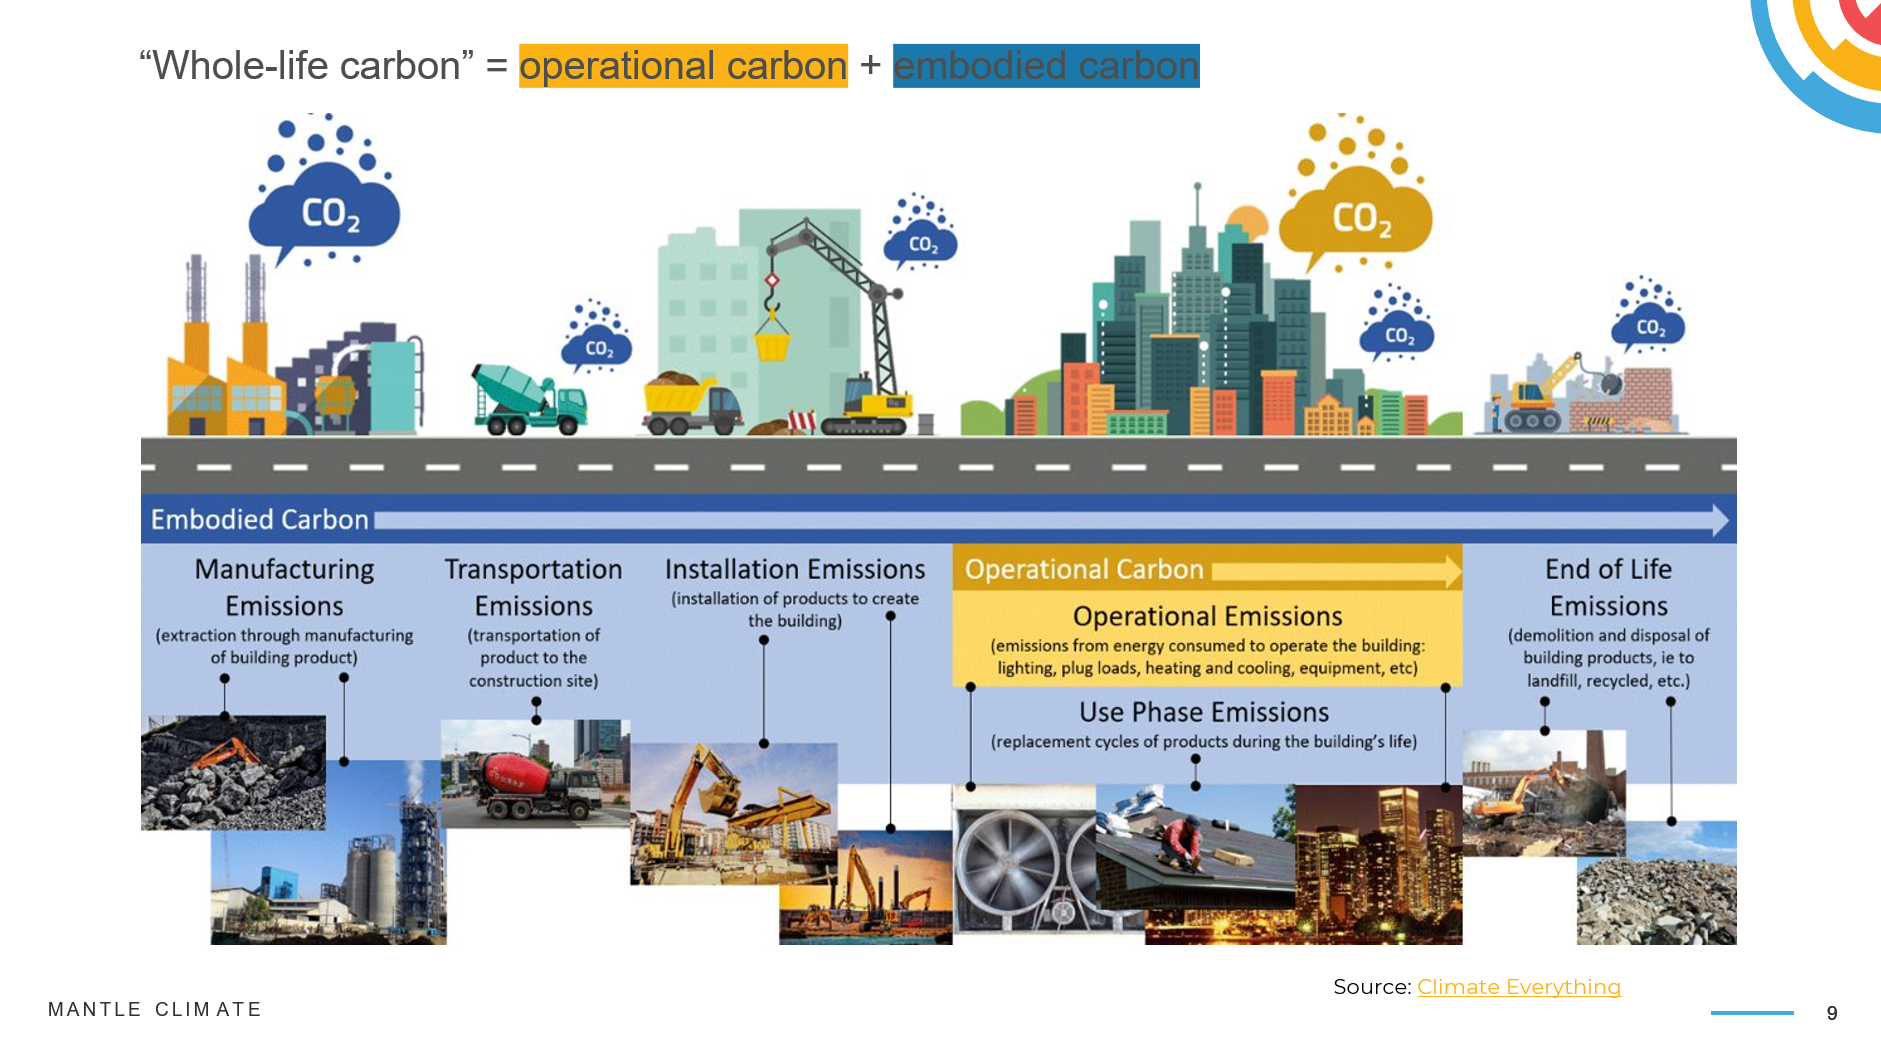
The full embodied picture also includes the use phase (replacing a roof, windows, or doors) and end of life (decommissioning and recycling).
Embodied carbon is calculated with a life cycle assessment (LCA). A whole building LCA (WBLCA) applies that method to an entire building. Ryan says the industry is making good progress on operational carbon as grids decarbonize and new buildings get more efficient. Embodied carbon is the other half of the pie, and it's where material choices like mass timber show up.
Once you know what an LCA measures, you can read the results with a sharper eye.
How to Read an Embodied Carbon Number
Embodied carbon is typically reported in kilograms of CO2 per square meter. Ryan's benchmarks:
- Around 400: a good result.
- 250 to 350: very low embodied carbon buildings.
Before you compare two numbers, check what's behind them:
- What's in scope? Most studies cover the structure and envelope.
- Were the connections counted? Some studies leave out steel connectors and treat them as a rounding error. Ryan says connections can carry a large carbon impact, depending on the metal, the size, and how they're made.
- How detailed was the study? A more thorough study often produces a higher number, because it captures materials other studies skipped.
Example: Limberlost Place
Limberlost Place at George Brown College shows what a complete study looks like. Ryan helped write a Natural Resources Canada grant application for the project about a decade ago. Its recently released assessment came in at 400 kg CO2/m². The study was detailed enough to include every steel connection in the mass timber structure. Publishing a number that complete gives the industry a real data point to learn from.
A good study also shows you where the carbon lives, which tells you where to cut it.
5 Ways to Lower Embodied Carbon on a Mass Timber Project
1. Measure and Report It, Even When You Don't Have To
T3 Bayside is a 10-story mass timber office building in Toronto. Mantle completed the embodied carbon assessment for its structure and envelope. The project didn't have to hit a threshold; it only had to calculate and report the number. That reporting earned a credit toward the building's LEED Gold certification. Measuring gives you a certification credit, a story to market, and a baseline for future decisions.
2. Decide on Below-Grade Space Early
Limberlost Place sits a few feet from Lake Ontario. Its program included underground space, and the high water table called for an extensive foundation and dewatering system. Those materials carry significant carbon. Ryan sees a growing movement toward building at grade and above as one of the most effective ways to cut embodied carbon. On sites with a high water table especially, weigh the carbon cost of below-grade space early.
3. Weigh Cladding Carbon Against Schedule Benefits
Limberlost's envelope arrived as large prefabricated panels on flatbeds and was craned into place. That's a real win for schedule and efficiency. The rigid frames that make those panels work rely on aluminum and other metals, which add embodied carbon. Neither choice is wrong. Make the trade-off on purpose.
4. Use Only the Material You Need
Ryan thinks the industry hasn't taken a hard look at which materials a building actually requires. Designers are often paid based on project budget, so there's little incentive to use material efficiently. Cutting what isn't needed saves carbon and money at the same time. Unlike most carbon strategies, this one lowers upfront cost.
5. Put Mass Timber's Speed to Work
The YMCA of Greater Toronto's first net zero certified building is a six-story, 31-unit transitional housing project downtown, with Assembly Corp as construction manager. It was funded through Canada's Rapid Housing Initiative, which comes with a very strict schedule. Mass timber was the only way to meet it, and the building went up in less than a year. When funding or financing depends on schedule, mass timber's speed can be what makes the project possible.
Design decisions are one driver. Policy is the other.
Embodied Carbon Policy: What to Check in Your Market
Ryan has done extensive policy work, and he sees momentum across Canada and the U.S.
In Toronto, he helped benchmark whole building LCA for large buildings for the first time in Ontario. That work fed into the Toronto Green Standard. It's a voluntary standard: projects that come in under its embodied carbon cap get a partial discount on development charges. The cap is 400 kg CO2/m² for most buildings, and lower for some building types.
Other markets are moving too:
- Vancouver has a robust embodied carbon policy.
- Edmonton is starting to require government buildings to report embodied carbon.
- Boston requires embodied carbon reporting for large new buildings.
- The Port Authority of New York and New Jersey has stringent low-carbon concrete requirements.
- California has low-carbon material requirements for state construction and whole building LCA requirements for large projects.
Codes are changing as well. Ontario now allows mass timber up to 18 stories, and BC and Quebec have done similar work. Ryan is also working on the 2030 National Building Code of Canada, which will include embodied carbon for the first time.
What to do in your market:
- Look for incentives tied to embodied carbon, like Toronto's development charge discount.
- Check whether your code allows taller mass timber. If it doesn't, there may be room to push for revisions.
- Watch for reporting requirements on public and large projects.
-
If you're exploring mass timber for your own projects, your going to need the team, knowledge and connections to make it successful.
How to Make Mass Timber Compete on Cost in Private Development w/ Josh Dortzbach of FOREFRONT Structural Engineers
Josh Dortzbach of FOREFRONT Structural Engineers on why timber gets cut at pricing, and the labor, system, and design decisions that keep it in the building.
You've seen it happen. A developer wants mass timber. The design team carries it through schematic design and into design development. Then the job gets priced, comes back over budget, and the timber gets cut.
Josh Dortzbach, SE, PE doesn't think that's a material problem. "Projects don't always die because timber is too expensive," he said. "They die often because nobody is telling the owner what it costs, or what to do about that cost."
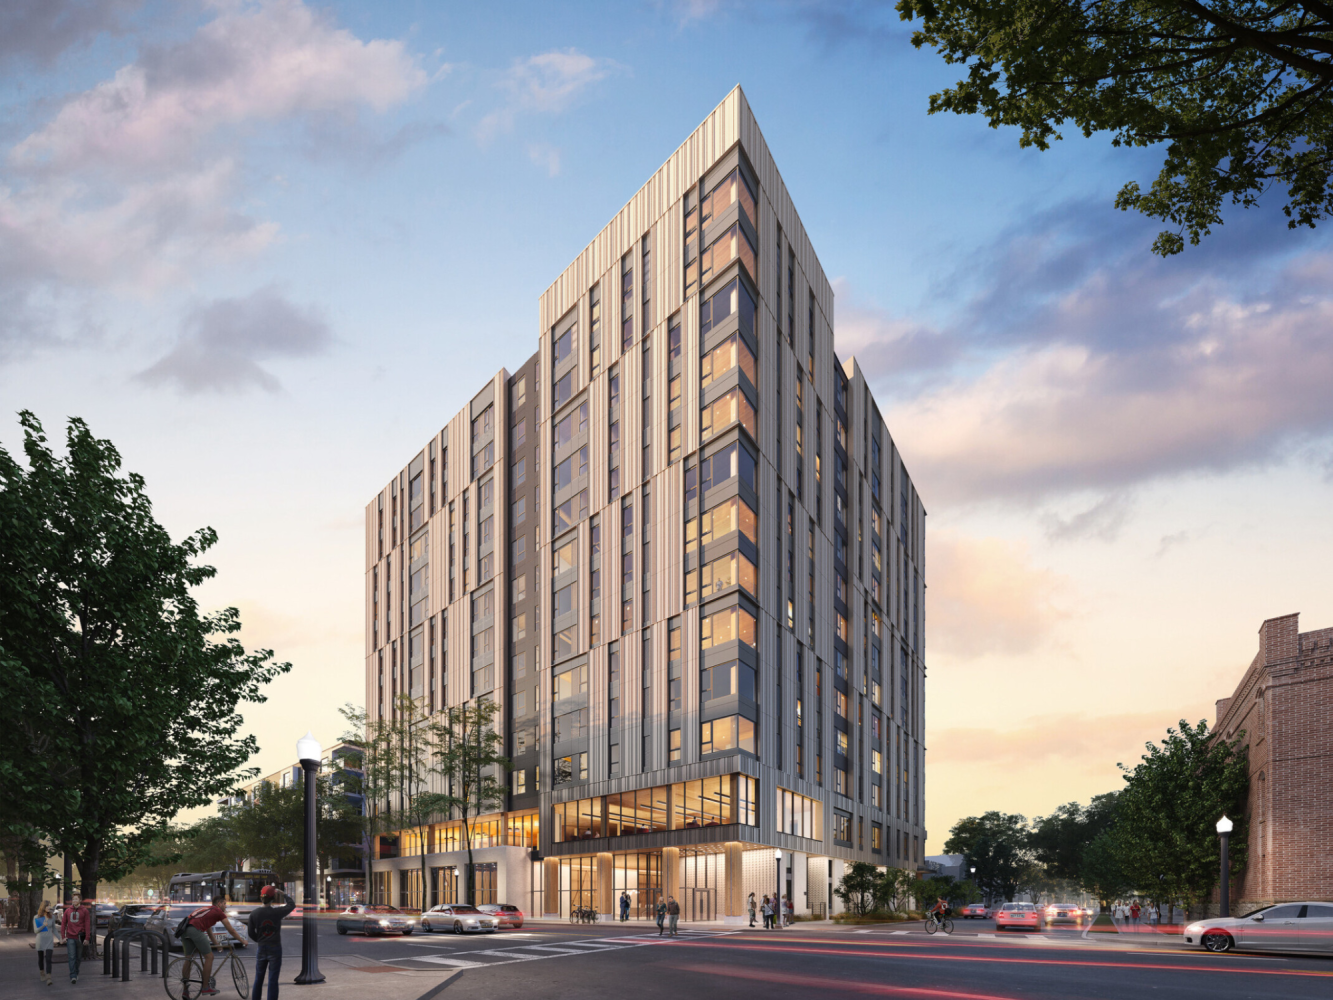
Dortzbach is a co-founder and CEO of Forefront Structural Engineers in Chicago. The firm's mass timber work includes INTRO Cleveland and 9th and High in Columbus (INTRO Columbus), a 13-story student housing tower made with mass timber from SmartLam . Much of FOREFRONT's work is in the private sector, for developers who need the numbers to work.
His approach comes down to three things. Know the numbers before schematic design is done. Solve for labor. Price the whole building, not just the frame.
This article is just one part of the newsletter where we cover who and what’s shaping the mass timber industry.
👉 Stay ahead of the mass timber industry & grow your network. Join Our Newsletter
Why Mass Timber Projects Go Over Budget
The usual sequence goes like this. The team finishes schematic design, moves into design development, and prices the job. It comes back over. Everyone puts ideas on the table. The design team gets paid to redesign, which it should, and the project gets priced again. By then something else has moved: the market, the budget, the schedule. "You're no better off than you were earlier," Dortzbach said.
Part of the problem is detail that shows up too late. Dortzbach sees projects reach DD without anyone accounting for a specific manufacturer's constraints. Panel width is a simple example. If one supplier ships four-foot-wide panels and another ships eight-foot panels, the narrow panel can mean twice as many crane picks and twice the labor to set the same floor. The wide-panel supplier might charge more for the material. Which one is cheaper depends on both numbers together.
TAKEAWEAY: Compare mass timber suppliers on material and erection labor together. A cheaper panel that takes twice as many picks may not be cheaper.
Is Mass Timber More Expensive Than Concrete?
The traditional answer has been that timber costs more as material and makes it back in labor.
Dortzbach says that's still true in places, but it varies by region, and the material side is changing. Domestic manufacturers have found their own ways to bring costs down. He points to SmartLam, the supplier on 9th and High, as much more cost-effective than it was two years ago, to the point it can compete with European suppliers.
The bigger issue is what you compare. A frame-to-frame comparison misses most of the money.
Take a cold-formed steel bearing wall building with concrete poured on a metal deck. The panelized walls go up quickly. Then the concrete crew comes in for the floor, and by Dortzbach's account about 75% of the floor-to-floor time goes to that horizontal work and the trade changeover. FOREFRONT has been developing a different combination: cold-formed bearing walls with CLT floor panels, all set by one carpentry crew, so the frame keeps moving without switching workforces.
Ceilings count too. Under the 2024 International Building Code, Type IV-B buildings up to 12 stories can leave up to 100% of the mass timber ceiling exposed, where the code has been adopted. In a steel or concrete building, a crew comes back to hang a gypsum ceiling. With exposed CLT, nobody has to.
So does the enclosure. At 9th and High, a post-and-beam building, crews are setting prepanelized cold-formed walls with the glass already installed, two floors behind the timber. That's faster than FOREFRONT's earlier projects and better for keeping weather out. The next question Dortzbach is asking: what if those exterior panels went up at the same time as the structure?
"You have to level all of the material costs, not just the frame of the building itself," he said.
TAKEAWEAY: Price systems, not frames. Include the trade sequence, the finishes, and the enclosure when you compare timber to concrete or steel.
Solving for Labor: How Fast Mass Timber Goes Up
Fewer people are going into the trades. To Dortzbach, that makes the cost question a labor question. "We are solving for labor at the end of the day," he said.
Chicago is a hard market to beat on speed. FOREFRONT designs post-tensioned concrete towers there too, and those crews build 12,000 square feet in two and a half to three days. In Raleigh, North Carolina, that cycle runs about 14 days. In Chicago, speed alone doesn't win the argument for timber.
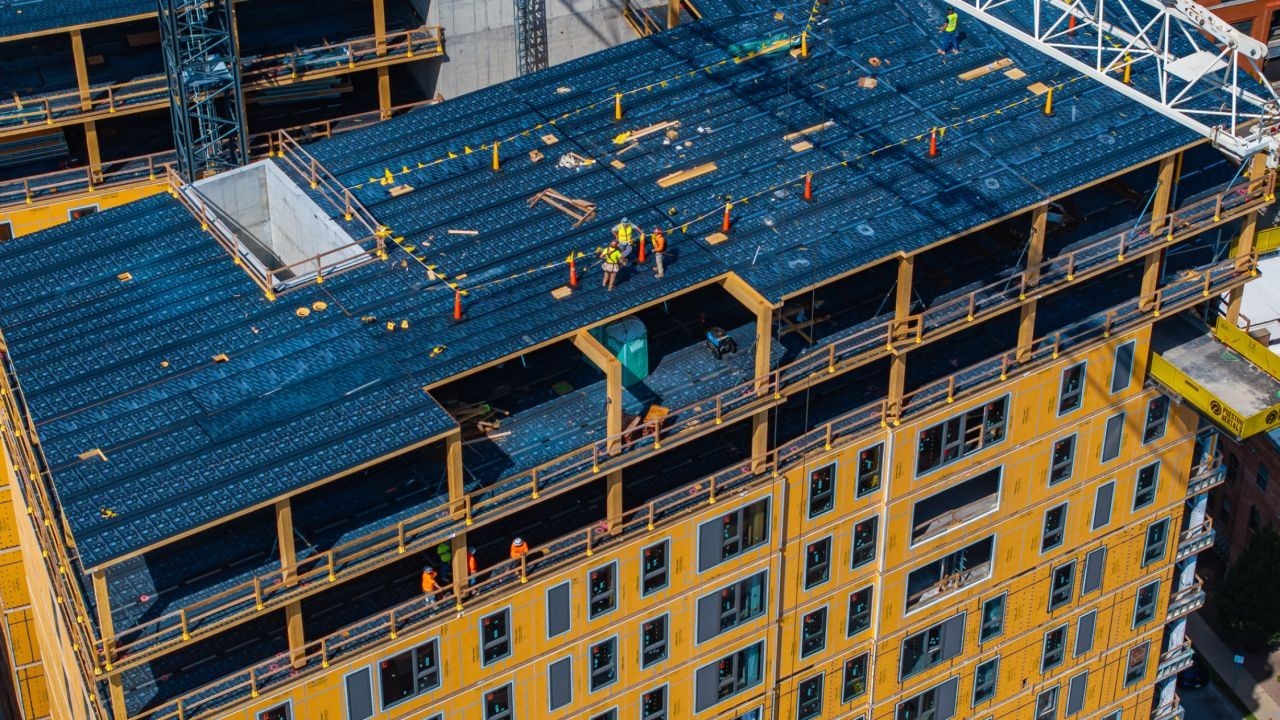
On 9th and High, the timber crew matched it: 12,000 square feet of mass timber in three-day cycles, with five or six people. Ironworkers set that building. INTRO Cleveland was set by carpenters, and the East Lansing project will be too. Different trades can do the work, and each has its own view of what works.
Speed becomes money through finance carrying costs, tower crane time, and the contractor's general conditions. FOREFRONT has built animations from productivity data on its own projects that stack a mass timber building beside a cast-in-place version, using regional rates. Where the project sits changes the pitch. In a slower concrete market, a developer can lead with timber as both a differentiator and a faster way to get in and up.
Tall timber still isn't all timber. These buildings use cast-in-place cores, so the concrete and timber crews have to work together.
What the Crews Changed on 9th and High
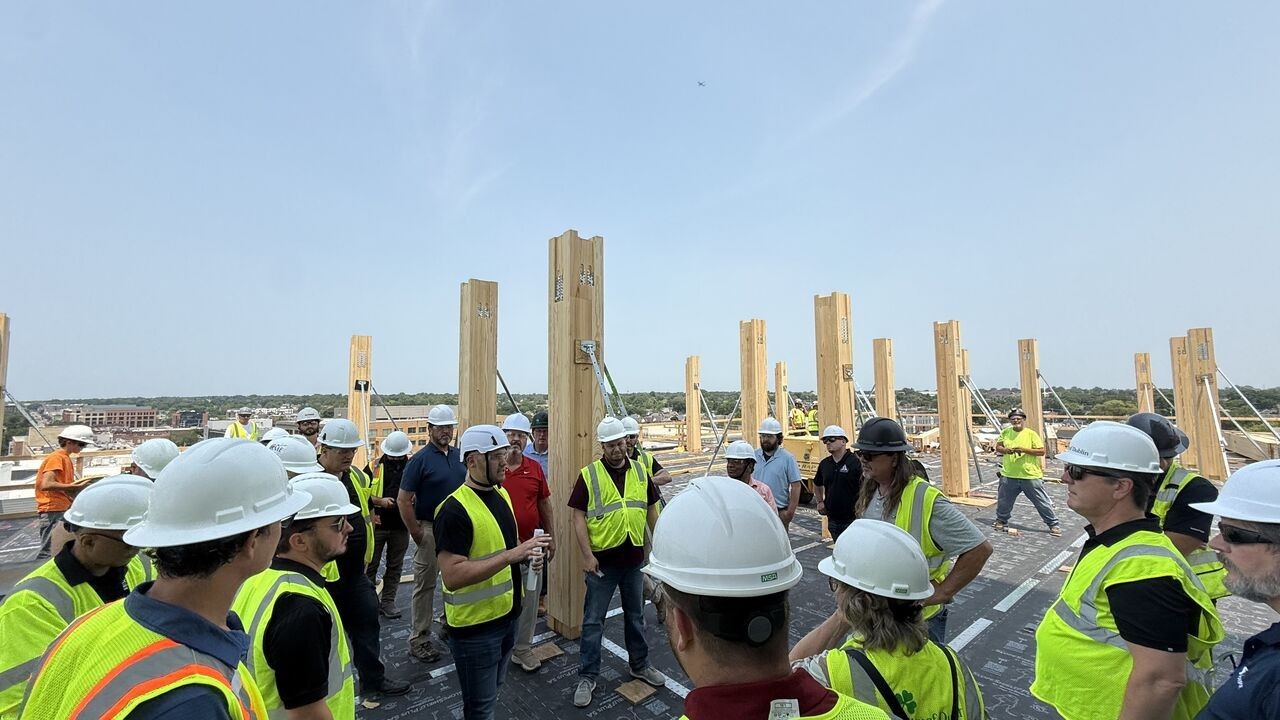
Several of the details that made 9th and High fast came from asking the people setting timber. "We should always be students," Dortzbach said.
Column joints. Many projects join columns with steel connections, either prefabricated or custom. Dortzbach watched laborers fuss with them in the field. On 9th and High, FOREFRONT switched to a wood-to-wood connection: a block-cut notch set with simple dowels. "There's a balance between a Swiss watch mentality and a get-er-done mentality," he said.
Panel joints. CLT panels are often joined with a recessed spline routed into each panel edge on a CNC machine. 9th and High uses Simpson Strong-Tie's LDSS straps instead. They sit on top of the panels, need no routing, and go down right over the waterproofed deck. That saves time at the plant and in the field. Dortzbach credits general contractor Elford Construction 's push to get the building watertight early, and SmartLam shipped the panels with a vapor barrier already on the deck.
Slab edge. A window wall needs room between the face of the column and the edge of the slab, typically a foot to two feet. Cantilevering CLT that far in its weak direction is hard, and the common fix is a haunch at each perimeter column, which adds another piece and another connection. FOREFRONT notched the column locally so the slab could sit on it, then developed a composite connector at the slab edge to push the spans further.
Crane time. On INTRO Cleveland, the team watched the tower crane do everything and saw how much time that cost. They set bundles of beams and columns on the deck and had one crew place them with a simple gantry crane, the kind most ironworkers have on site. That kept the tower crane on CLT panels.
TAKEAWAY: Before details are fixed, ask the crew that will set them what slows them down.
Off-the-Shelf Connectors and the Case for Commoditizing Mass Timber
INTRO Cleveland used custom-designed connectors throughout. That gave a local steel fabricator work it might not otherwise have had. It also caused problems during construction whenever a piece didn't fit up.
Since then, several manufacturers have brought out off-the-shelf concealed connectors that can be used in fire-rated assemblies of two or even three hours. FOREFRONT worked with Neutral on a three-hour loaded fire test of a mass timber assembly with standard connectors in 2025 with @Simpson Strong-Tie, a hardware supplier. The assembly performed well under full load. On 9th and High, the beam-to-column joints use standard Simpson connectors.
Connectors are part of a bigger argument. Walk through a large CLT or glulam plant and you'll see blanks come off the line quickly. The slowdown comes at CNC, where each piece gets cut for its connections. "For manufacturers to spit out just a pure blank with no finishing on it, that's like a dream for them," he said.
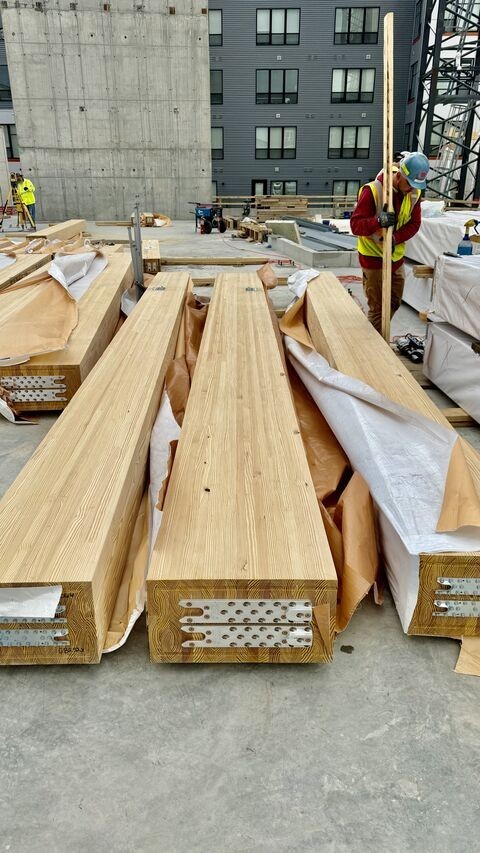
Dortzbach wants mass timber to work more like lumber already does. Builders buy 2x4s and sheet goods in standard sizes, and go to a lumberyard for higher grades. He'd like to see CLT blanks that could be bought and modified on site, and a menu of standard pieces that covers 70 to 80% of the market.
The pushback is that equipment lines, species, and design values vary too much across North America. Dortzbach doesn't buy it. "Whenever anybody says it's impossible, there's probably an ulterior motive behind that," he said. He doesn't expect it to happen overnight. But the industry already turned trees into commodity lumber. Turning commodity lumber into commodity panels and beams is the next step.
Standard parts don't mean standard buildings though. Dortzbach compares it to Lego or an IKEA kit: fixed pieces, unlimited combinations. Some volumetric modular buildings get criticized for looking like stacked boxes. A kit of commodity timber parts doesn't have to.
How to Get Cost Certainty Before Schematic Design
FOREFRONT builds its own software. The tools combine Rhino and Grasshopper with C#, Python, and custom code that reaches into the APIs of industry-standard programs. They let the team test options for any manufacturer and any layout quickly, and check them against the developer's pro forma.
Some developers now bring FOREFRONT in before they've hired an architect. The team tests structure and program against the pro forma first, then brings the architect in to do what architects do best. Recently, one FOREFRONT engineer designed an optimized 18-story building in a day, and it went out for pricing. Dortzbach calls that an extreme case. The client doesn't pay for a day of labor. It pays a premium, because the work cut out close to six months.
Programming is part of the early work. Clients and architects often ask for the most efficient grid. The answer depends on where the amenities go and what unit sizes work. Dortzbach aims for about 80% efficiency and leaves 20% for what makes the building distinct.
The software is only part of it. Dortzbach pairs a 40-year veteran with a two-year engineer who's fluent in digital tools, then puts both in front of a contractor who gets asked how to do it better. He tells his engineers to stay in coordination meetings after their part is done, because that's where they learn how the rest of the process works.
"We should never get to schematic design completion and not know that we can build this thing." - Josh Dortzbach
TAKEAWAY: Test the structure against the pro forma before schematic design is complete, with the supplier's constraints included. Pricing should confirm the budget, not reset it.
What's Next: Cold-Formed Bearing Walls and CLT
The system Dortzbach is most excited about combines panelized cold-formed steel bearing walls with CLT floors. The target is student housing, multifamily, and hotels at roughly 15 stories and under. He doesn't think timber can beat five-over-one wood framing on cost. He thinks it can take much of what has been built above that height in cold-formed steel or cast-in-place concrete.
FOREFRONT is using it on a 10-over-3 project in East Lansing, Michigan: cold-formed bearing walls, CLT slabs, and punched windows and window wall following quickly behind the frame. The hard part is shortening. Stack CLT on cold-formed walls platform-style at that height, and the top of the building could move down as much as an inch and a half to two inches. At five stories that's manageable. At eight to 12, it isn't. FOREFRONT has developed connector nodes between the floors to solve it.
He puts the opportunity at about 10 billion square feet of load-bearing wall construction over the next decade.
None of what he describes is fixed. "Whatever tools or tips or tricks we're doing right now, it's going to be different in six months," he said.
If you're exploring mass timber for your own projects, your going to need the team, knowledge and connections to make it successful.
Frequently Asked Questions
- Is mass timber more expensive than concrete? Often on material and construction cost, according to published cost studies, but results vary widely by project and region. Comparisons that account for schedule, crane time, finance carrying costs, and finishes such as exposed ceilings can narrow or close the gap. FOREFRONT Structural Engineers compares whole building systems rather than structural frames alone.
- How fast can a mass timber floor be installed? On 9th and High in Columbus, Ohio, a crew of five or six set 12,000 square feet of mass timber in three-day cycles, according to FOREFRONT. That matches post-tensioned concrete cycles in Chicago, one of the fastest concrete markets in the country.
- Can mass timber ceilings be left exposed in tall buildings? Under the 2024 International Building Code, Type IV-B construction, allowed up to 12 stories, permits up to 100% of mass timber ceilings to be exposed within a dwelling unit or fire area. The 2021 code allowed 20%. Adoption varies by state and city.
- What are off-the-shelf mass timber connectors? They are manufactured, tested connectors, such as concealed beam hangers, used in place of custom-fabricated steel. Several carry two-hour fire ratings, and a three-hour loaded fire test of a mass timber assembly using standard connectors was completed in 2025.
- When should a project team price mass timber? Before schematic design is complete. FOREFRONT tests structural options against the developer's pro forma early, sometimes before an architect is hired, so the first full pricing confirms the budget instead of triggering a redesign.
- Who installs mass timber, carpenters or ironworkers? Both. On FOREFRONT's projects, ironworkers set 9th and High in Columbus, while carpenters set INTRO Cleveland and will set the firm's upcoming project in East Lansing, Michigan.
Building a CLT Plant: Why Starting Small Can Beat Starting Big with Ledinek's Jaka Bradac
How mass timber gets made, what plant size changes, and what Ledinek's Jaka Bradač has learned selling CLT and glulam lines on both sides of the Atlantic.
Picture two CLT plants in the same town, chasing the same customers. One cost $25 million. The other cost $250 million. At the start, they'd win the same share of the market. One of them has to sell more than three times as much to stay on track.
That's the case Jaka Bradac makes for starting small. He's Sales Executive for North America at Ledinek Engineering, a Slovenian company that has designed and built more than 35 CLT and glulam lines. Most North American plants were built big, sized for demand expected three to five years out. Bradač argues the next wave should look different, and his reasons come down to four things: how much you have to sell, how fast you get to product, how you grow, and how much control you have over your wood.
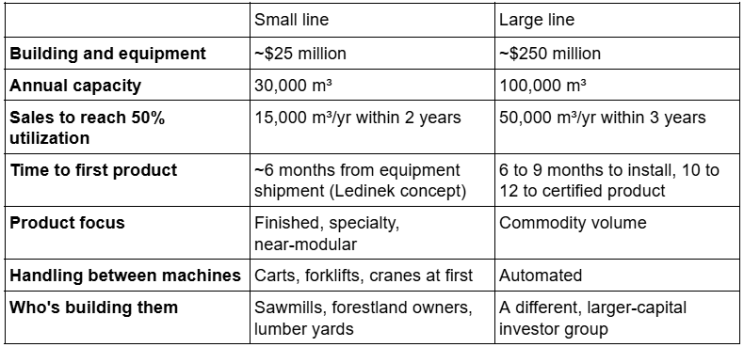
Here's how the two compare.
This article is just one part of the newsletter where we cover who and what’s shaping the mass timber industry.
👉 Stay ahead of the mass timber industry & grow your network. Join Our Newsletter
How is CLT made? From log to finished panel
Every CLT plant, large or small, turns boards into panels the same way. Cross-laminated timber (CLT) is a structural panel made by gluing layers of lumber at right angles to each other. Glulam is a beam or column with every lamination running the same direction. Both follow the same path.
Example of a CLT production line. Credit: Ledinek
Where the lumber comes from
A sawmill cuts the log to a pattern set by a scanner and optimizer, sorts the wet boards, and kiln-dries them, typically to about 12% moisture content. (ANSI/APA PRG 320-2025, the North American CLT standard, caps it at 16%.) The boards are planed and graded visually, by X-ray, or by machine stress rating (MSR), which bends each board to measure stiffness.
Inside the plant
A graded board still carries knots, cracks, and splits. The plant regrades it and cuts out the defects. The clear pieces are finger jointed into long laminations. That joint is watched closely: glue application, joint pressure, and friction through the press are all monitored, and joints get daily tension tests. Then the laminations are planed, the surfaces prepared, and glue applied, with ambient conditions recorded. The press applies a specified load for a specified time. A finishing step completes the panel.
Bradač calls the finger jointer, the planer, and the press machine centers. They're the expensive part of a line, and they set its capacity. Everything that moves wood between them is handling: automated conveyors in a big plant, carts and forklifts in a small one. Handling is where a small line can save the most up front, and where it finds capacity later.
TAKEAWAY: Large or small, every CLT plant runs the same steps: regrade, cut out defects, finger joint, plane, glue, press, finish. Scale changes how those steps are automated and connected. It doesn't change what they are.
How do European and North American CLT plants differ in size and wood supply?
In Europe, CLT grew out of glulam. The first producers were attached to sawmills, and some were tied all the way back to logging. The boards that reached their lines came from their own mills, not the open market. Those plants started small and grew over time. That control shows up in the product: a typical European CLT layup mixes a wide range of layer thicknesses and grades, because the producer decides which boards go where.
North American plants mostly skipped that path. They were built at large scale “from zero,” and all but a few buy their lumber on the open market, usually as graded, kiln-dried dimensional lumber.
How does plant size change a CLT plant's risk?
Capital comes with a production target. The bigger the investment, the more the plant has to produce and sell to cover it, and the sooner it has to get there.
But plant size doesn't change demand. Go back to the two plants in the same town. At the start, they win the same customers and the same orders. What changes is how much of each line those orders fill.
The small plant needs to sell half its 30,000 cubic meters, or 15,000 a year, within its first two years. The large plant needs to sell half of 100,000, or 50,000 a year, within three. If both win the same orders, the small plant is on track. The large plant is running at a fraction of its capacity. The small one, as Bradač puts it, doesn't have to stress as much.
That pressure decides what each plant can make. A large plant only makes money with its press full, so it has to chase commodity volume. Specialty projects don't fill an operation that size. A small plant can take that work, and specialty is where the margin is.
The volume target also takes a long time to reach. In Europe, the companies running 100,000 cubic meters a year got there after 20 years of winning business.
TAKEAWAY: A large plant carries more risk because it has to sell more, sooner, into the same market. A small plant can hit its target on fewer orders, and that leaves room for higher-margin specialty work.
What should a small CLT line make?
A small line wins on product, not volume.
One of the smallest lines Ledinek has built, in Europe, has a press that makes panels up to 45 feet long and runs four to five cycles a day. The plant doesn't sell bare panels. It goes a couple steps further to serve the housing market: insulation and cladding installed at the plant, ready to go. It's a niche, value-added product. It doesn't need to compete with the large manufacturers for big projects.
Bradač sees the same model fitting North America: a more complete, modular or prefab product that simplifies the purchase and grows the market.
But that model doesn't lock a small line out of larger work either. A $25 million plant can still run eight CLT press loads a day. It needs longer delivery times on a big job, but it can deliver. And size alone doesn't guarantee throughput. Unless a plant's downstream formatting line is fully automated across several machine centers, it runs into bottlenecks anyway.
How fast can a CLT plant get product out the door?
A 100,000 cubic meter line takes six to nine months to install and 10 to 12 months to reach first certified product, roughly. Every situation is unique.
Ledinek's 30,000 cubic meter concept is built to move faster. Product comes about three months after installation starts. Then comes roughly a month of commissioning to dial in reliable bonds, and three to four weeks for APA certification. That's about six months from the day equipment ships from Europe to product on the U.S. market.
How does a small CLT line add capacity?
Start with the machine centers. Move wood between them by cart, forklift, or overhead crane. Automate the links later, when the orders justify it.
Full automation between machine centers is what drives a line's price up. Plenty of North American plants still run on hand work, and a new pilot plant can do the same.
Growth then comes in two steps. The first is utilization. Machine centers are built with growth in mind, so they are rarely the limit. Handling is. Wood doesn't reach the machine because the forklift driver is on a coffee break and half an hour is gone. Or it can't leave because something backed up downstream. Tightening that up adds roughly 20 to 25% capacity from equipment you already own. The second step, if you need to double output, is ordering another line.
“It's not the machine centers. It's mostly the handling around the machine centers.” - Jaka Bradač, Ledinek
No two lines come out the same. Each is customized to the owner, which is why machine selection matters at the start. It sets how much headroom you have to grow into.
What this means if you're considering a CLT plant
- Size the line to the orders you can win, not the market you expect.
- Spend first on machine centers. Move wood manually until volume pays for automation.
- Make a product your line can add to: finished, specialty, higher margin.
- Get close to the wood. Own a mill, partner with one, or build next to one.
- Choose machines with growth potential in mind. Your first 20 to 25% of growth comes from handling, not new equipment
If you're exploring mass timber for your own projects, your going to need the team, knowledge and connections to make it successful.
Frequently asked questions about CLT plants
- How is CLT made? Kiln-dried, graded lumber is regraded at the plant and trimmed of defects such as large knots and cracks. The clear pieces are finger jointed into long laminations, planed, and glued. Layers are laid at right angles to each other and pressed under a specified load and time, then finished.
- How much does a CLT plant cost? It depends on capacity and automation. Ledinek’s Jaka Bradač contrasts roughly $25 million for a small plant with $250 million for a large one as an illustration. Published European projects include about €30 million for a 100,000 m³ plant (2017) and €130 million for 140,000 m³ including sorting and planing.
- How long does it take to build a CLT plant? According to Bradač, a 100,000 m³ line takes six to nine months to install and 10 to 12 months to reach first certified product. Ledinek’s 30,000 m³ concept is designed to produce certified product for the U.S. market about six months after equipment ships from Europe.
- What is the difference between CLT and glulam? CLT is a panel made from layers of lumber glued at right angles, used for floors, roofs, and walls. Glulam is a beam or column made from laminations glued with the grain running the same direction. Both are mass timber products and share much of the same production process.
- Can CLT be made from hardwood? Yes. Yellow poplar was added to ANSI/APA PRG 320, the North American CLT standard, in its 2025 edition. University testing found yellow poplar CLT comparable in strength and stiffness to Southern pine CLT. Hardwood lumber is still appearance graded rather than machine stress rated, which remains a gap for glulam.
- What wood species are used for CLT in North America? PRG 320-2025 covers softwood groups including Spruce-Pine-Fir, Douglas Fir-Larch, Hem-Fir, Southern pine, and others, plus yellow poplar.

AEC Convention
This is THE mass timber event where new projects get started, deals happen, and you grow your network (ask anybody who comes).
Next year, we'll have dedicated tracks for each AEC profession, and a series on developer conversations and priorities.